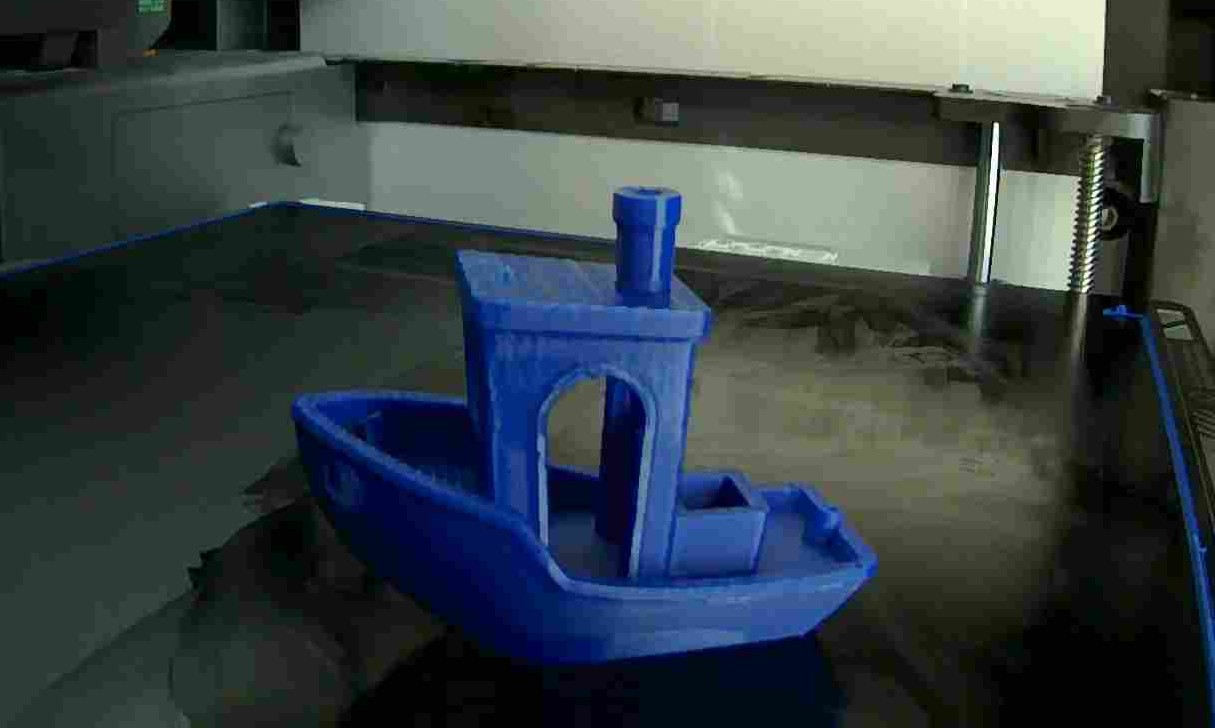
By using some of the signatures made previously on this thread, I believe I have successfully printed with the blue. The changes that I did not alter the performance of the white either.
Thank you to all of those who figured this all out before so that I had less trouble.
I also had massive problems with the BL PETG Blue. Changing to 265C and increasing fan speed seemed to have helped a lot. BL should really to a better QC, or at least add info about the blue needing different settings
I just wanted to share my experience with Bambu Lab PETG filament and the P1P.
Just like the OP, I had the same horrible stringing (or is it layers separating?) when printing a threaded mason jar lid.
As it was suggested in this thread, I changed the default BL PETG settings to the following and got pratically perfect results:
printing temp to 265c
max volumetric speed to 10mm3
cooling min 40%
cooling max 90%
aux fan speed to 30%
I didn’t have any problems printing a 3D Benchy using the stock BL profile but for some reason I guess the stock profile is just not good enough for more complex shapes.
I had the same problem with PETG-CF, no layer adhesion and thread formation. For me the problem was from under-extrusion. Since I left my additional lighting off during the flow calibration, it’s been fine.
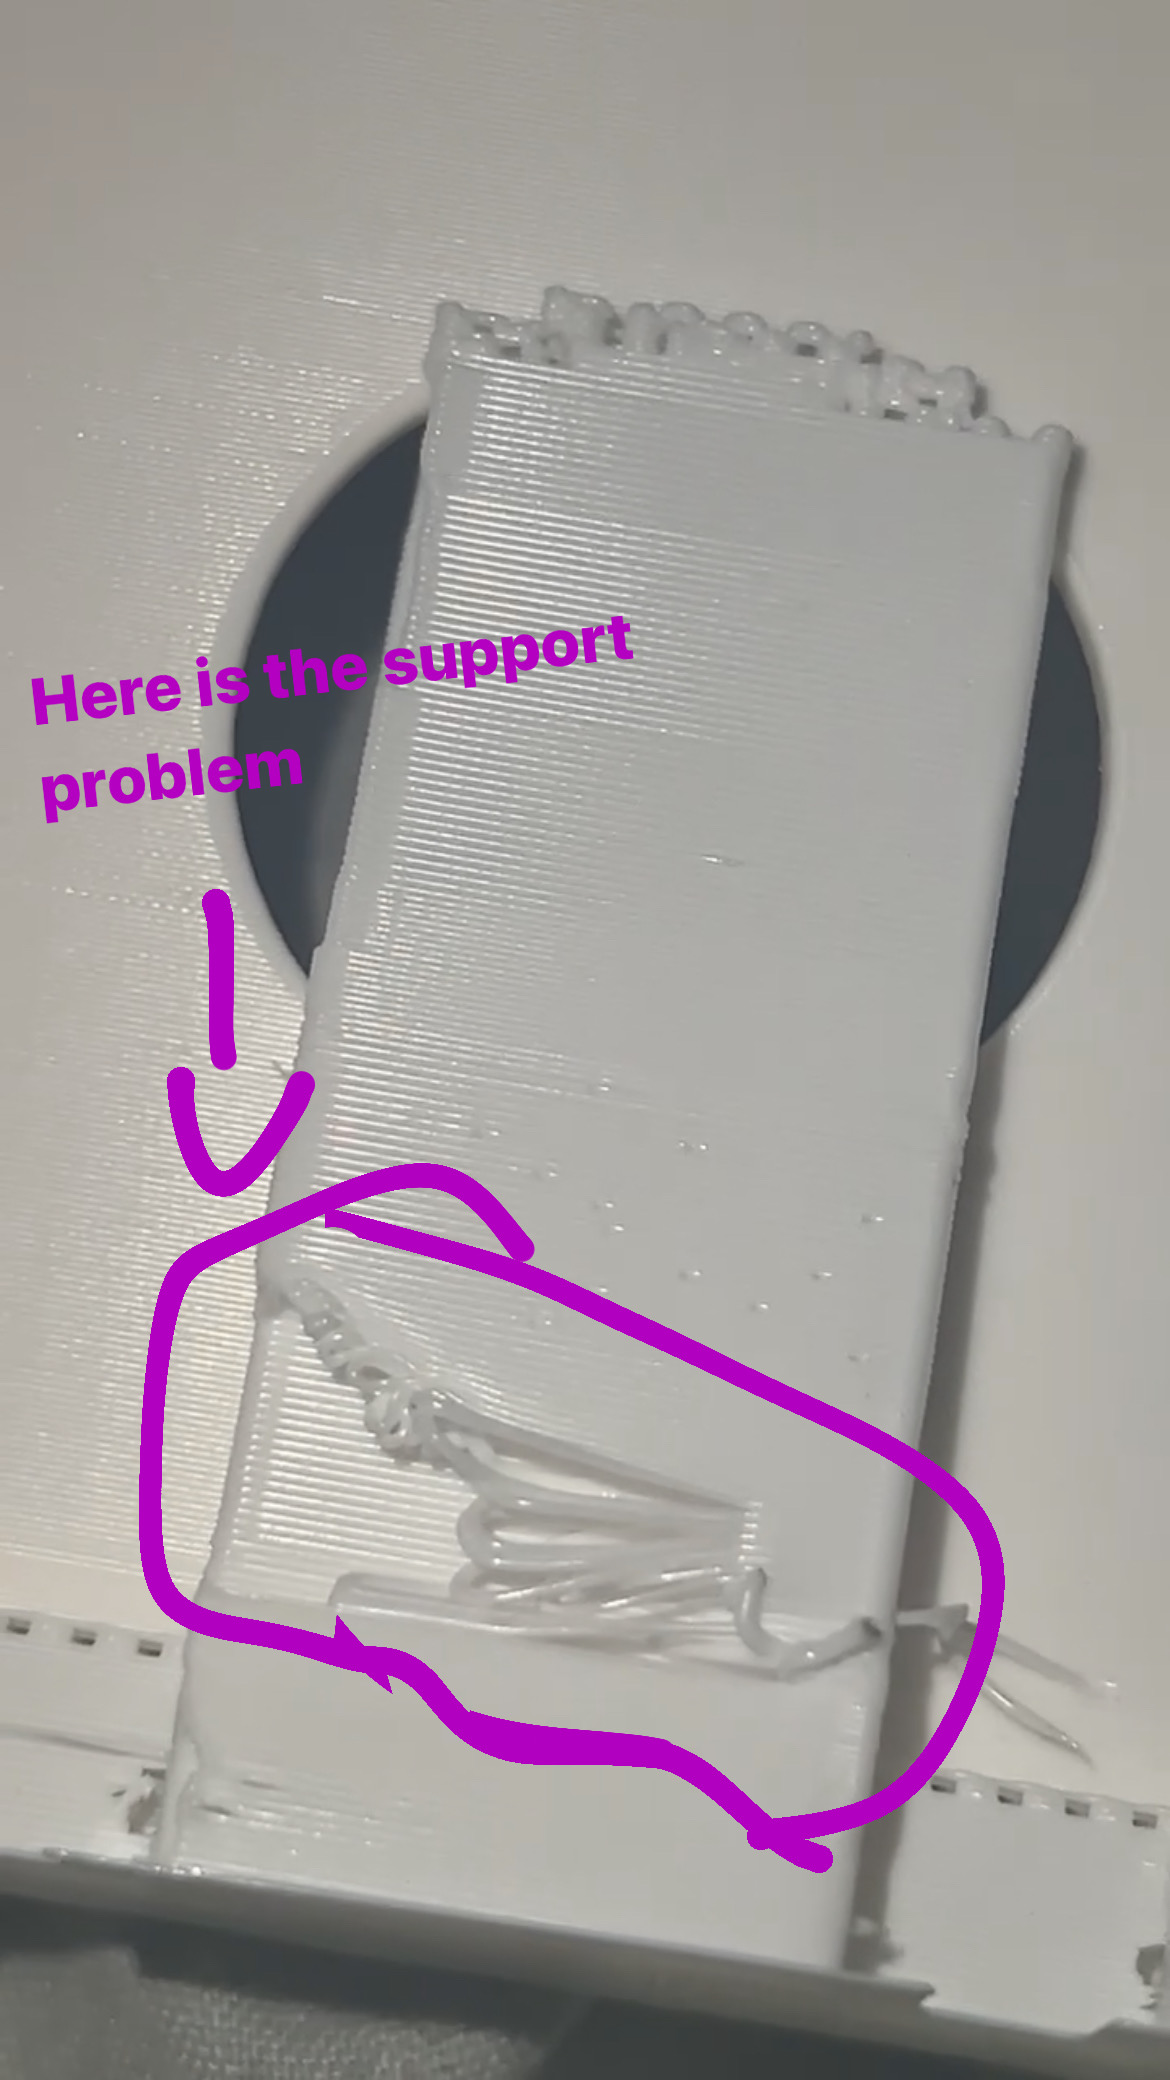
I use all the setting you just said and here is the result I don’t understand why there is a plenty of little hole and a part of the support is not looking really well
@Gab44k If you tilt that model a few degrees to the left so the vertical part is straight up or even slightly tilted the opposite way, it would likely only need supports for the base. But you should slow it down as the piece might wiggle when the nozzle is near the top. Or tip it on its side and use tree supports for just the overhangs. Also, sometimes for aesthetics it’s better to split up models so you don’t need any supports and join them together after printing.
Dear friends,
so many people tell me that PETG printing is a zero brainer but I don’t feel that way. As many other users here I started with the same problems with Bambu PETG basic:
many filament gooping up at the nozzle
many debris on the build plate
ugly infills
matte surface
After reading and testing this is my current state:
filament IS dry
print temp at 255°C
max volumetric speed = 6
inner wall = 200
gyroid infill
layer height >= 0.2 improved a lot. Otherwise nozzle keeps running on the lines
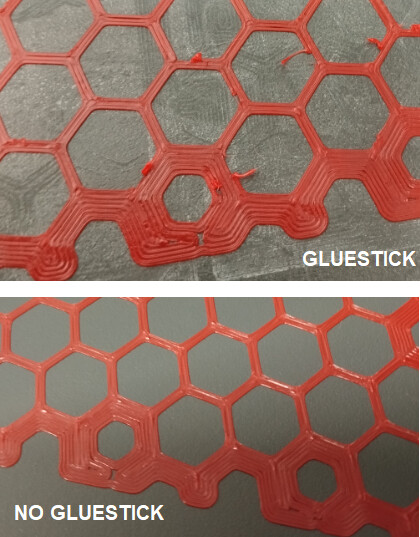
It is not that important to me to print fast but to print reliable. Those settings worked for me okay for some time until I found printing honeycombs at the first layer giving me frustration. It appears that some lines just won’t stick to the bed. Raisig print and bed temperatures and playing with the flow ratio did not change anything so I was removing the glue stick and that did the trick. See the following picture (ignore the brim around the honeycombs):
Often glue stick is used as a release layer, not an adhesion layer so removing it and having the print stick better does make sense. There are lots of people here, myself included that don’t use glue stick… 3d printing is finding what works for you.