First/Top Layer Gaps on H2 Series — Confirmed Bug, Still Unresolved

I want to bring attention to an ongoing print quality issue affecting the H2 series that has gone unresolved for many months and is continuing to grow in reports.

Many H2C, H2D, and H2S owners are experiencing gaps between lines on first and top layers, pinholes, and lines not fusing together — particularly on complex geometry and detailed prints. This has been reported consistently since late 2024 and reports are still being added weekly.

A Bambu developer confirmed this is a known bug in February 2026 on the official GitHub issue tracker and stated a fix was being worked on. Since that response there has been complete silence from Bambu’s side despite continued and growing community reports.

In the meantime, many of us have been sent through extensive hardware troubleshooting by support including bed leveling, flow calibration, hotend swaps, eddy sensor checks, and factory resets. None of these resolve the issue because the evidence strongly points at the slicer, not the hardware. Notably, internal test prints stored on the printer produce near-perfect results on the same machines that show consistent defects when printing Bambu Studio sliced files.

I have personally completed the following without resolution:

  • Bed trammed manually to within 0.005mm, factory reset, full recalibration

  • Multiple hotend swaps — issue identical across all units

  • Eddy sensor gap corrected per wiki spec

  • Flow calibration confirmed no adjustment needed

  • All available Bambu Studio and firmware updates applied

  • All suggested workarounds from the GitHub thread tested

My machine produces near-perfect results on internal test prints and simple geometry. The defects appear consistently on complex geometry sliced in Bambu Studio.

The official bug report is here and needs more documented reports to get prioritized:
https://github.com/bambulab/BambuStudio/issues/9768

I am posting here because after weeks of support tickets, extensive personal troubleshooting, and no developer response on GitHub for months, I am hoping someone from Bambu’s team monitoring this forum can either provide a status update on the fix or escalate this internally. This is affecting a significant number of owners of what is marketed as the flagship Bambu product line.

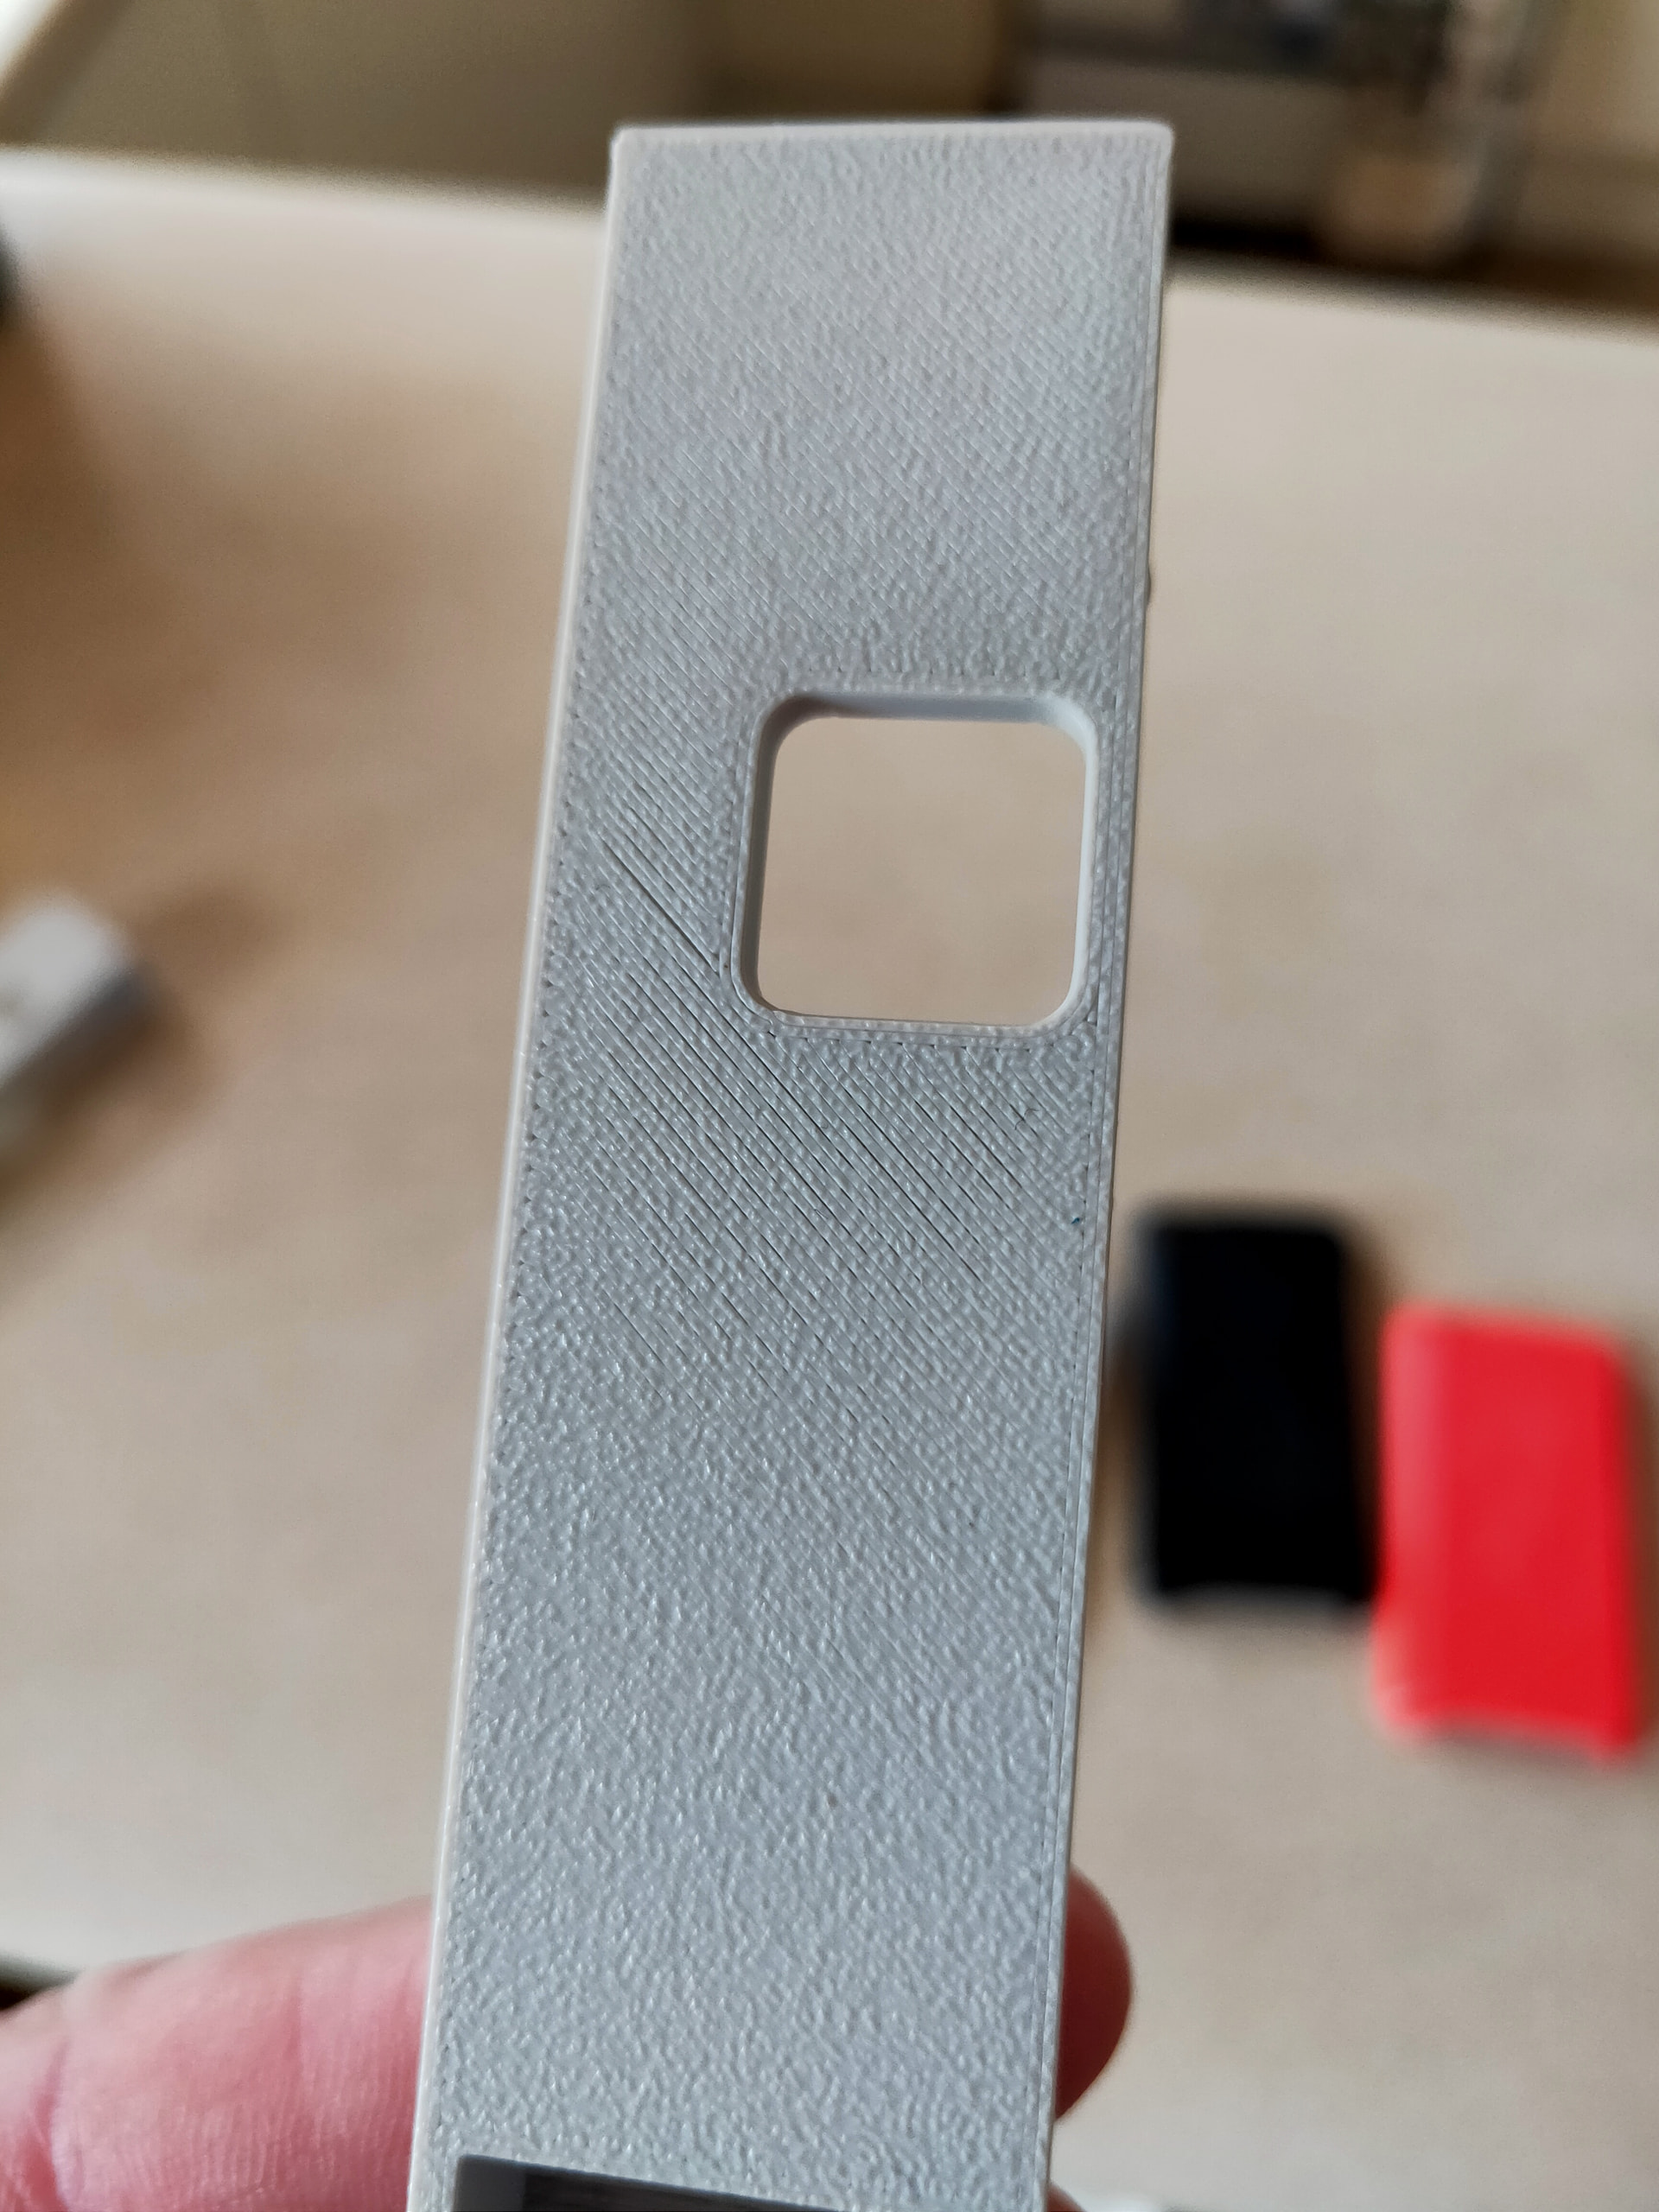
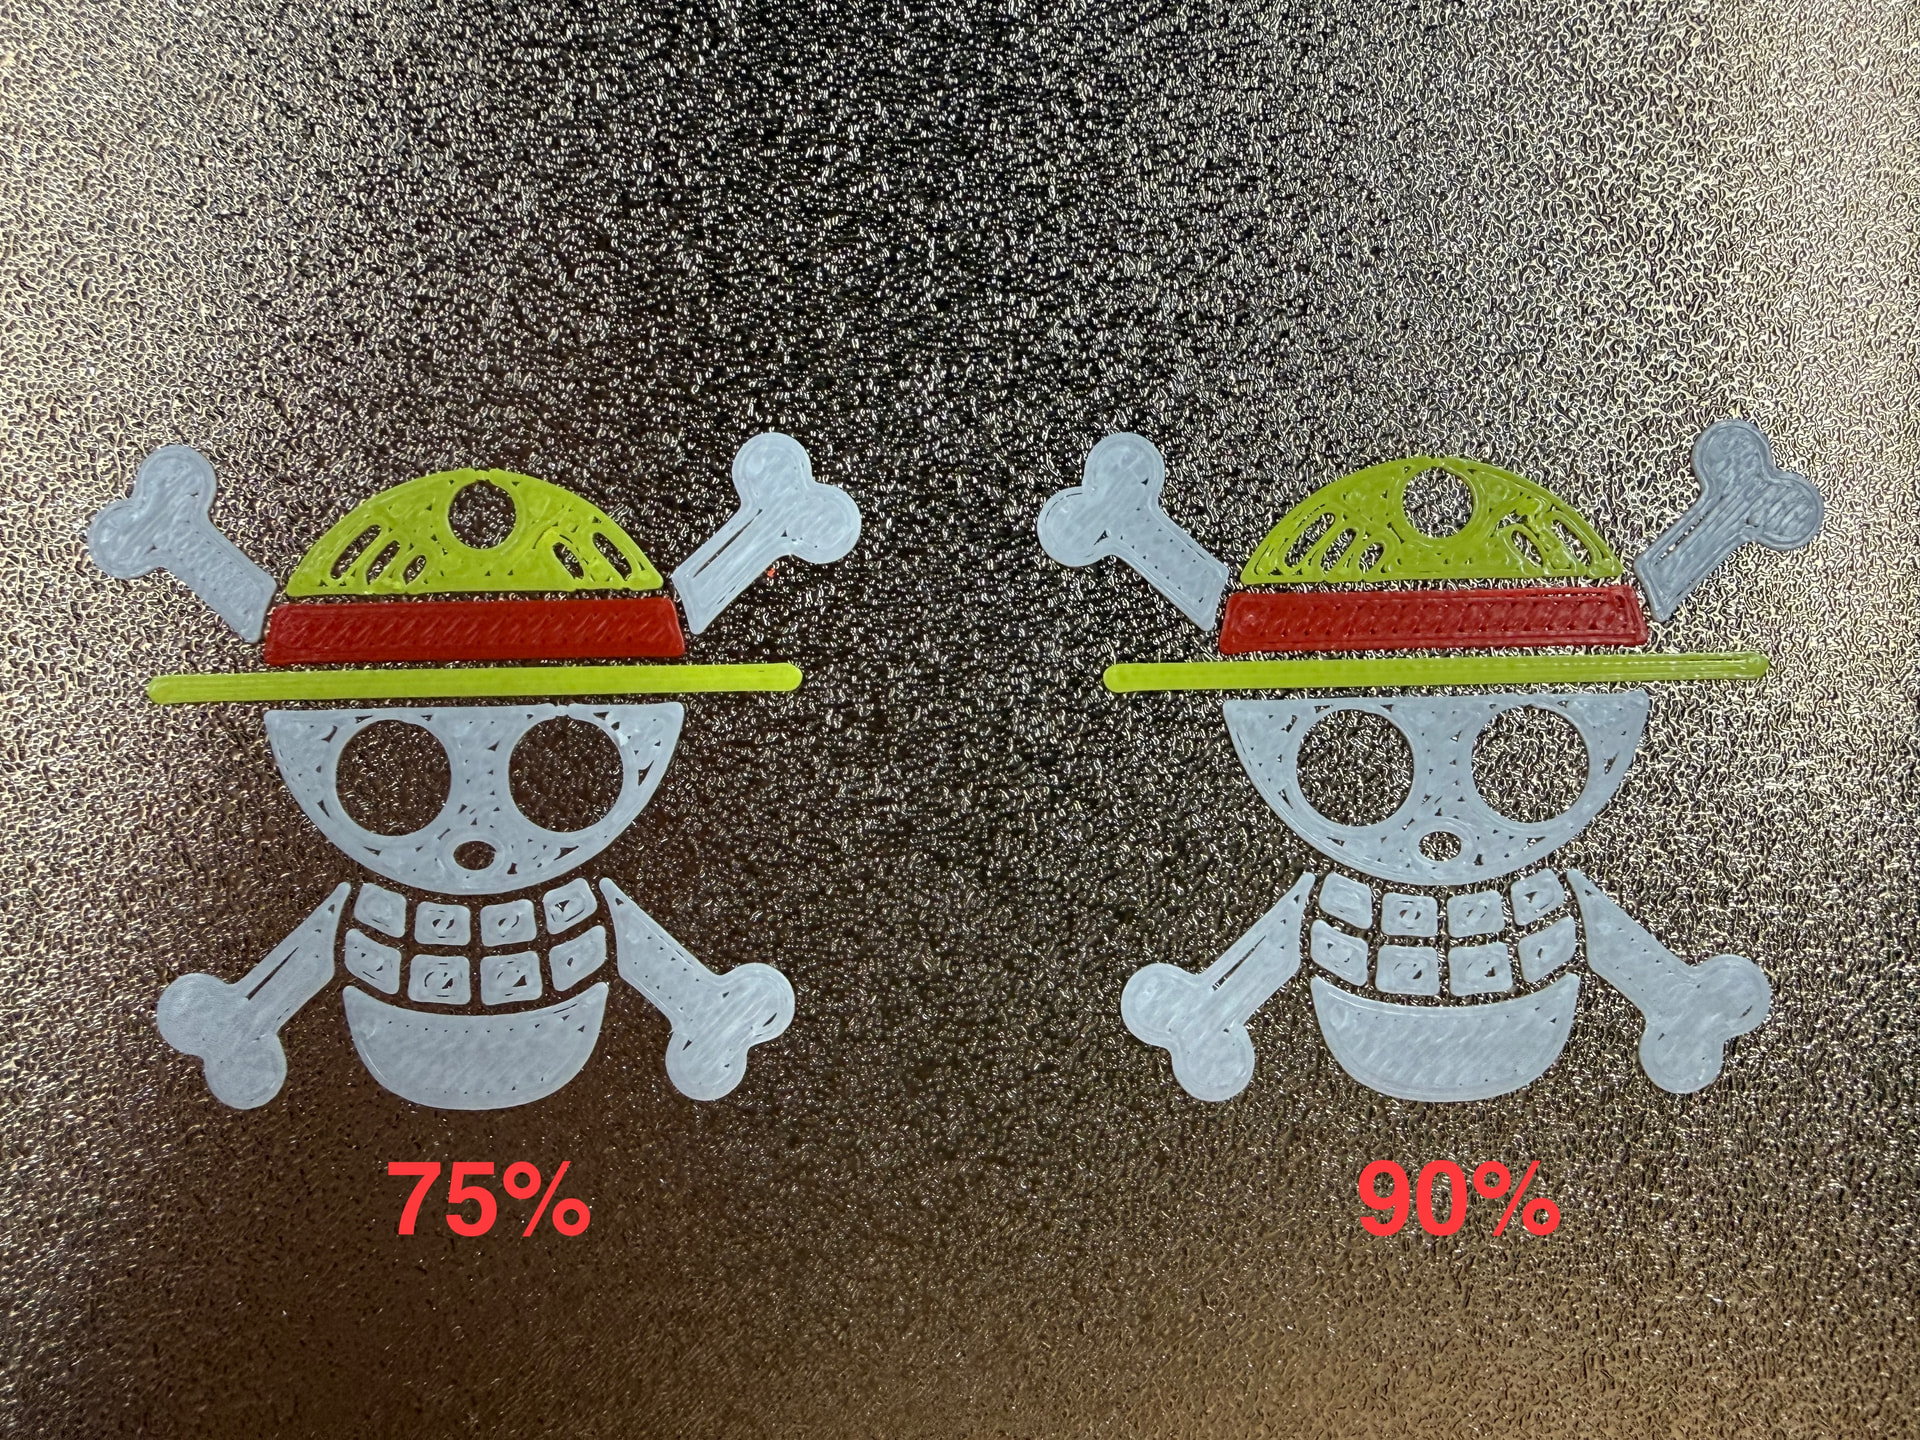
The only workaround posted (developer settings: Monotonic line travel extend), and the one support is pushing after finally getting at least support to review the GitHub page, also doesn’t work - see pictures below:
Have you tried printing with Download OrcaSlicer ? If it is a software issue and not a hardware issue, then OrcaSlicer should narrow down the problem if it is a bug in BambuStudio.

Unfortunately, the H2C is not officially supported in OrcaSlicer at this time.

The profile is currently included in the nightly OrcaSlicer builds as an experimental printer profile. My understanding is that the inclusion is currently modifications pulled from Bambu Studio.

Something I’m willing to try, but hasn’t been high on the priority list considering the above.

Looks like they were having some issues and H2C support has been removed from the nightly builds as of now.

Unfortunately, I haven’t been able to get much attention here in the forums, but it is what it is. I did want to share a quick update for anyone following this:

Bambu support has tested one of my .3mf files and confirmed they are reproducing the same issue internally. I have asked them to escalate to the engineering team and provide a timeline for a fix in a future Bambu Studio release.

Thanks for keeping us updated and especially for the effort you put in to get this issue resolved! I really hope they are (finally) listening and acting. :+1:

This is the one thing that keeps me away from ordering one of the H2-Series printers despite having a true need for the provided capabilities.

Anyway, would be great if someone with a H2S or H2D could provide some test prints of a part sliced with Orca and Bambu Studio.

Hi,

I sent you a PM a few days ago.

Could you send me the 3MF file that Bambu used for testing?

Thanks.

Have you tried changing the top surface pattern from lines to one of these three ?

I found in slicing, these would fill any holes left by straight line travel issues

I have found to increase the flowrate to 1 to 1.02 quite helpful…

Just replied with the model

I will add I’ve had the same ticket open since 29 APRIL and have been back and forth since them with multiple tests suggestions all to be continually shutdown. As if they don’t see the gaps, lines inconsistencies.
My latest response from Bambu Support:

2026-07-28 20:15:12
Dear Customer,

Thanks for the update!

We tested the same print on an H2C, and the results were generally similar to yours. It is possible that dual-nozzle multi-color printing may be less stable than single-nozzle multi-color printing due to the technical characteristics of the dual-nozzle system.

Unfortunately, this is a limitation of the current technology, and we are unable to further improve the result through adjustments at this time.

Thank you for your understanding.

Best regards,
Bambu Lab Customer Support

In their words or to the like, it’s a Flagship machine, purpose built for multi colour, multi nozzle. Even recommends they use of both left and right nozzles within prints.

I really don’t know what to say to their response!!

This is definitely a weird response, unless your issue is different than the OP’s one.
In th images shown the issue is within one colored region.

Judging by the response to you, there is probably a different case here.

Can you share images of your issue?

For Clarification:

I purchased a Bambu Lab H2C expecting reliable dual-nozzle, multi-colour printing.

Order Timeline

Order placed: 15 April 2026
Shipped: 16 April 2026
Delivered: 21 April 2026

I reported my first print quality issues on 29 April 2026, just 8 days after delivery, and have been working with Bambu Lab Support ever since.

Main Issue

From the beginning, the printer has produced inconsistent first-layer quality, particularly during dual-nozzle and multi-colour printing. The issues include:

Visible first-layer lines and gaps.
Inconsistent extrusion quality between the left and right nozzles.
Poor bonding between colours.
Print quality varying between identical prints without any setting changes.
Results significantly worse than my Bambu A1 printing the same files using the same Bambu filaments.
Troubleshooting Completed

Over the past three months I have fully cooperated with every troubleshooting request, including:

Multiple full machine calibrations and factory reset.
Automatic and manual filament calibrations.
Nozzle offset calibrations before printing.
Flow ratio adjustments and speed changes.
Testing numerous filaments and nozzle combinations.
Printing supplied Bambu test files.
Supplying multiple 3MF project files.
Providing extensive photos and detailed comparisons.
Installing replacement hardware supplied under warranty, including a left hotend heating assembly and nozzle lifting rail.

Despite all of these steps, the problem has never been resolved and the print quality remains inconsistent.

Current Position

In Bambu Lab’s most recent response, support advised that:

They printed my supplied files on their own H2C.
Their results were generally similar to mine.
Dual-nozzle multi-colour printing may be less stable due to the characteristics of the system.
They consider this a limitation of the current technology.
They are unable to further improve the results through additional adjustments.

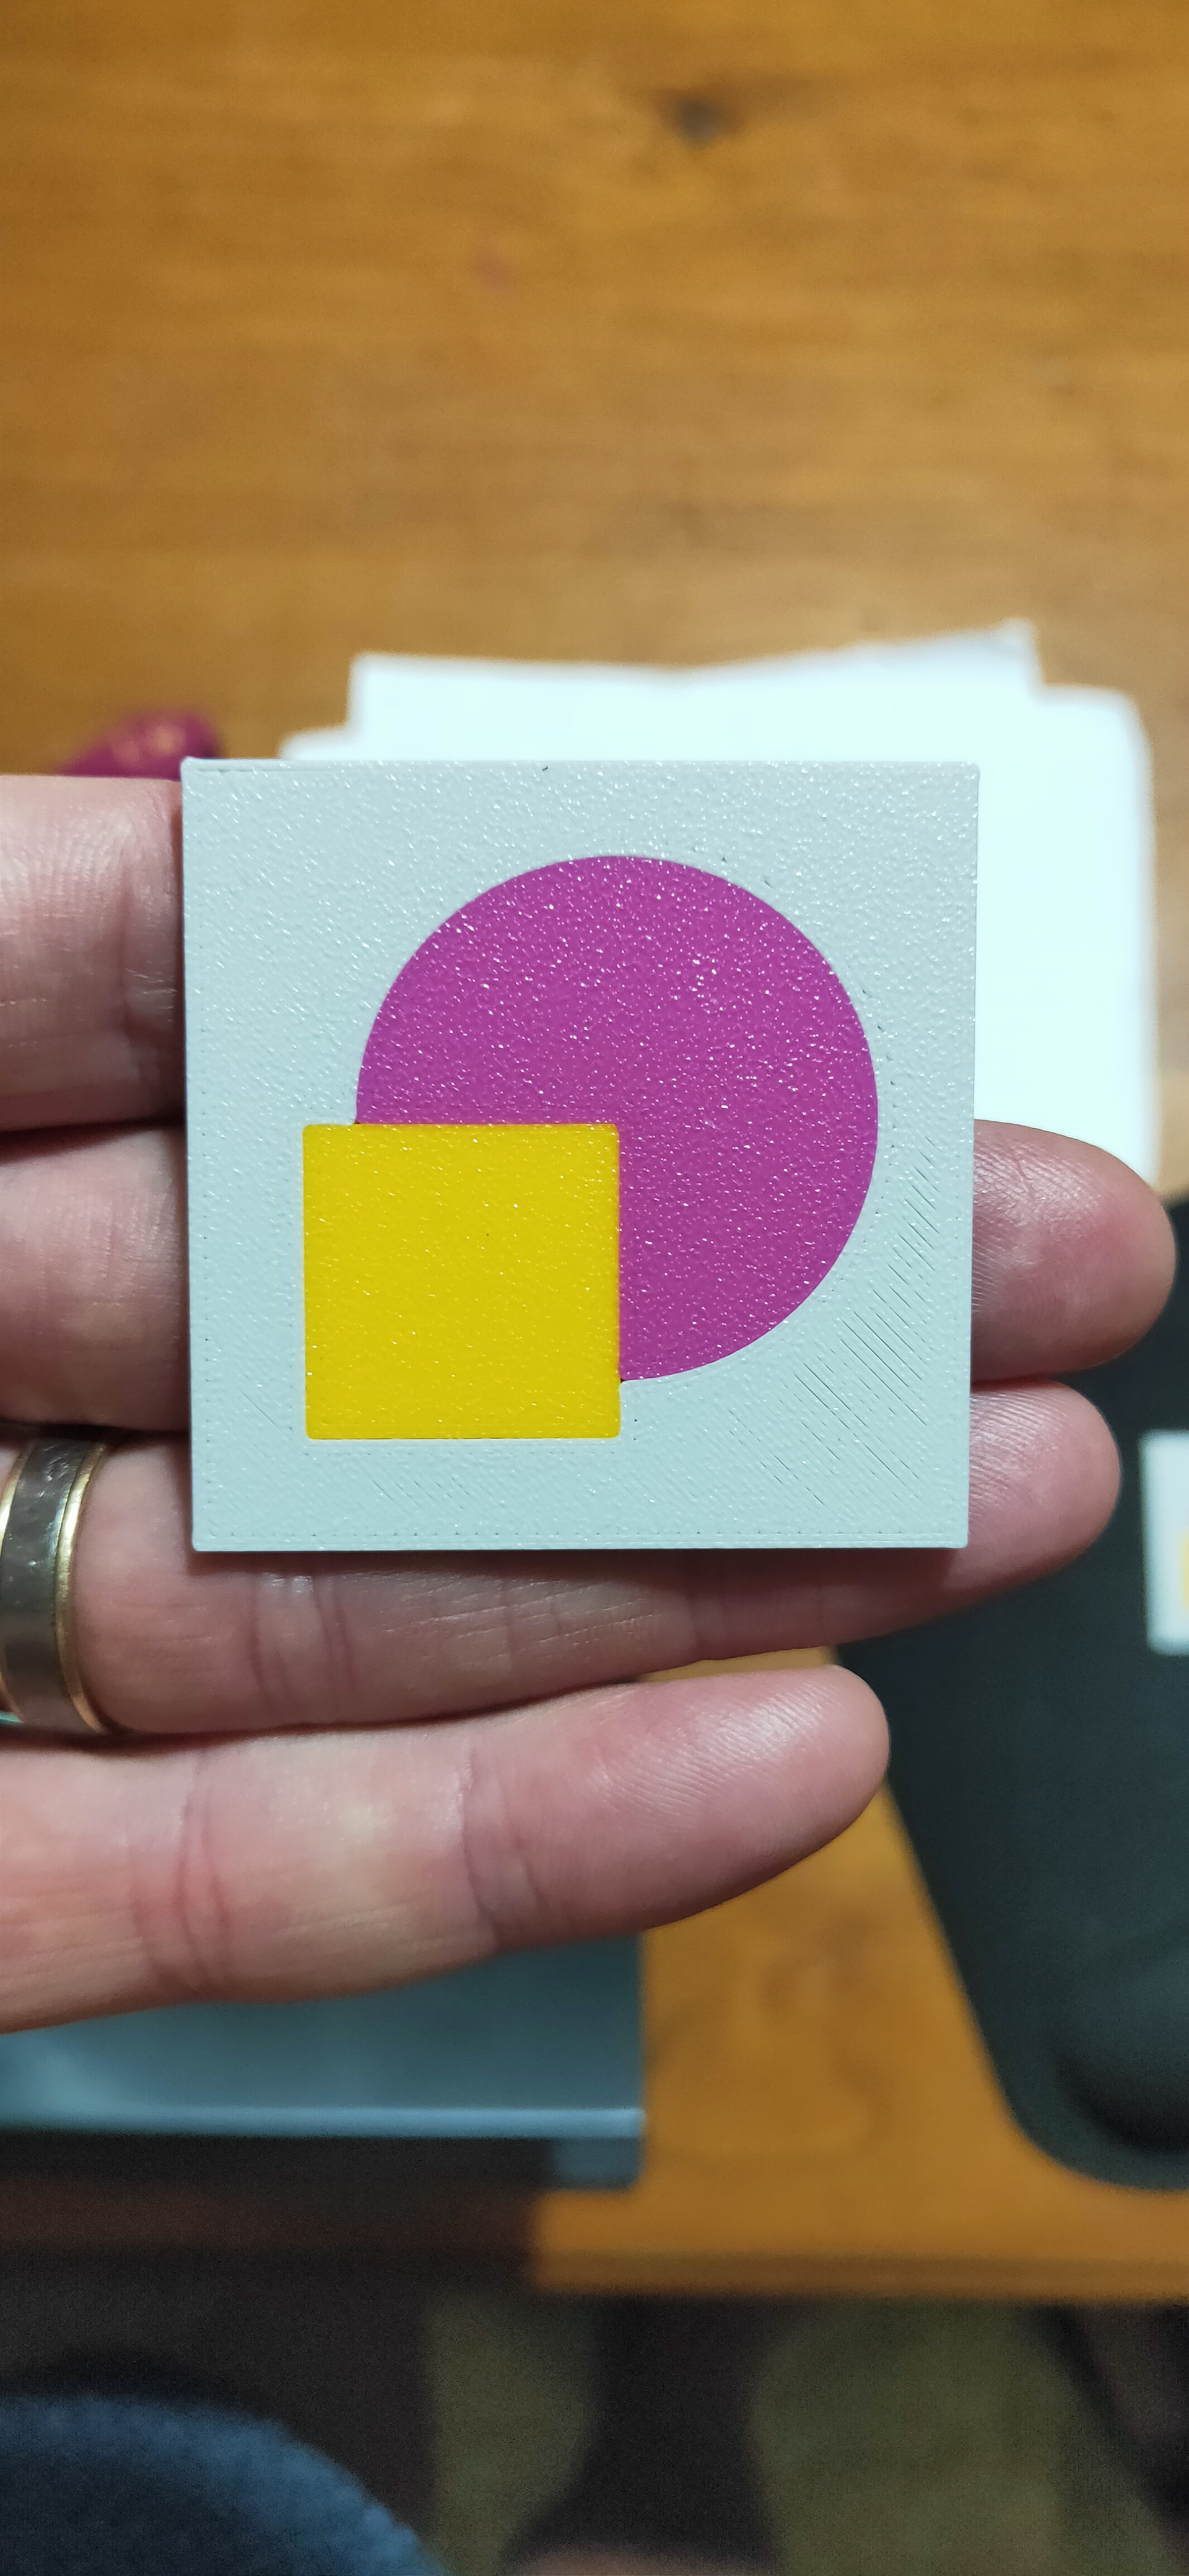
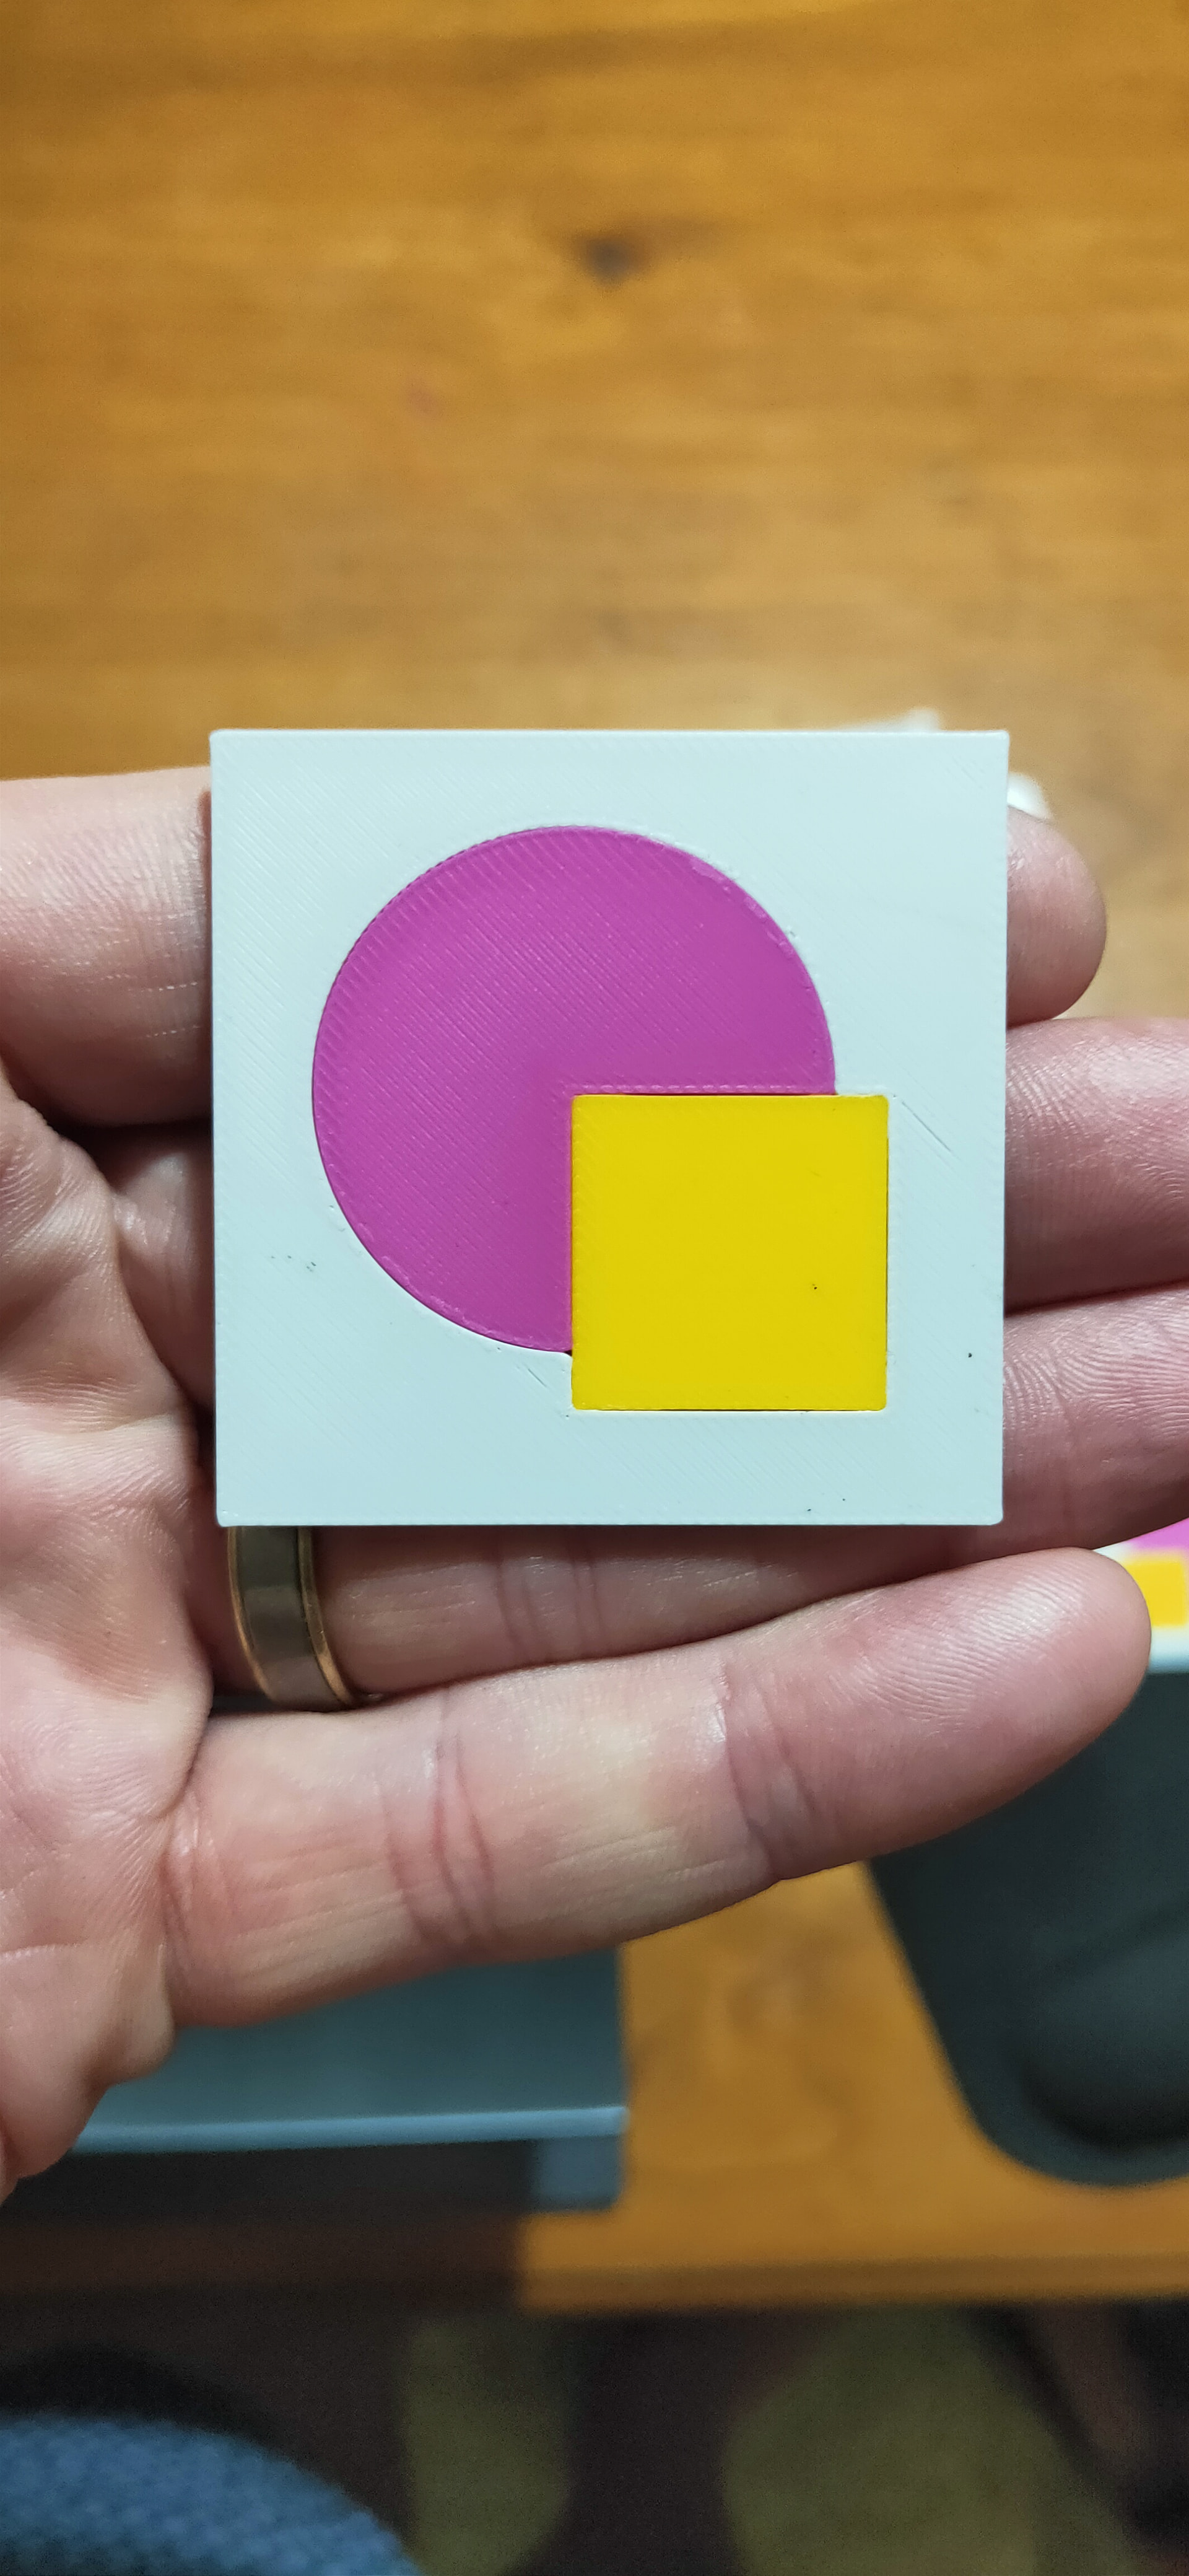
Here are some example photos of my current results,
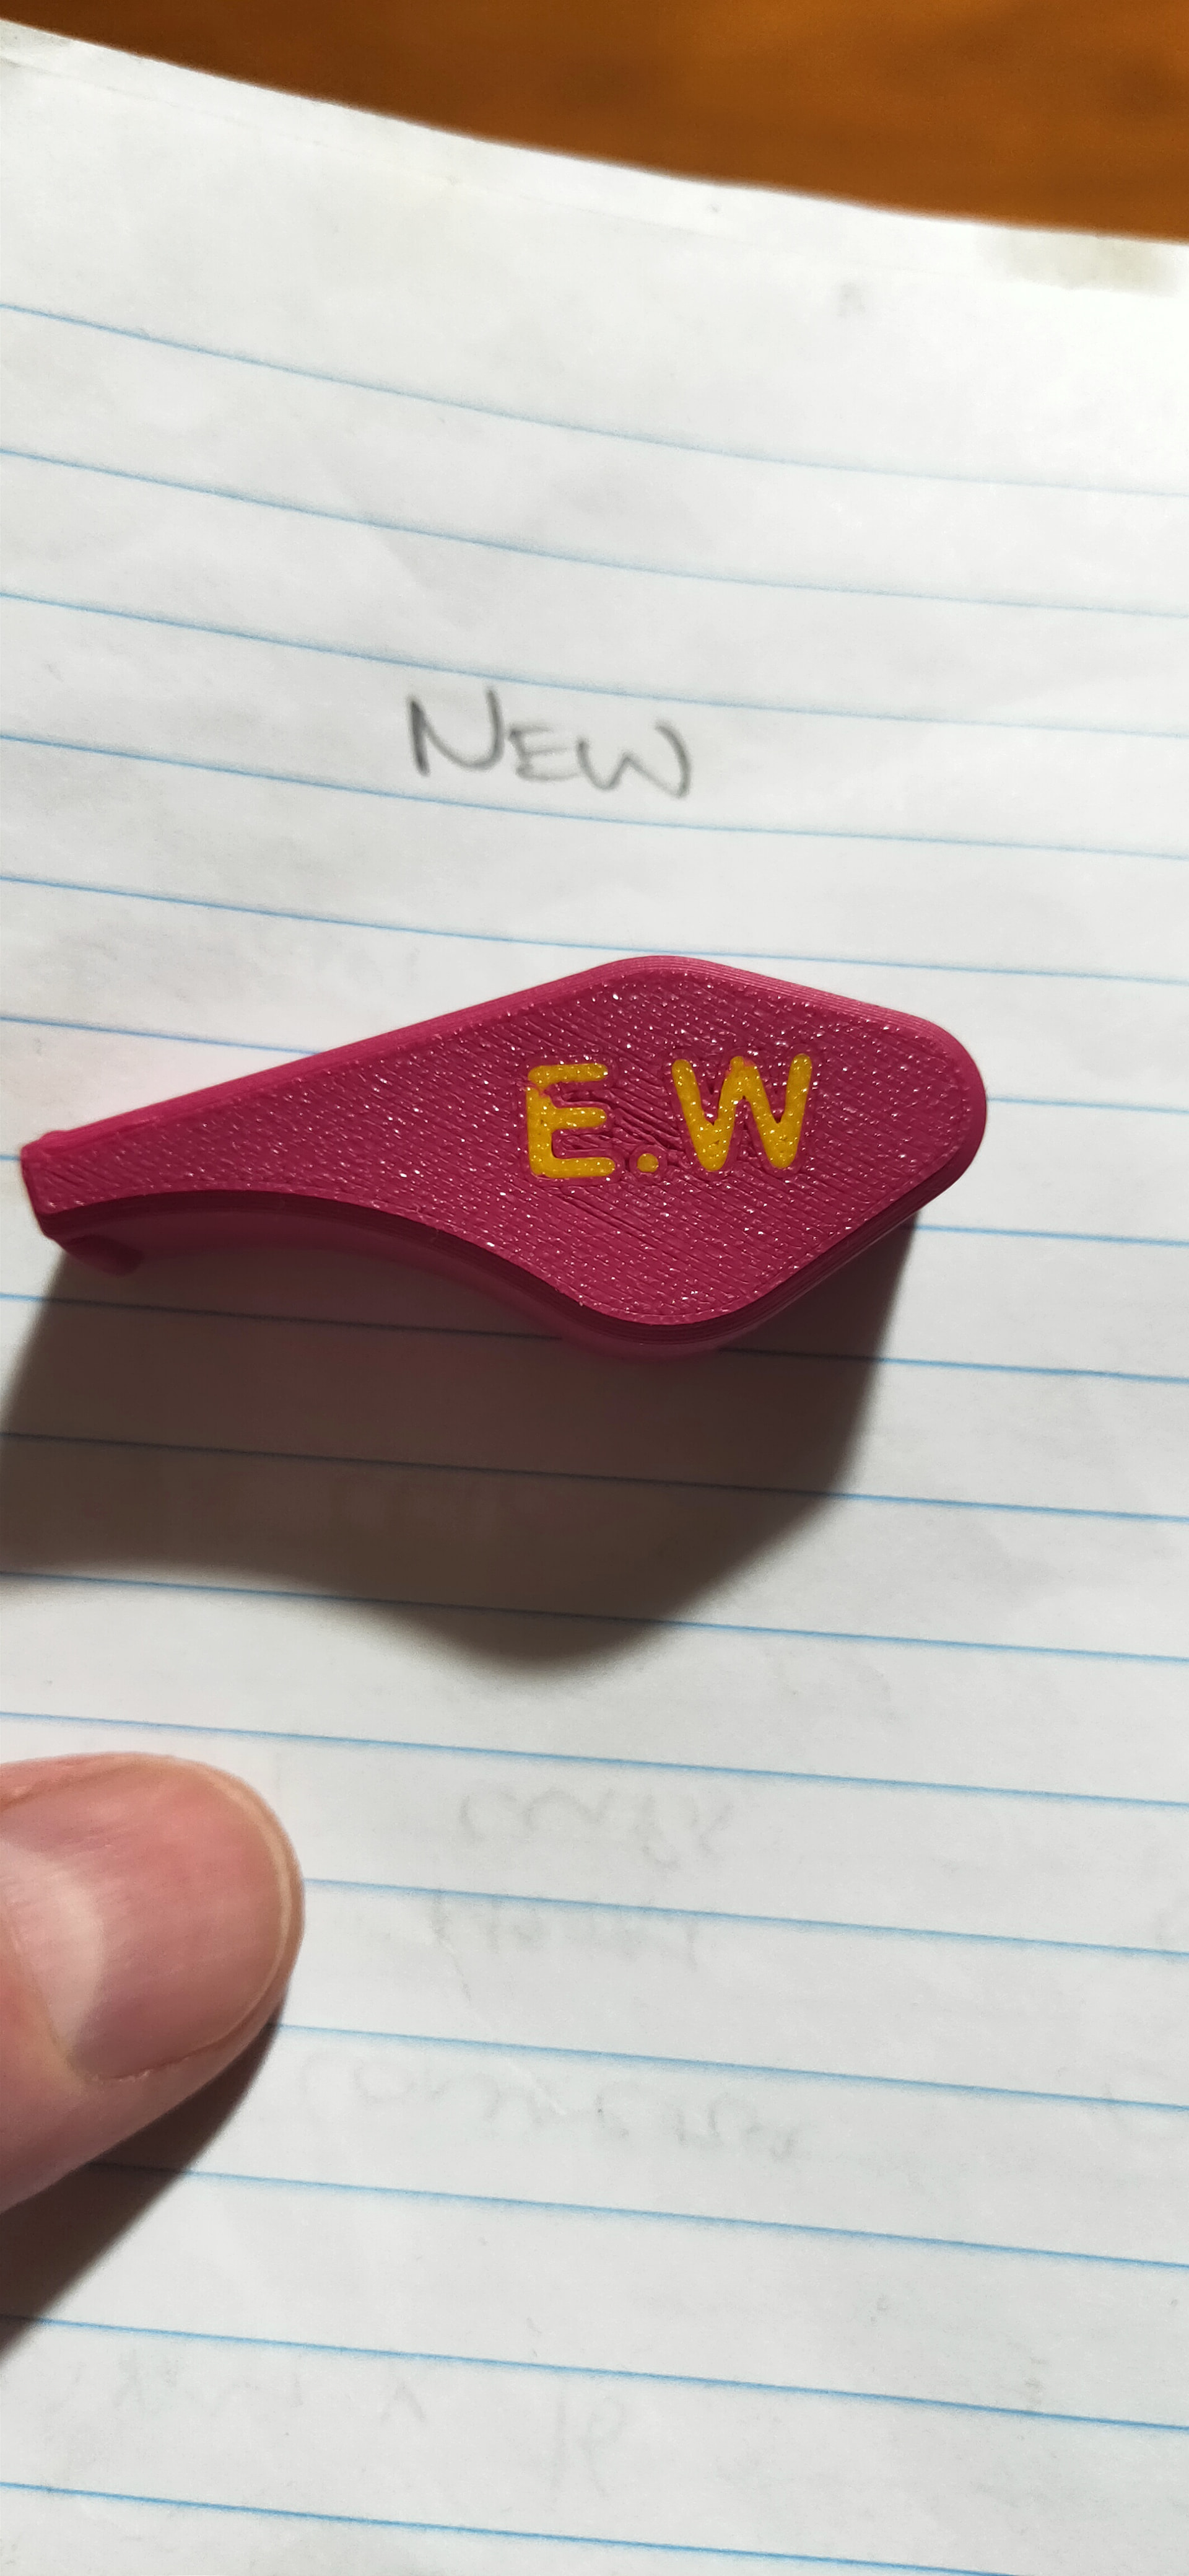
The purple whistle is with all of their parameters to slow initial layer speeds and i added increase flow 1.05 and tried 1.1 no better:
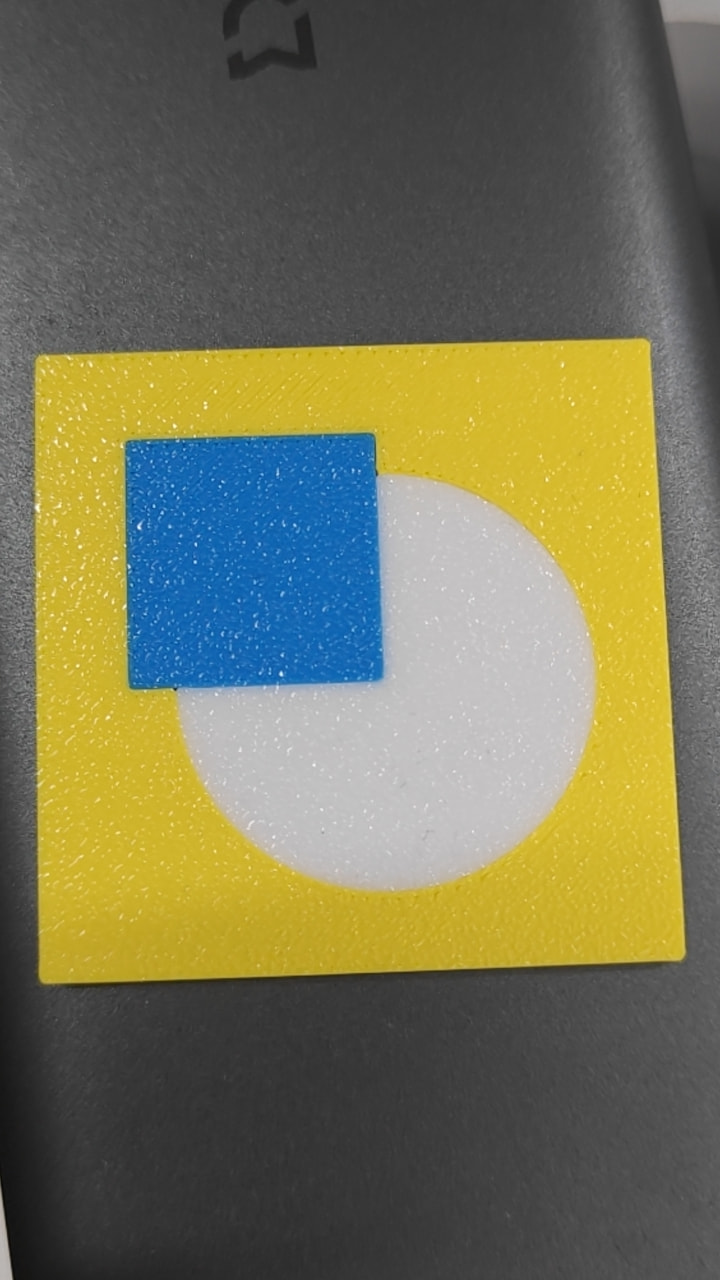
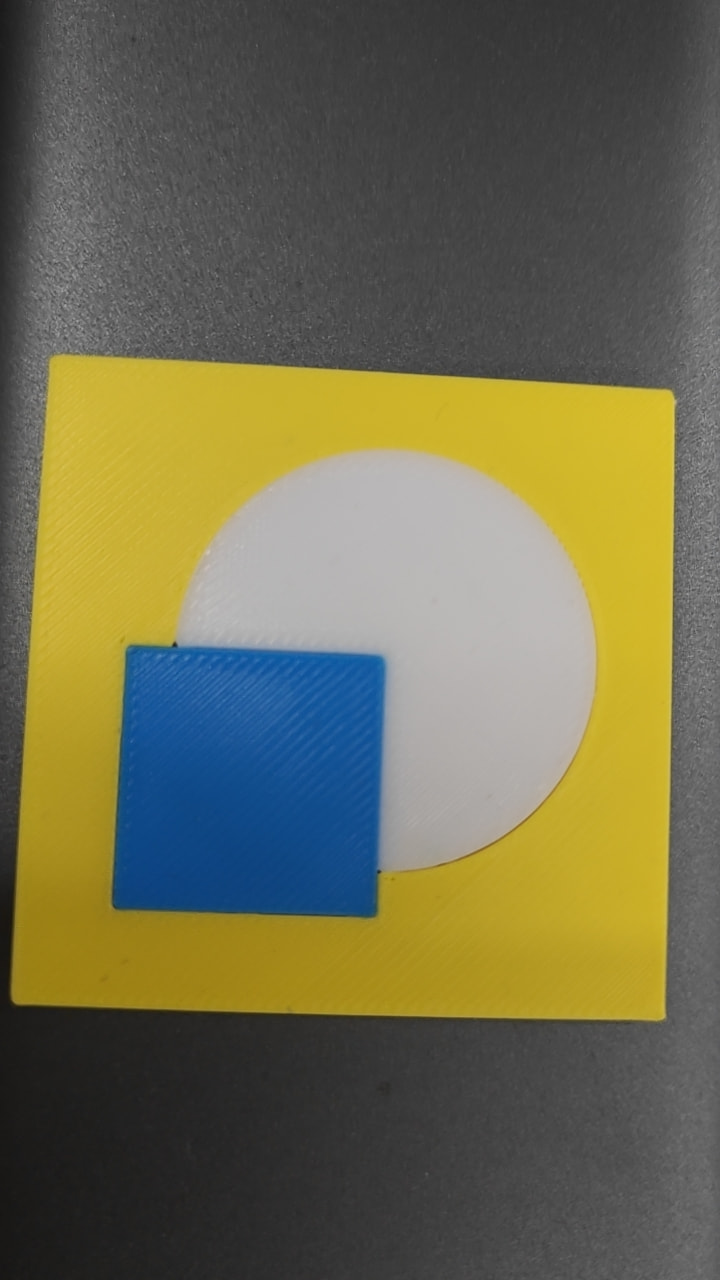
The yellow square with Blues square and white circle is their results.

What you’re showing is inevitable for FDM.

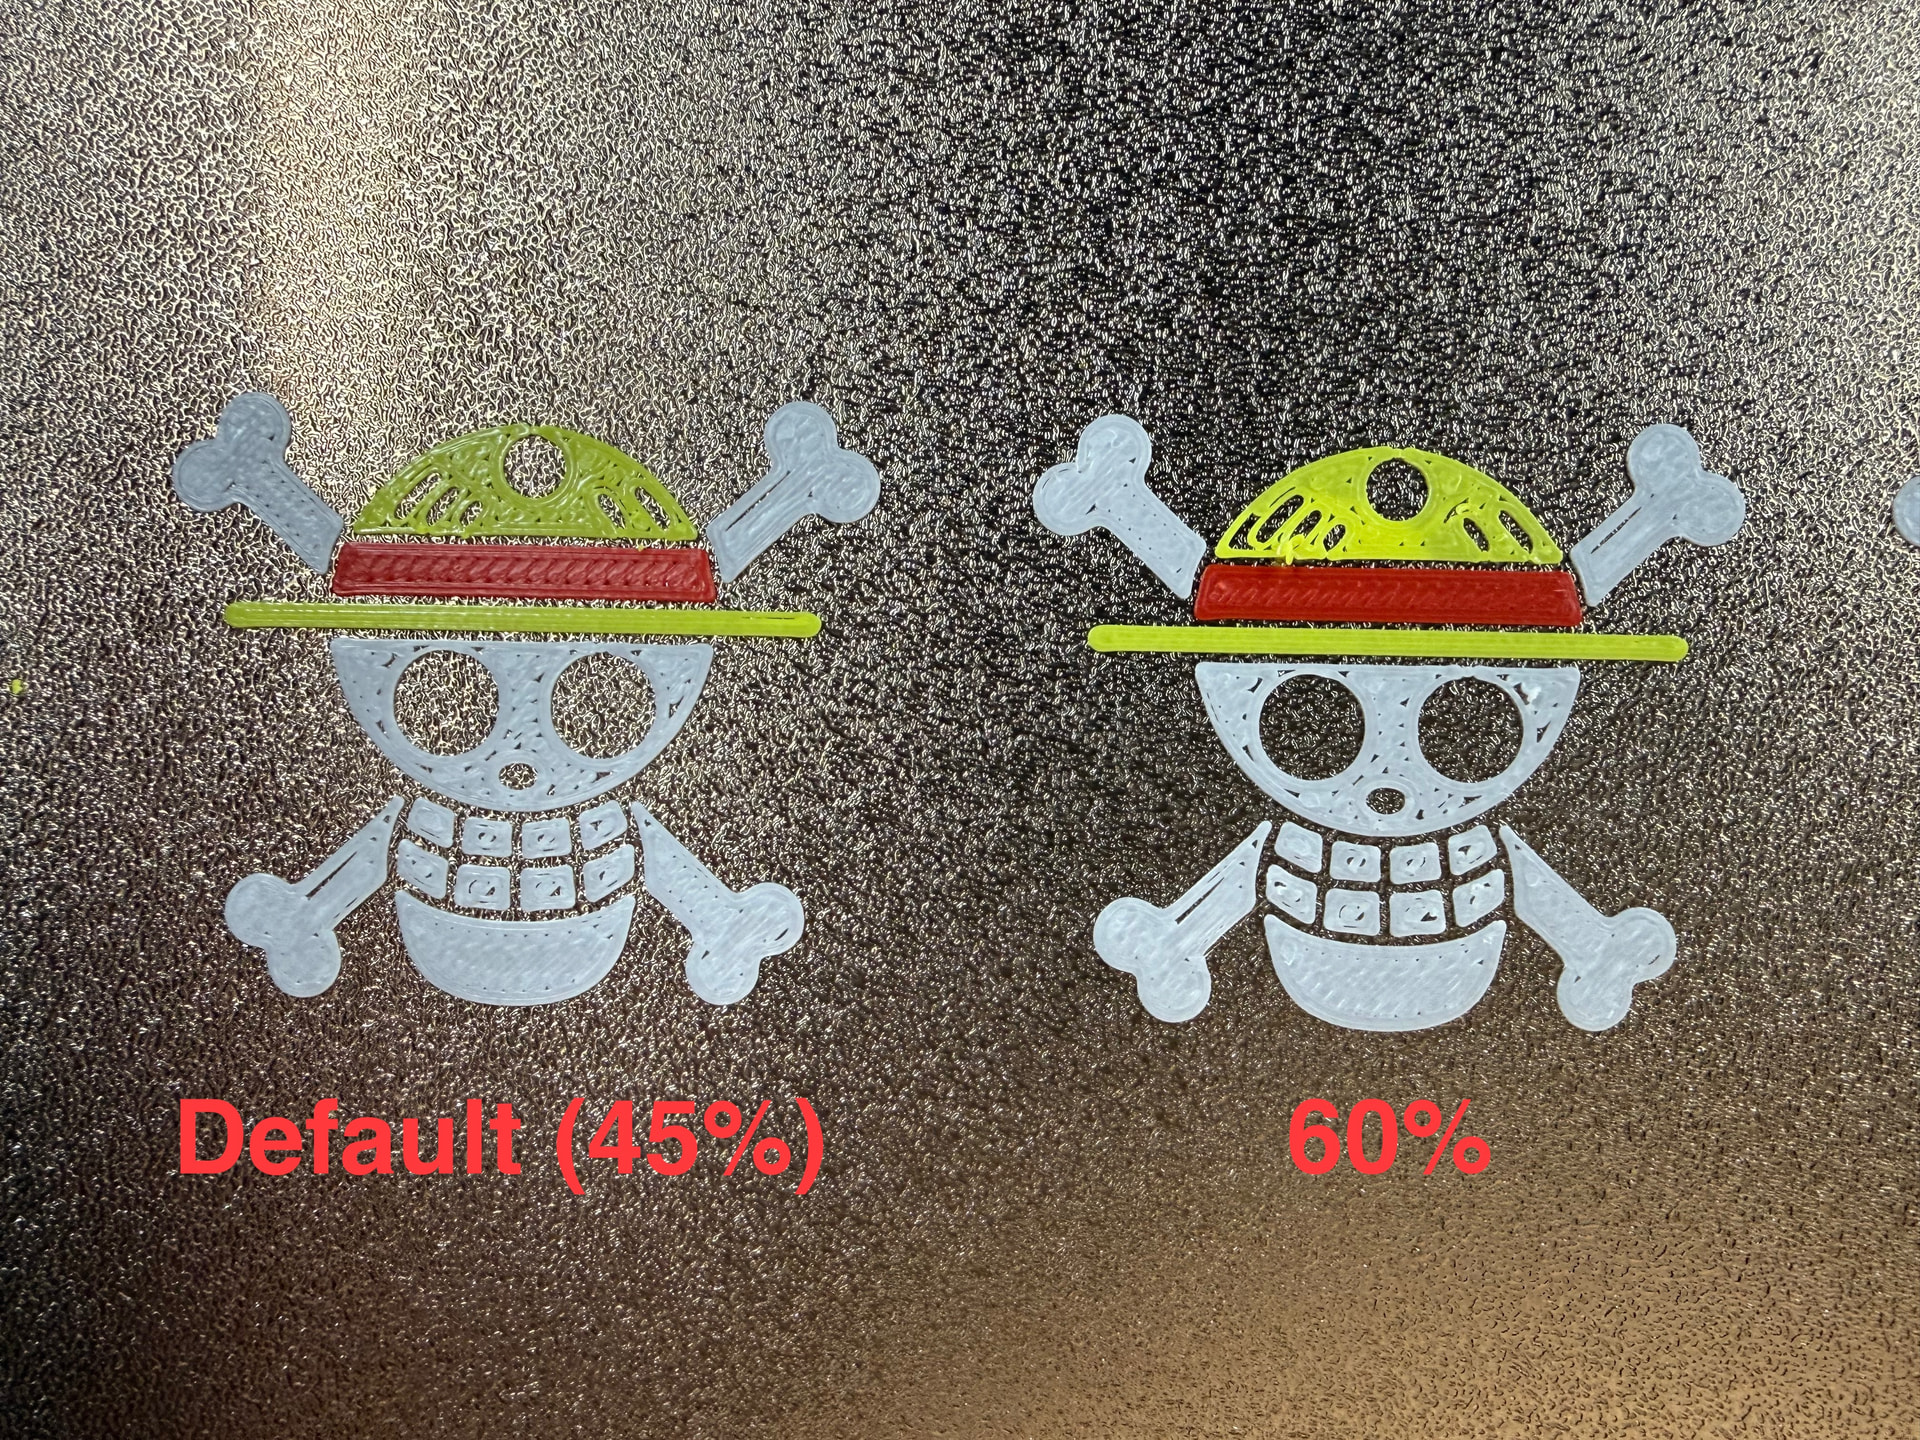
There would be some workarounds, some band aids, but there won’t be a full solution. Remember that you’re plotting 0.42mm lines and they should not cross each other. Now use that rule to draw something like this:

You won’t be able to draw without any holes either.

Here is just one example I printed tonight on my A1 all default setting:

And another with an increase to initial flow to 1.05:

and here is the example printed on my H2C, initial flow 1.05, initial layer and infill speeds reduced:

I understand that some small gaps are an inherent limitation of FDM printing, particularly around complex colour boundaries. That’s not really what I’m questioning.

My concern is the overall consistency and quality of the first layer.

Every comparison I’ve submitted has been printed using the same Bambu filament and the same print files. On my Bambu A1, those same files produce a much cleaner result using completely default settings.

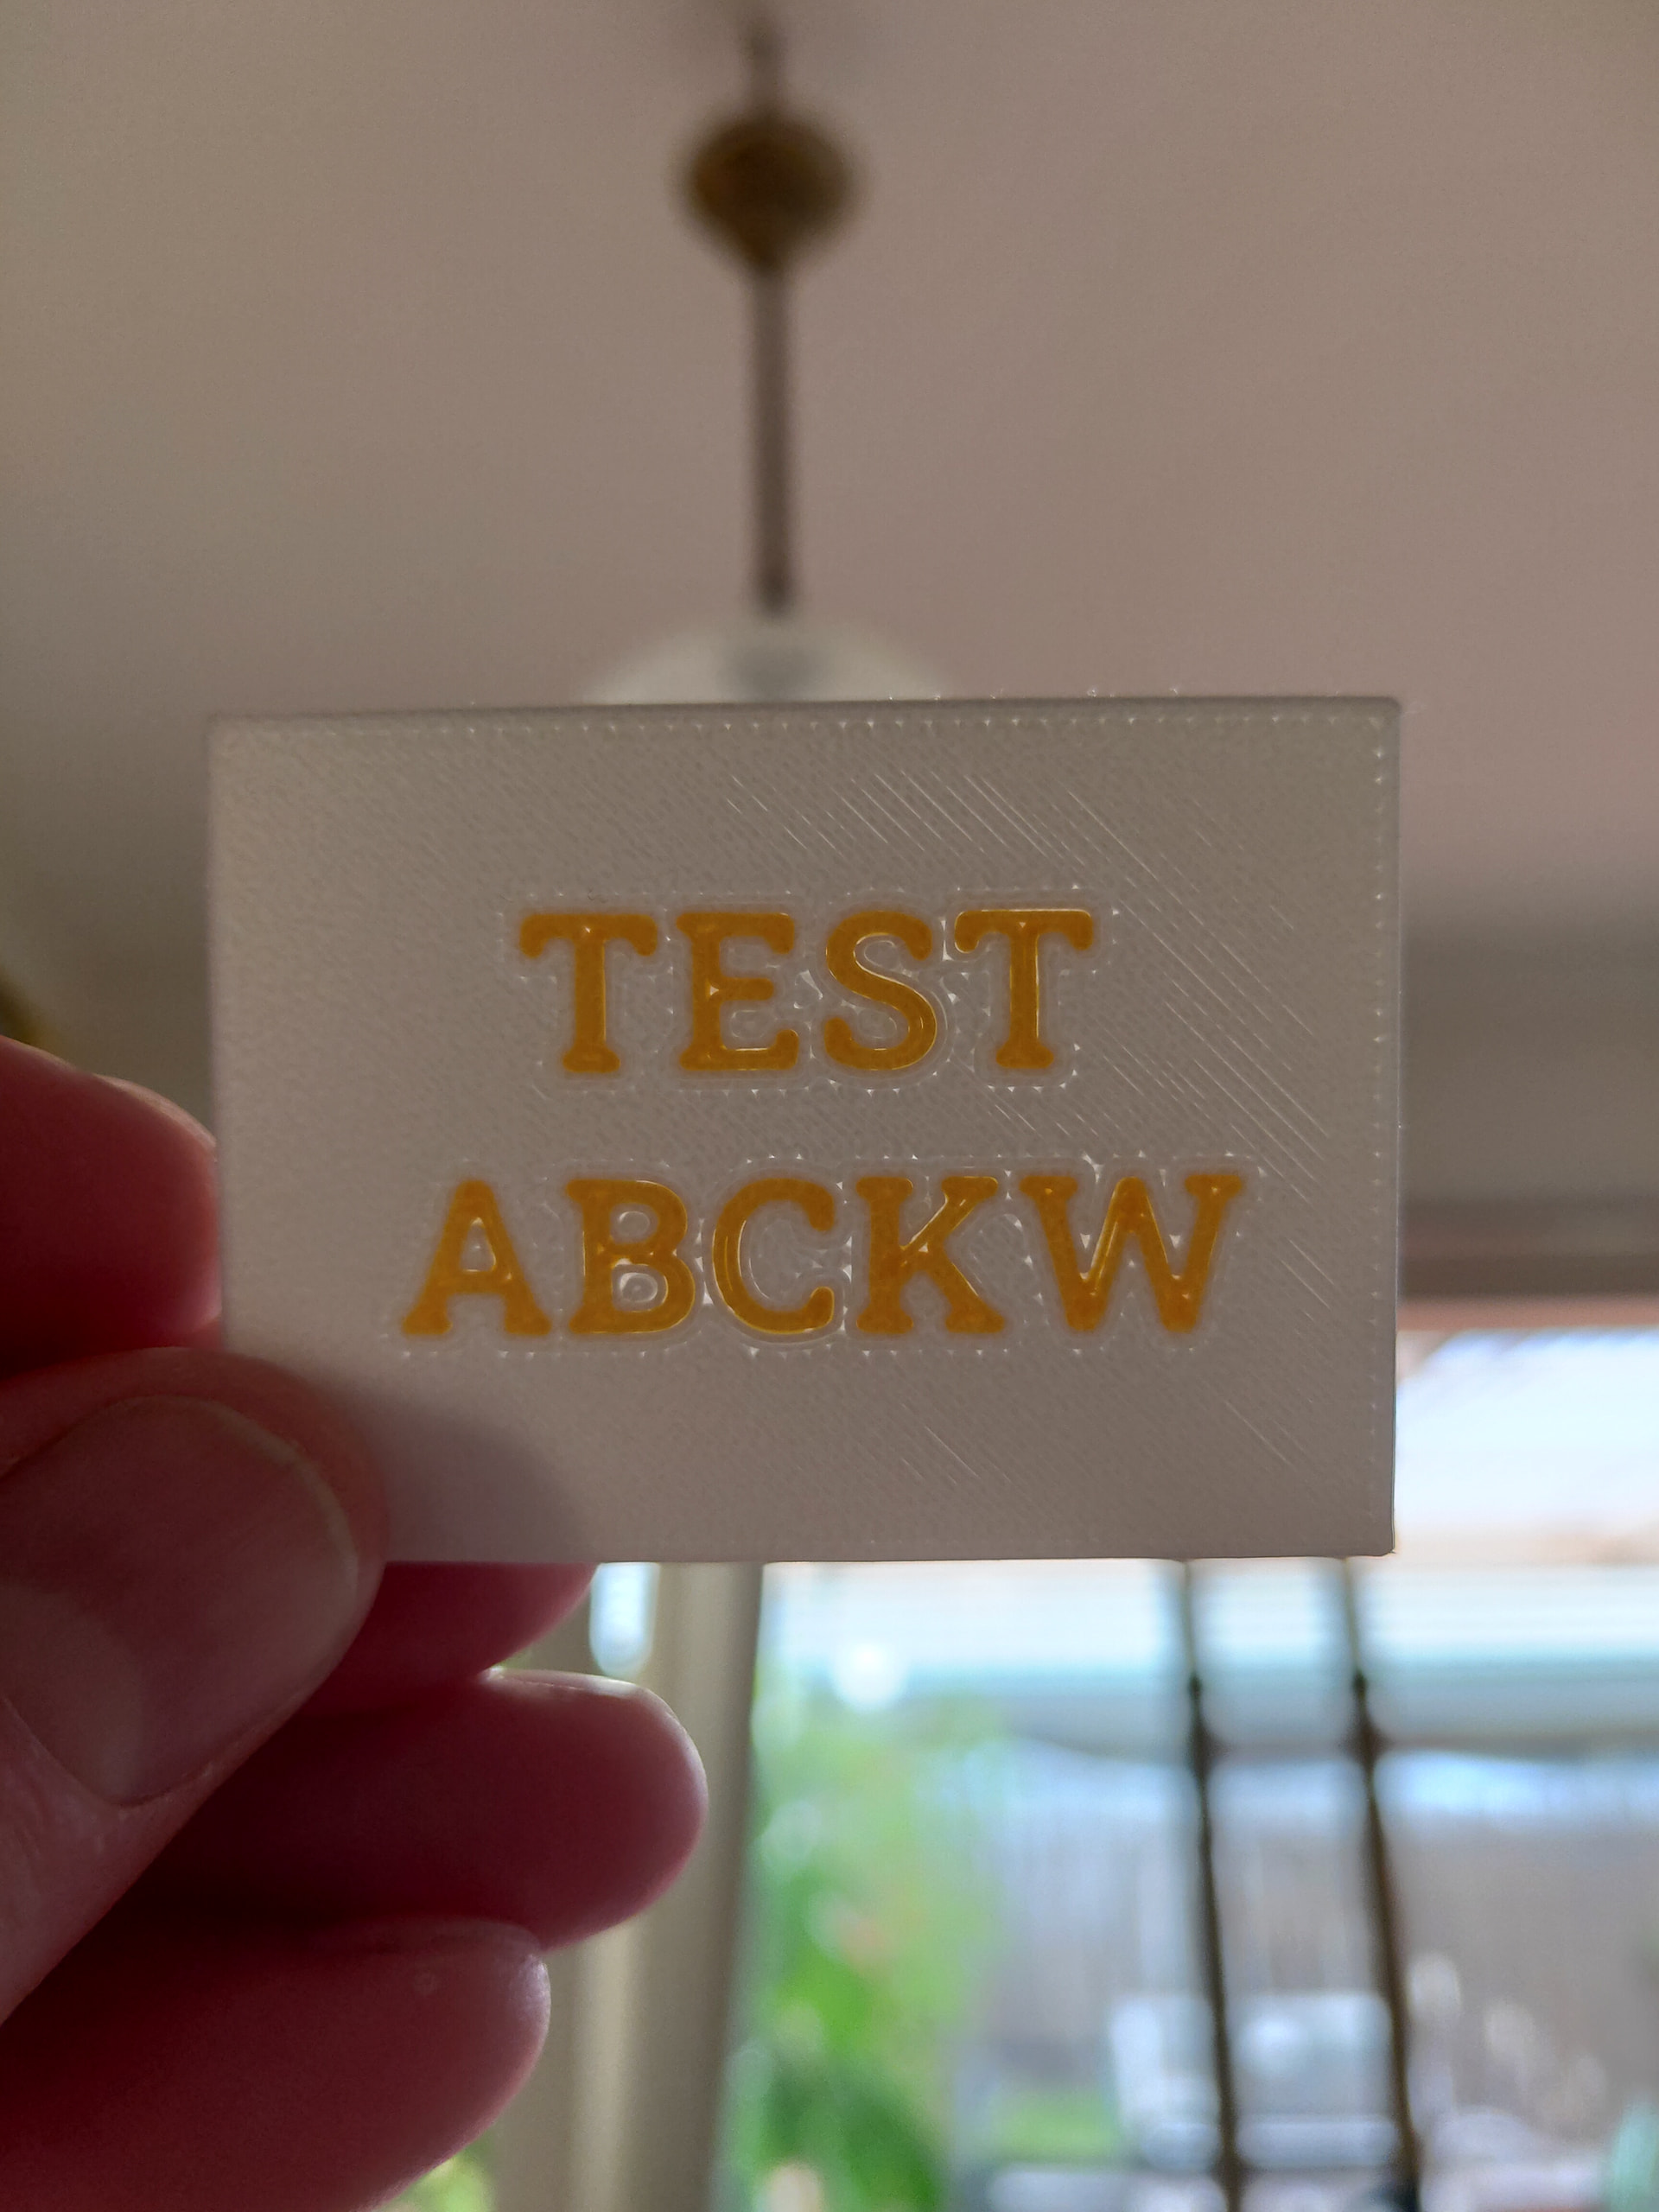
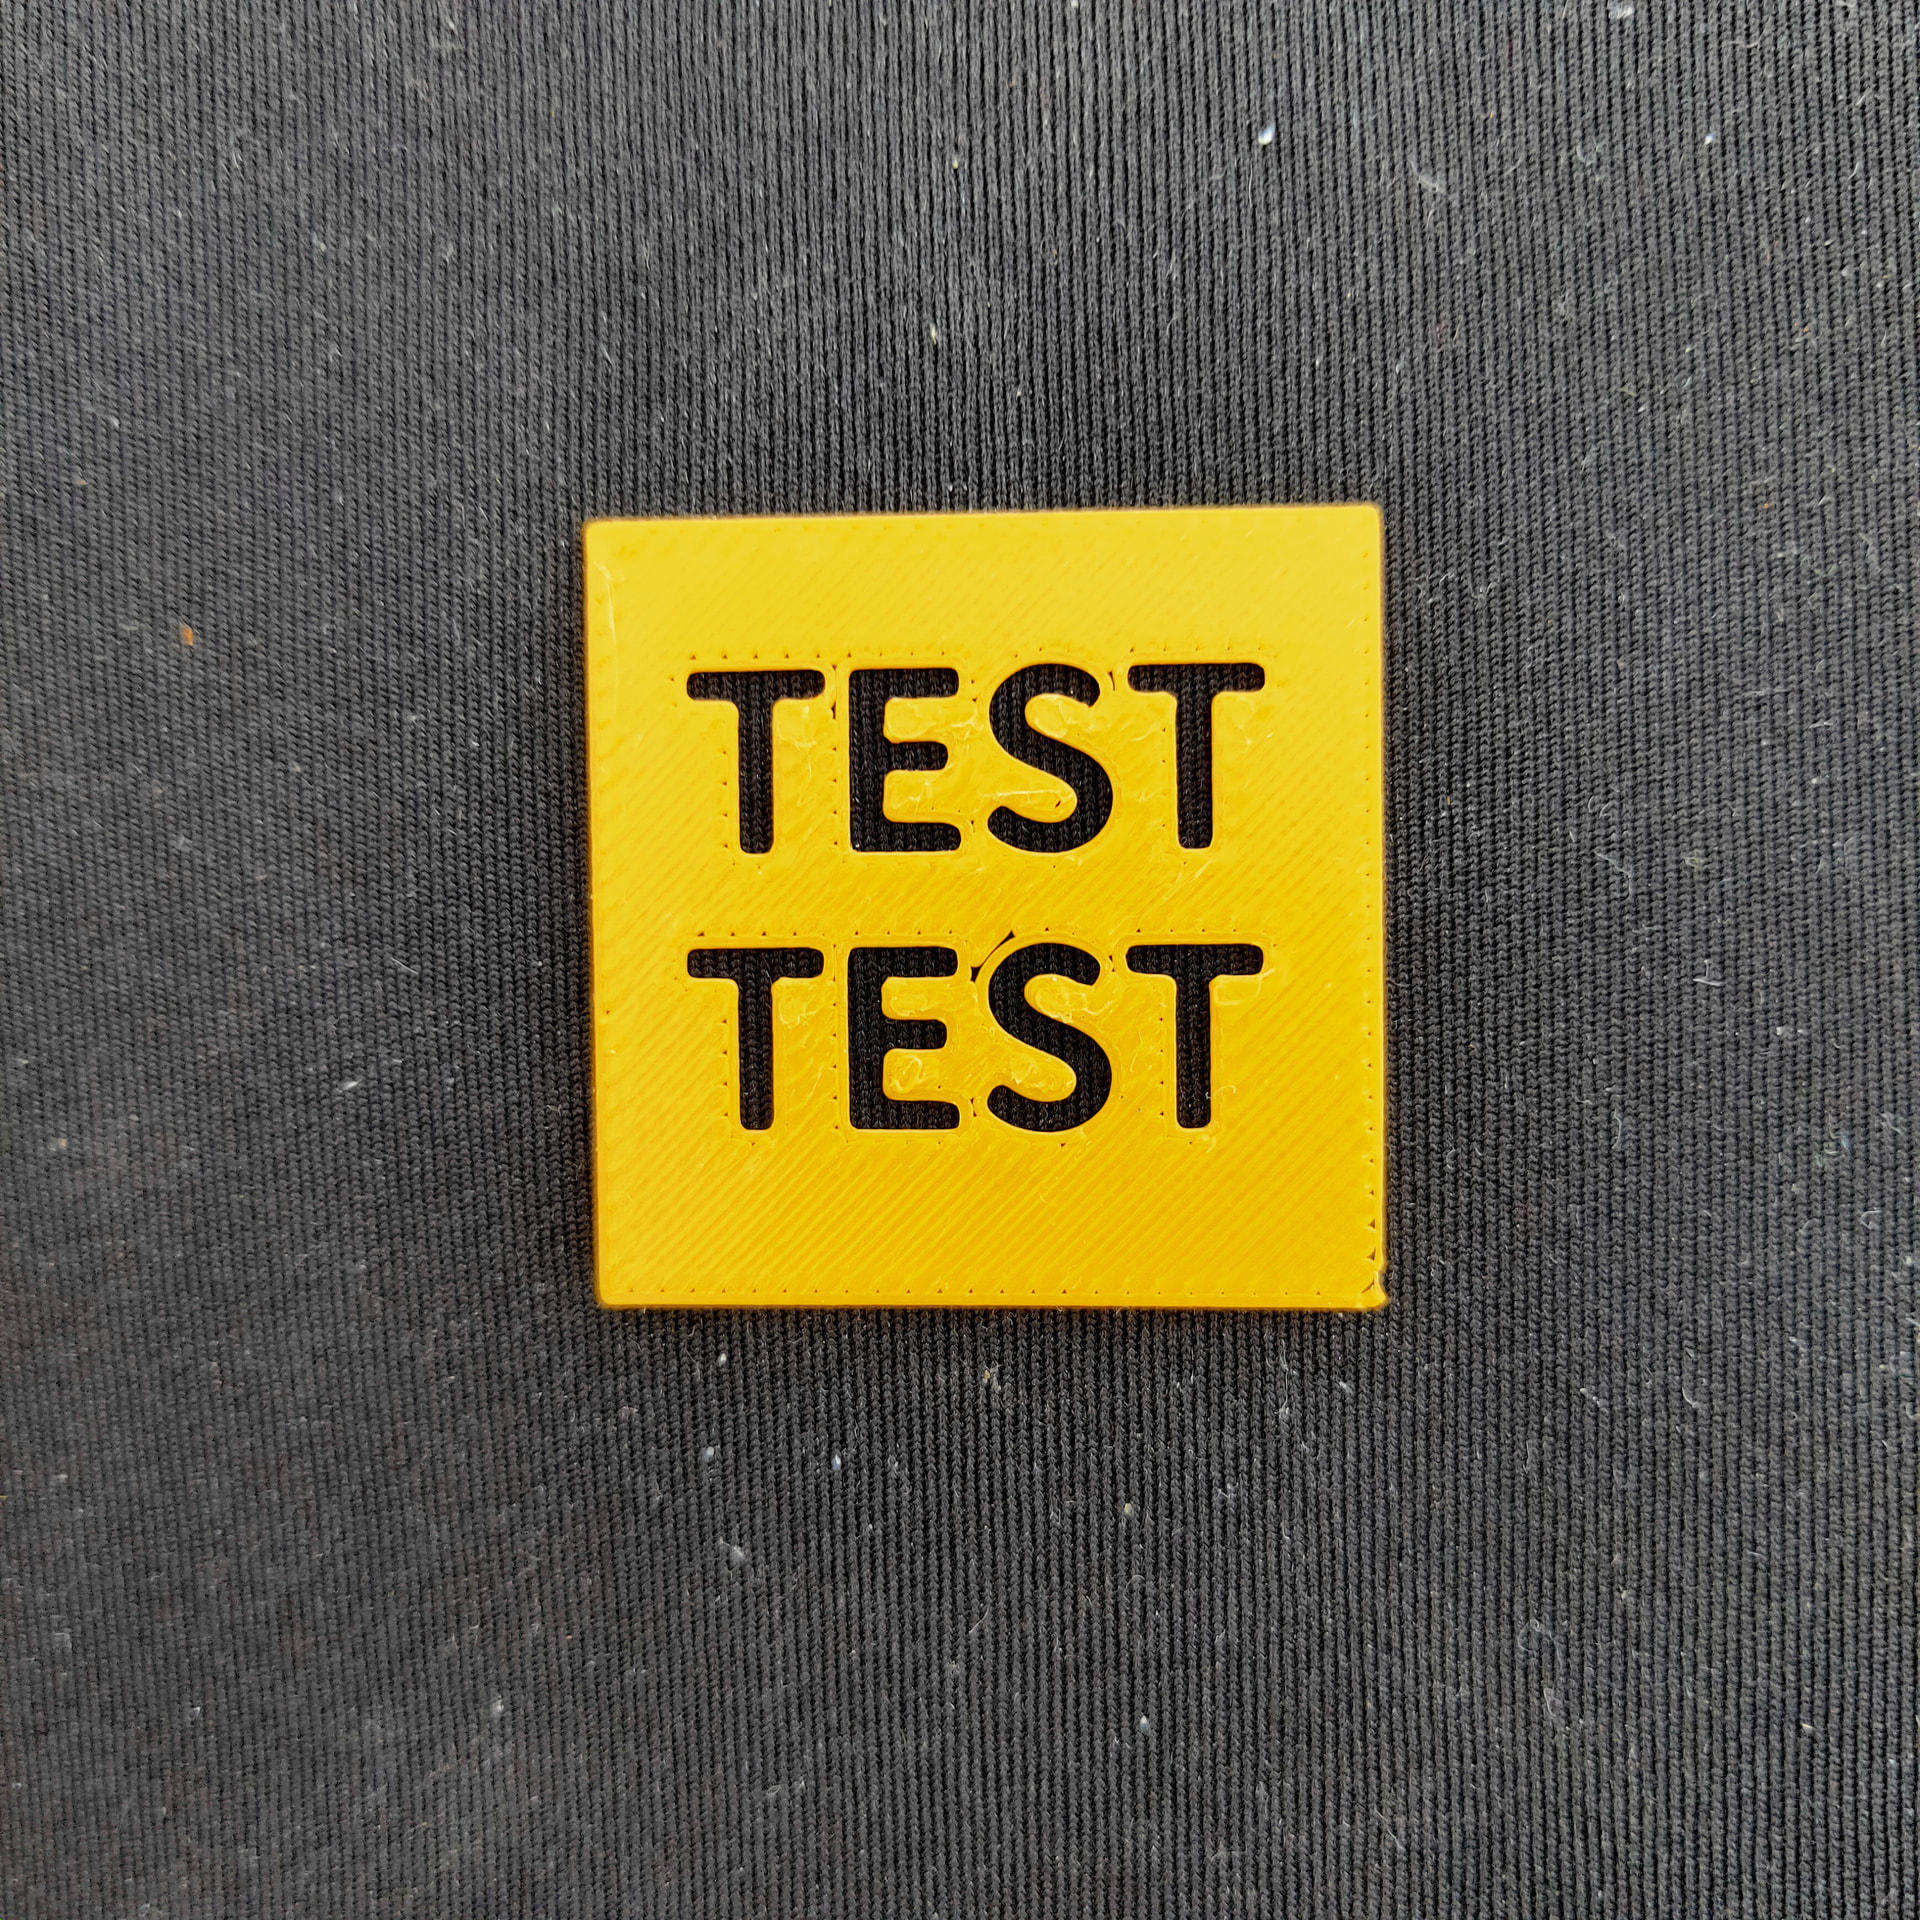
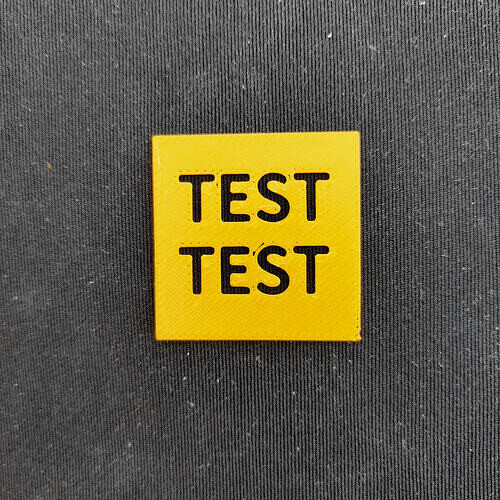
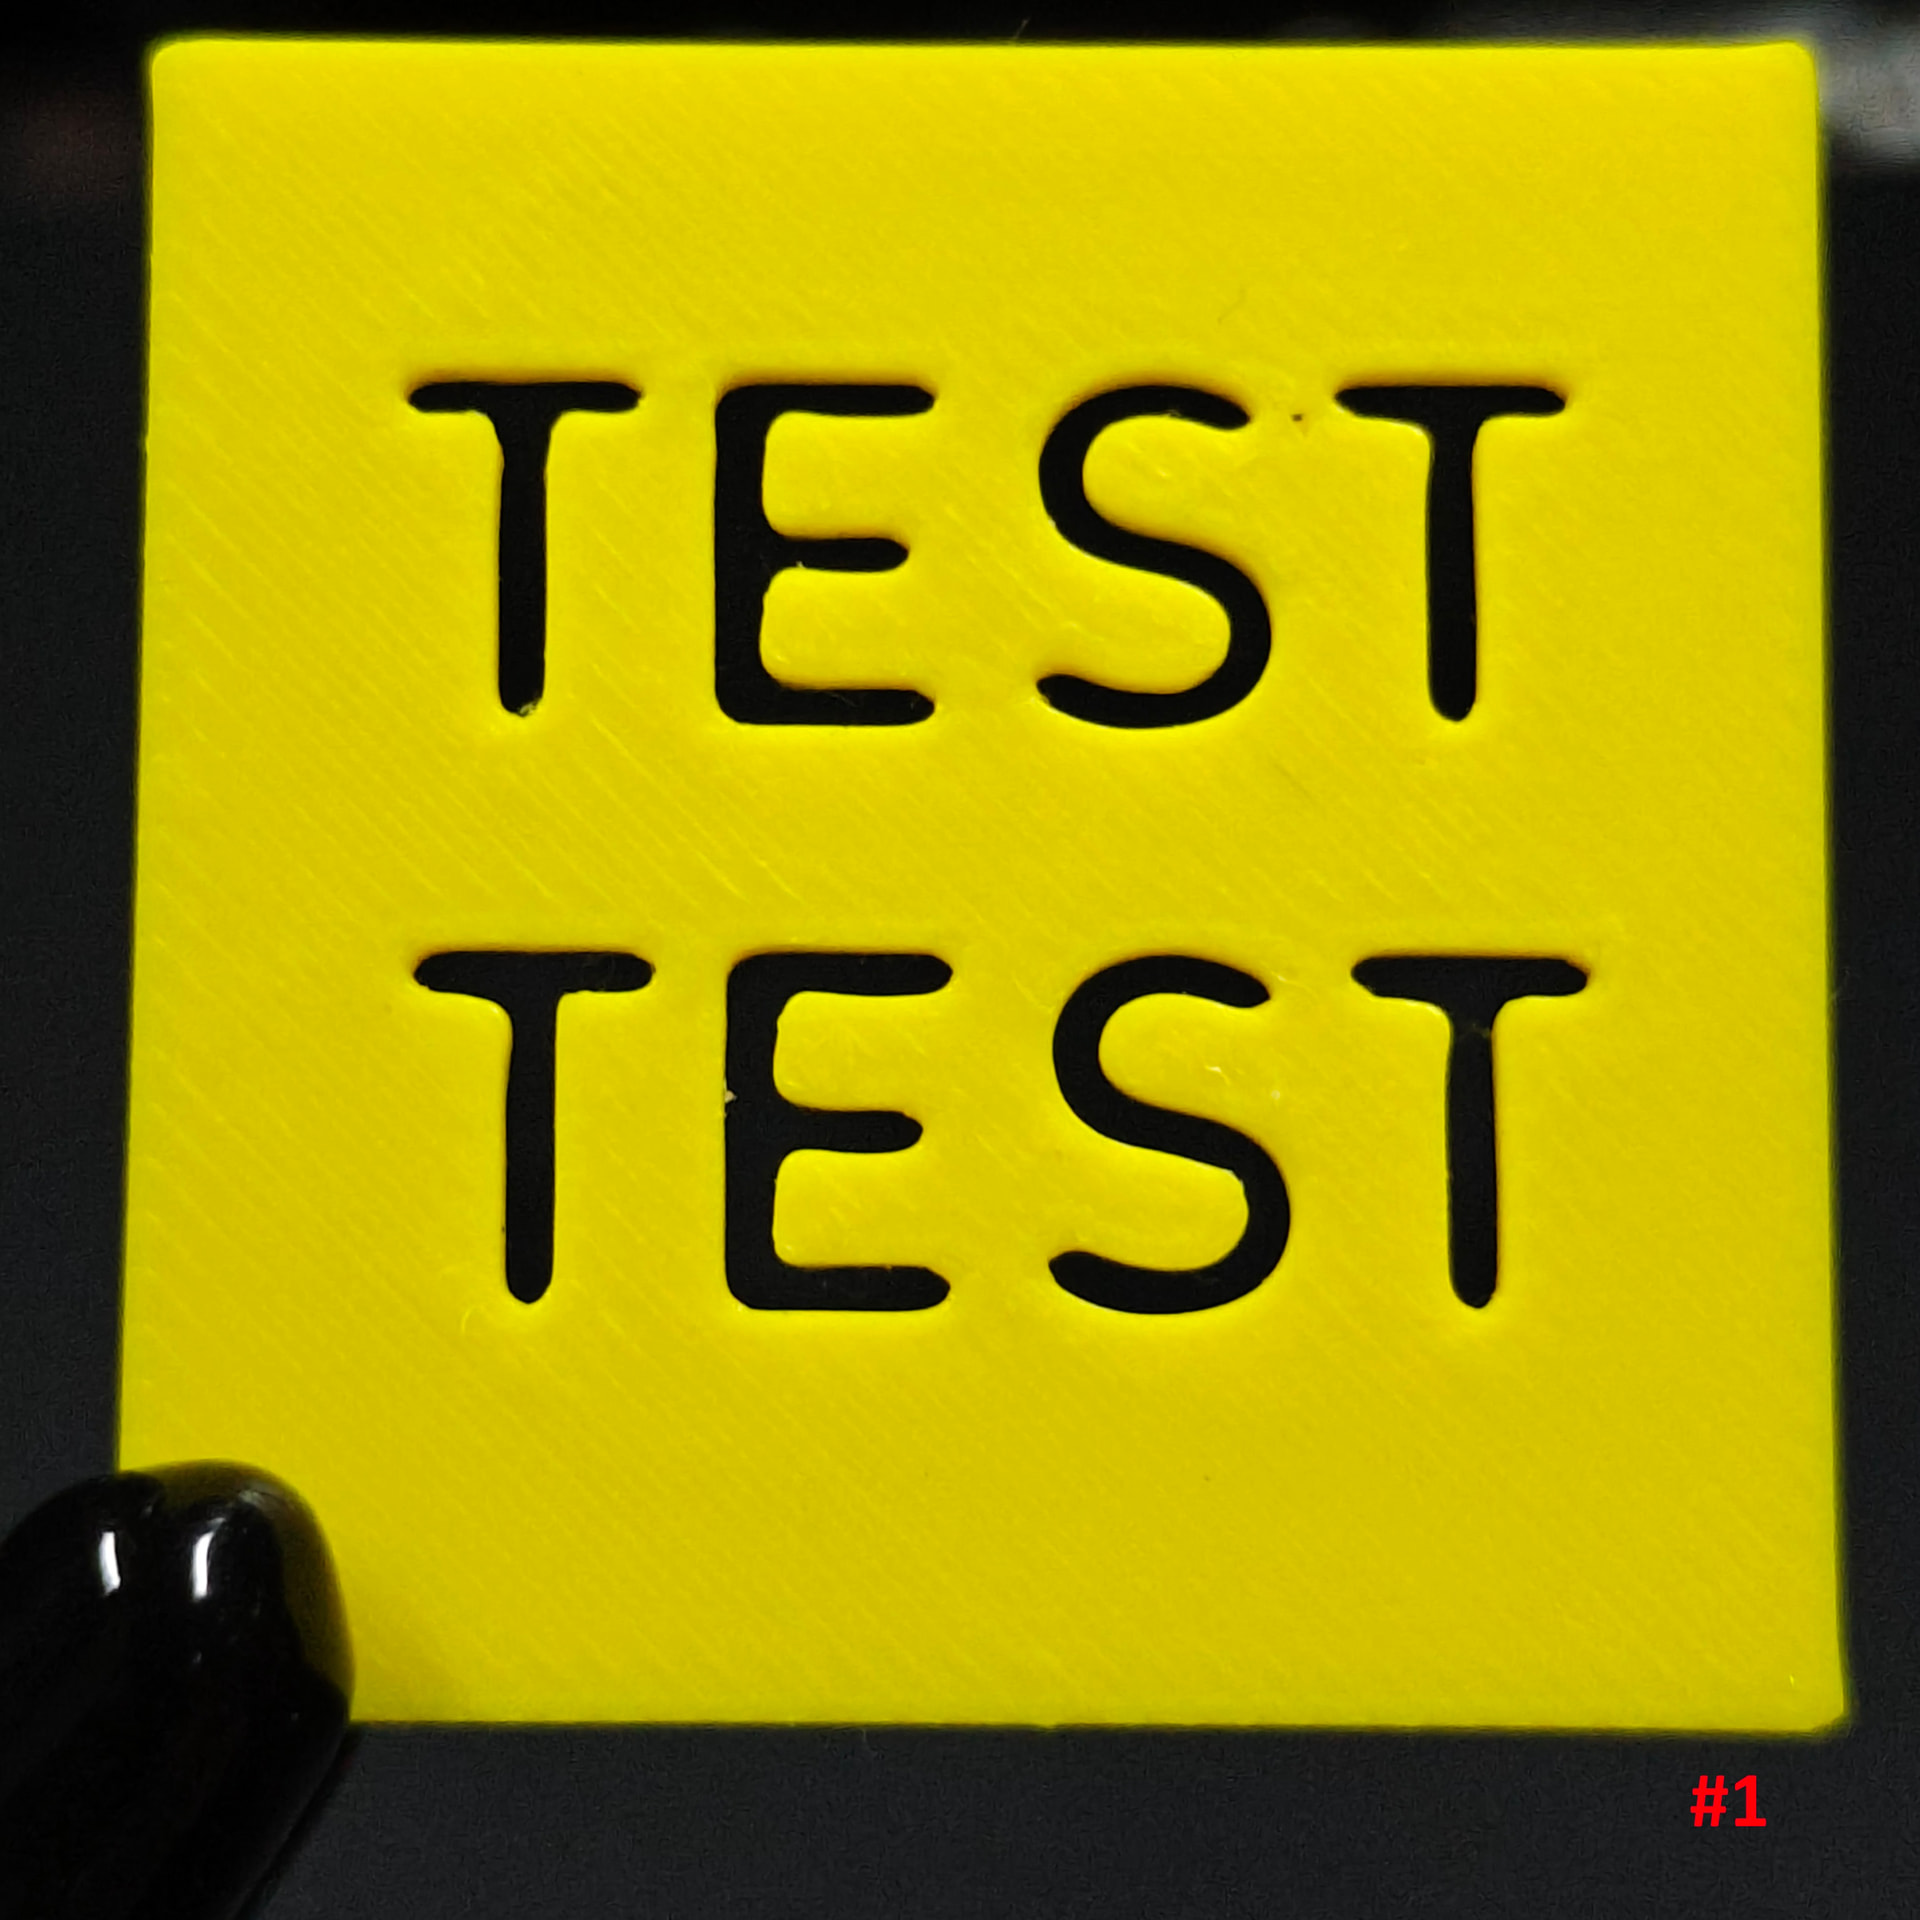
As another example, I printed the “TEST TEST” model on my A1 tonight using entirely default settings, and the result was near perfect. By comparison, the H2C example previously shown was printed using Bambu Support’s recommended changes (20 mm/s initial layer, 30 mm/s initial layer infill, plus an increased initial layer flow of 1.05) and it still produced a noticeably poorer result.

I’m not expecting a flawless first layer with no microscopic gaps. My concern is that the H2C consistently produces significantly poorer and less consistent results than another Bambu printer using the same material and print data, even after three months of troubleshooting and following Bambu Support’s recommendations.

@RogueOhio Hi, can you share or PM me the 3mf of TEST/TEST model? Edit: so I can print on my H2C and share a picture here.

TEST TEST.3mf (38.3 KB)

Here the file I popped together in studio. Take note i have increased the initial layer flow to 1.05. Might be worth testing on the default 1 and increase from there if needed on your machine.

This is by no means a defining print it is simply one i replicated to the original gcode file bambu support sent.

If I were to pop together ANY geometric shape in Bambu Studio with holes or multi colour shapes on the initial layer I will see flaws. I cant remember now if this was the test Bambu asked me to try slow speeds but there was one I did and this did nothing to help.

I can pretty much pop any file to print and received sub par first layer results. The most concerning things are:

  1. Inconsistent results across any print files so I’m always having to to test prints just to try and dial things in still with imperfect results.
  2. When you incorporate multi colour over both Left and Right nozzle

Great, thank you. I started a 35 hour print 60min ago so unless it fails early I’ll revert in a couple days with pictures.

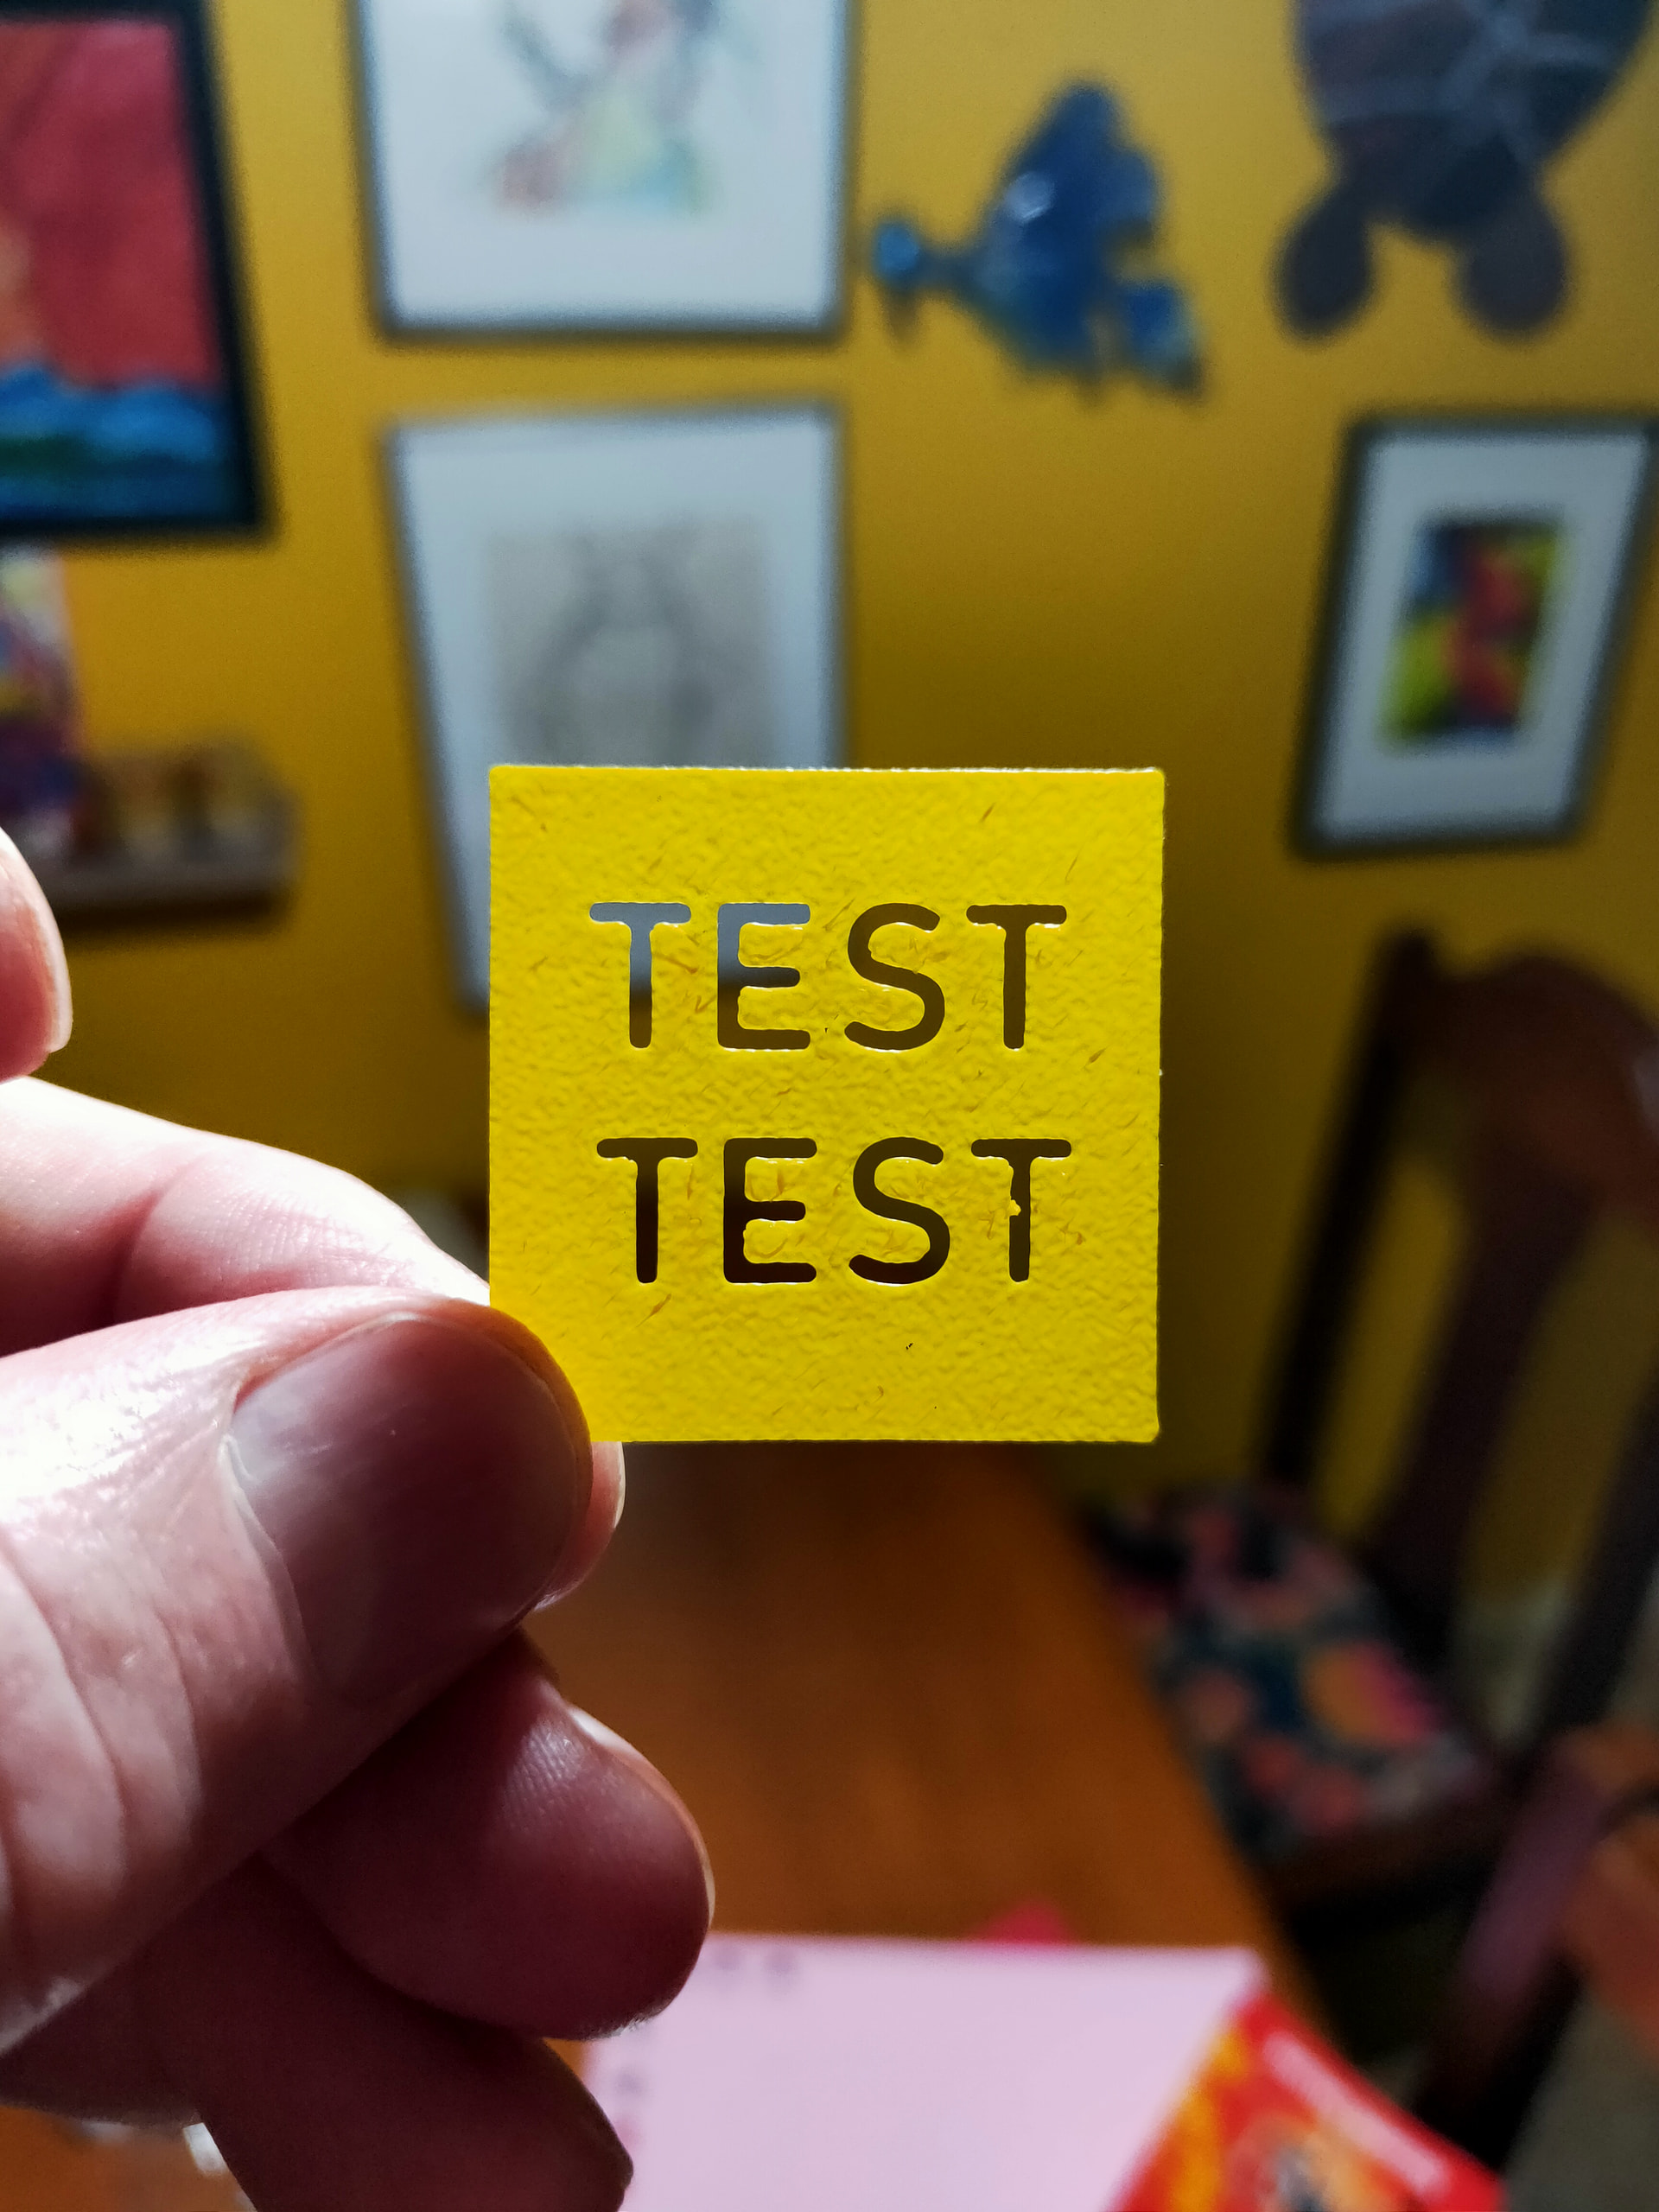
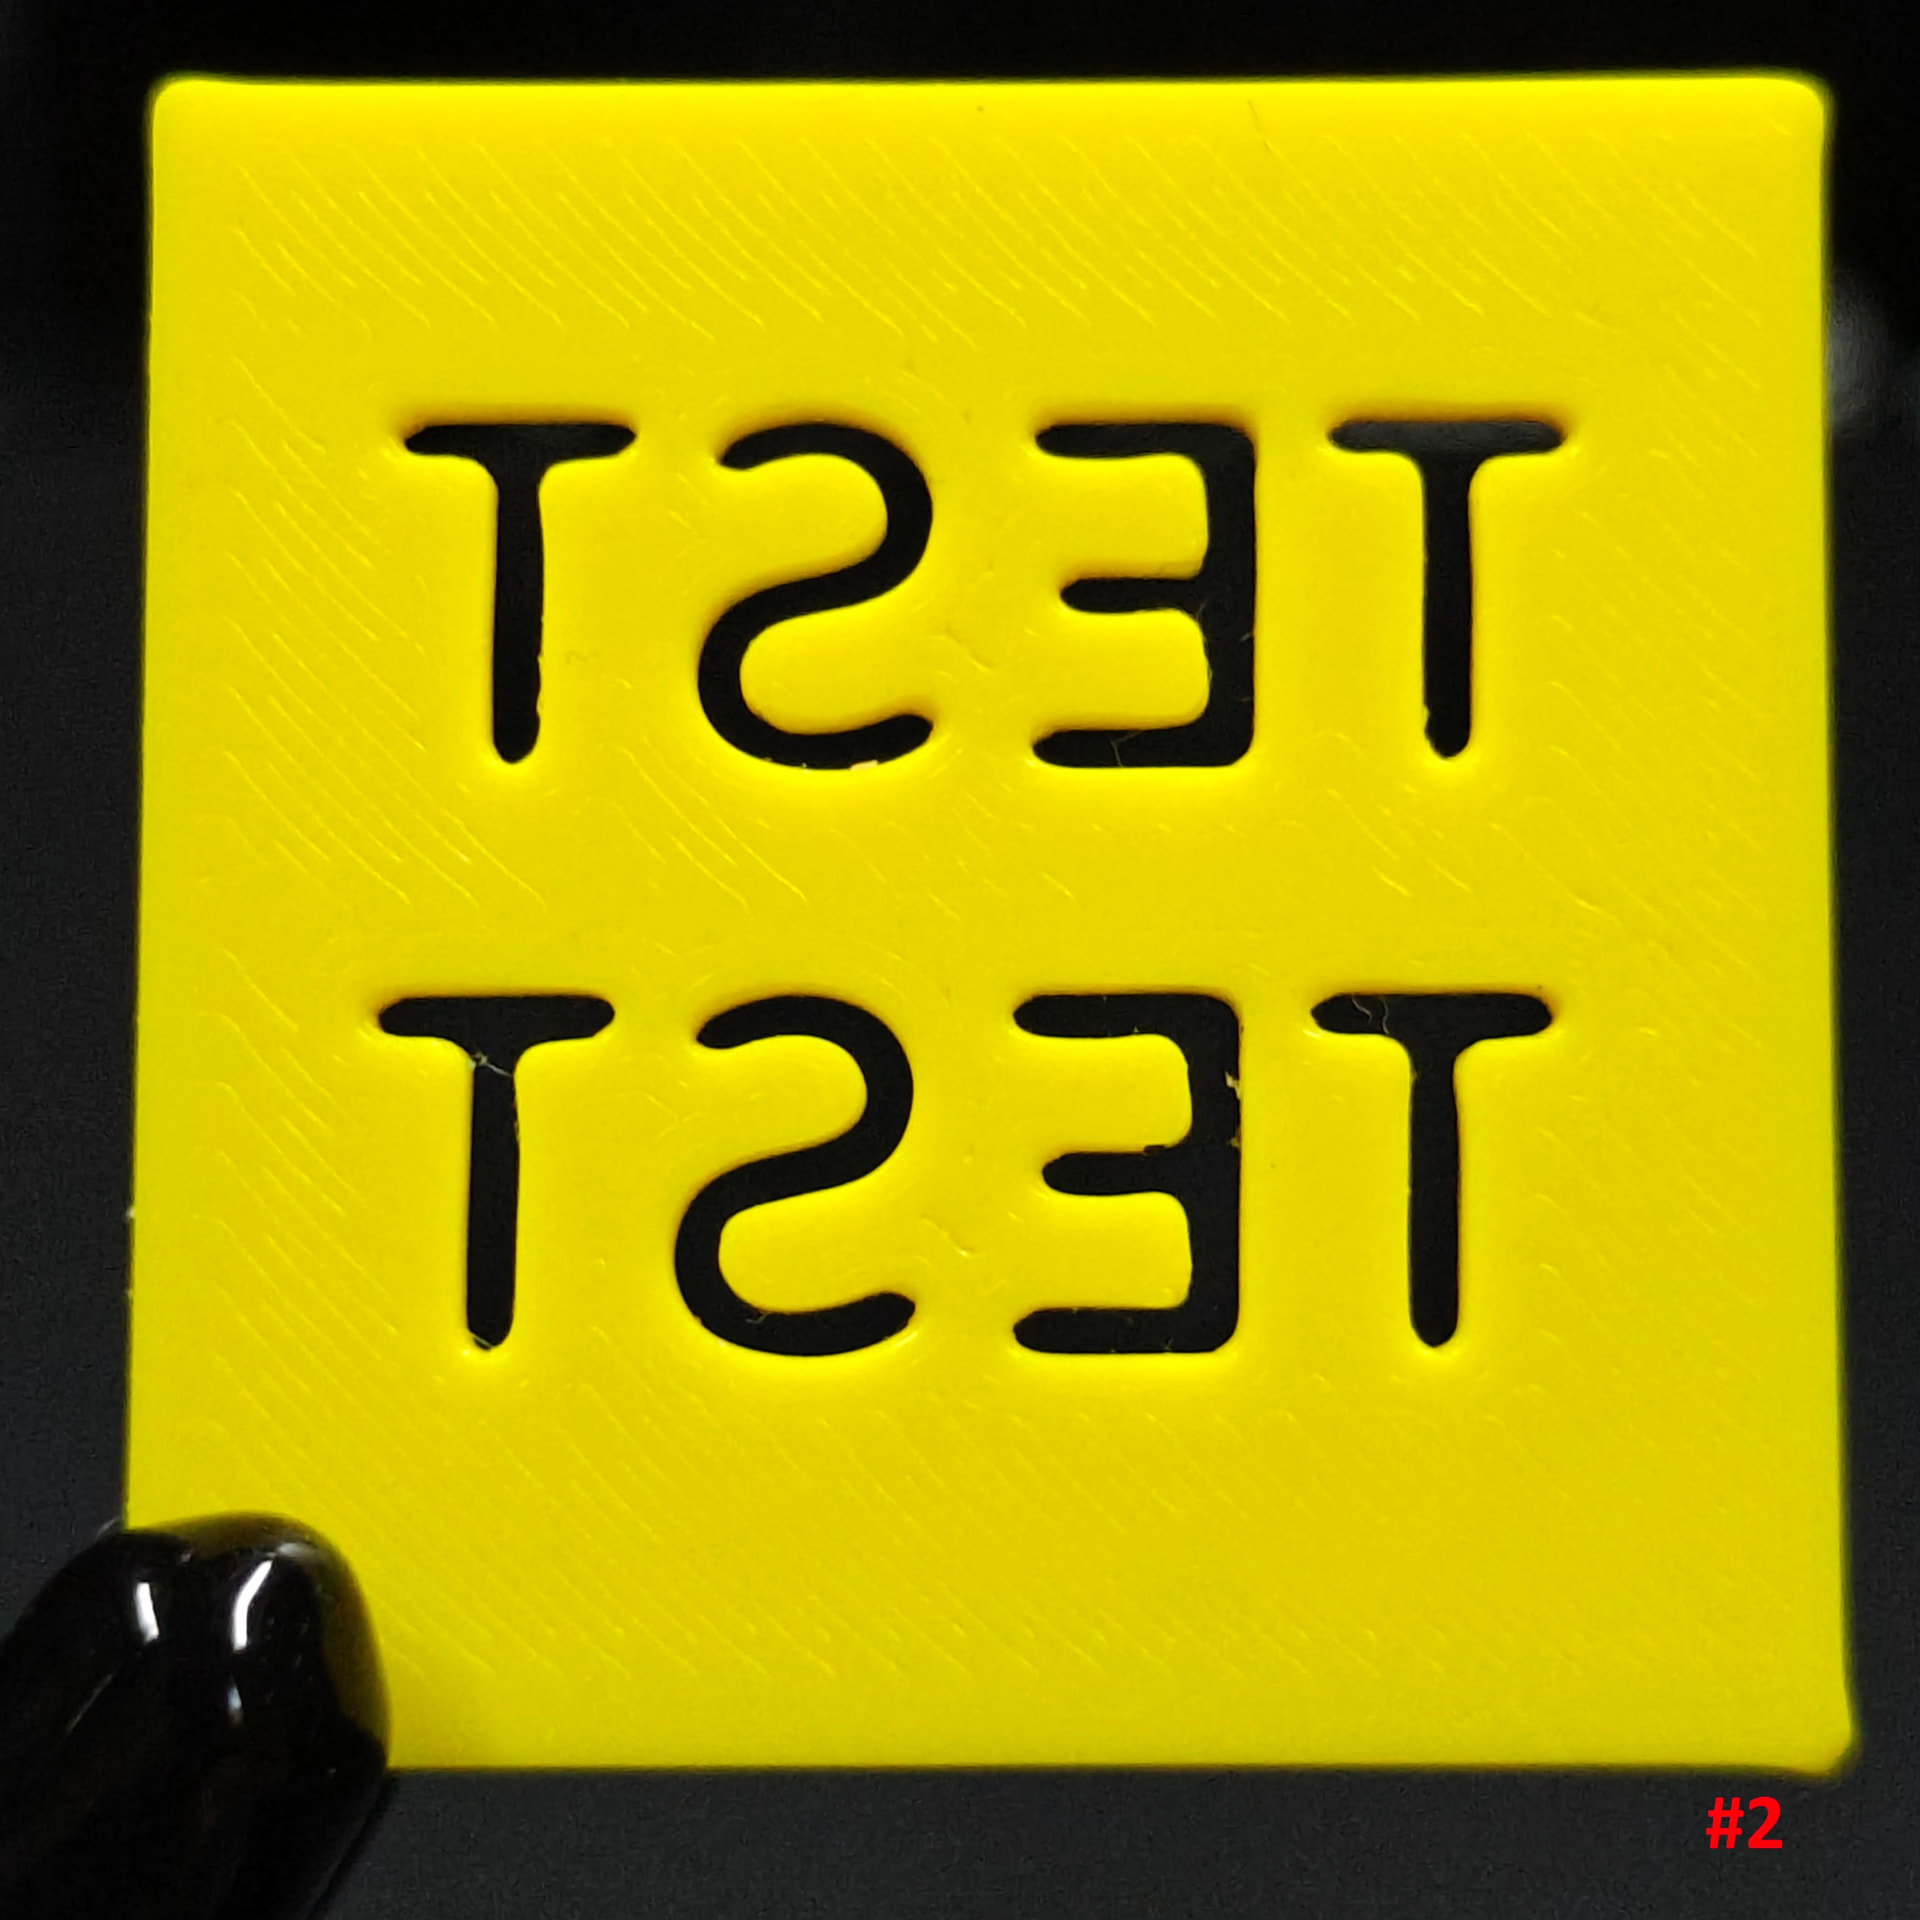
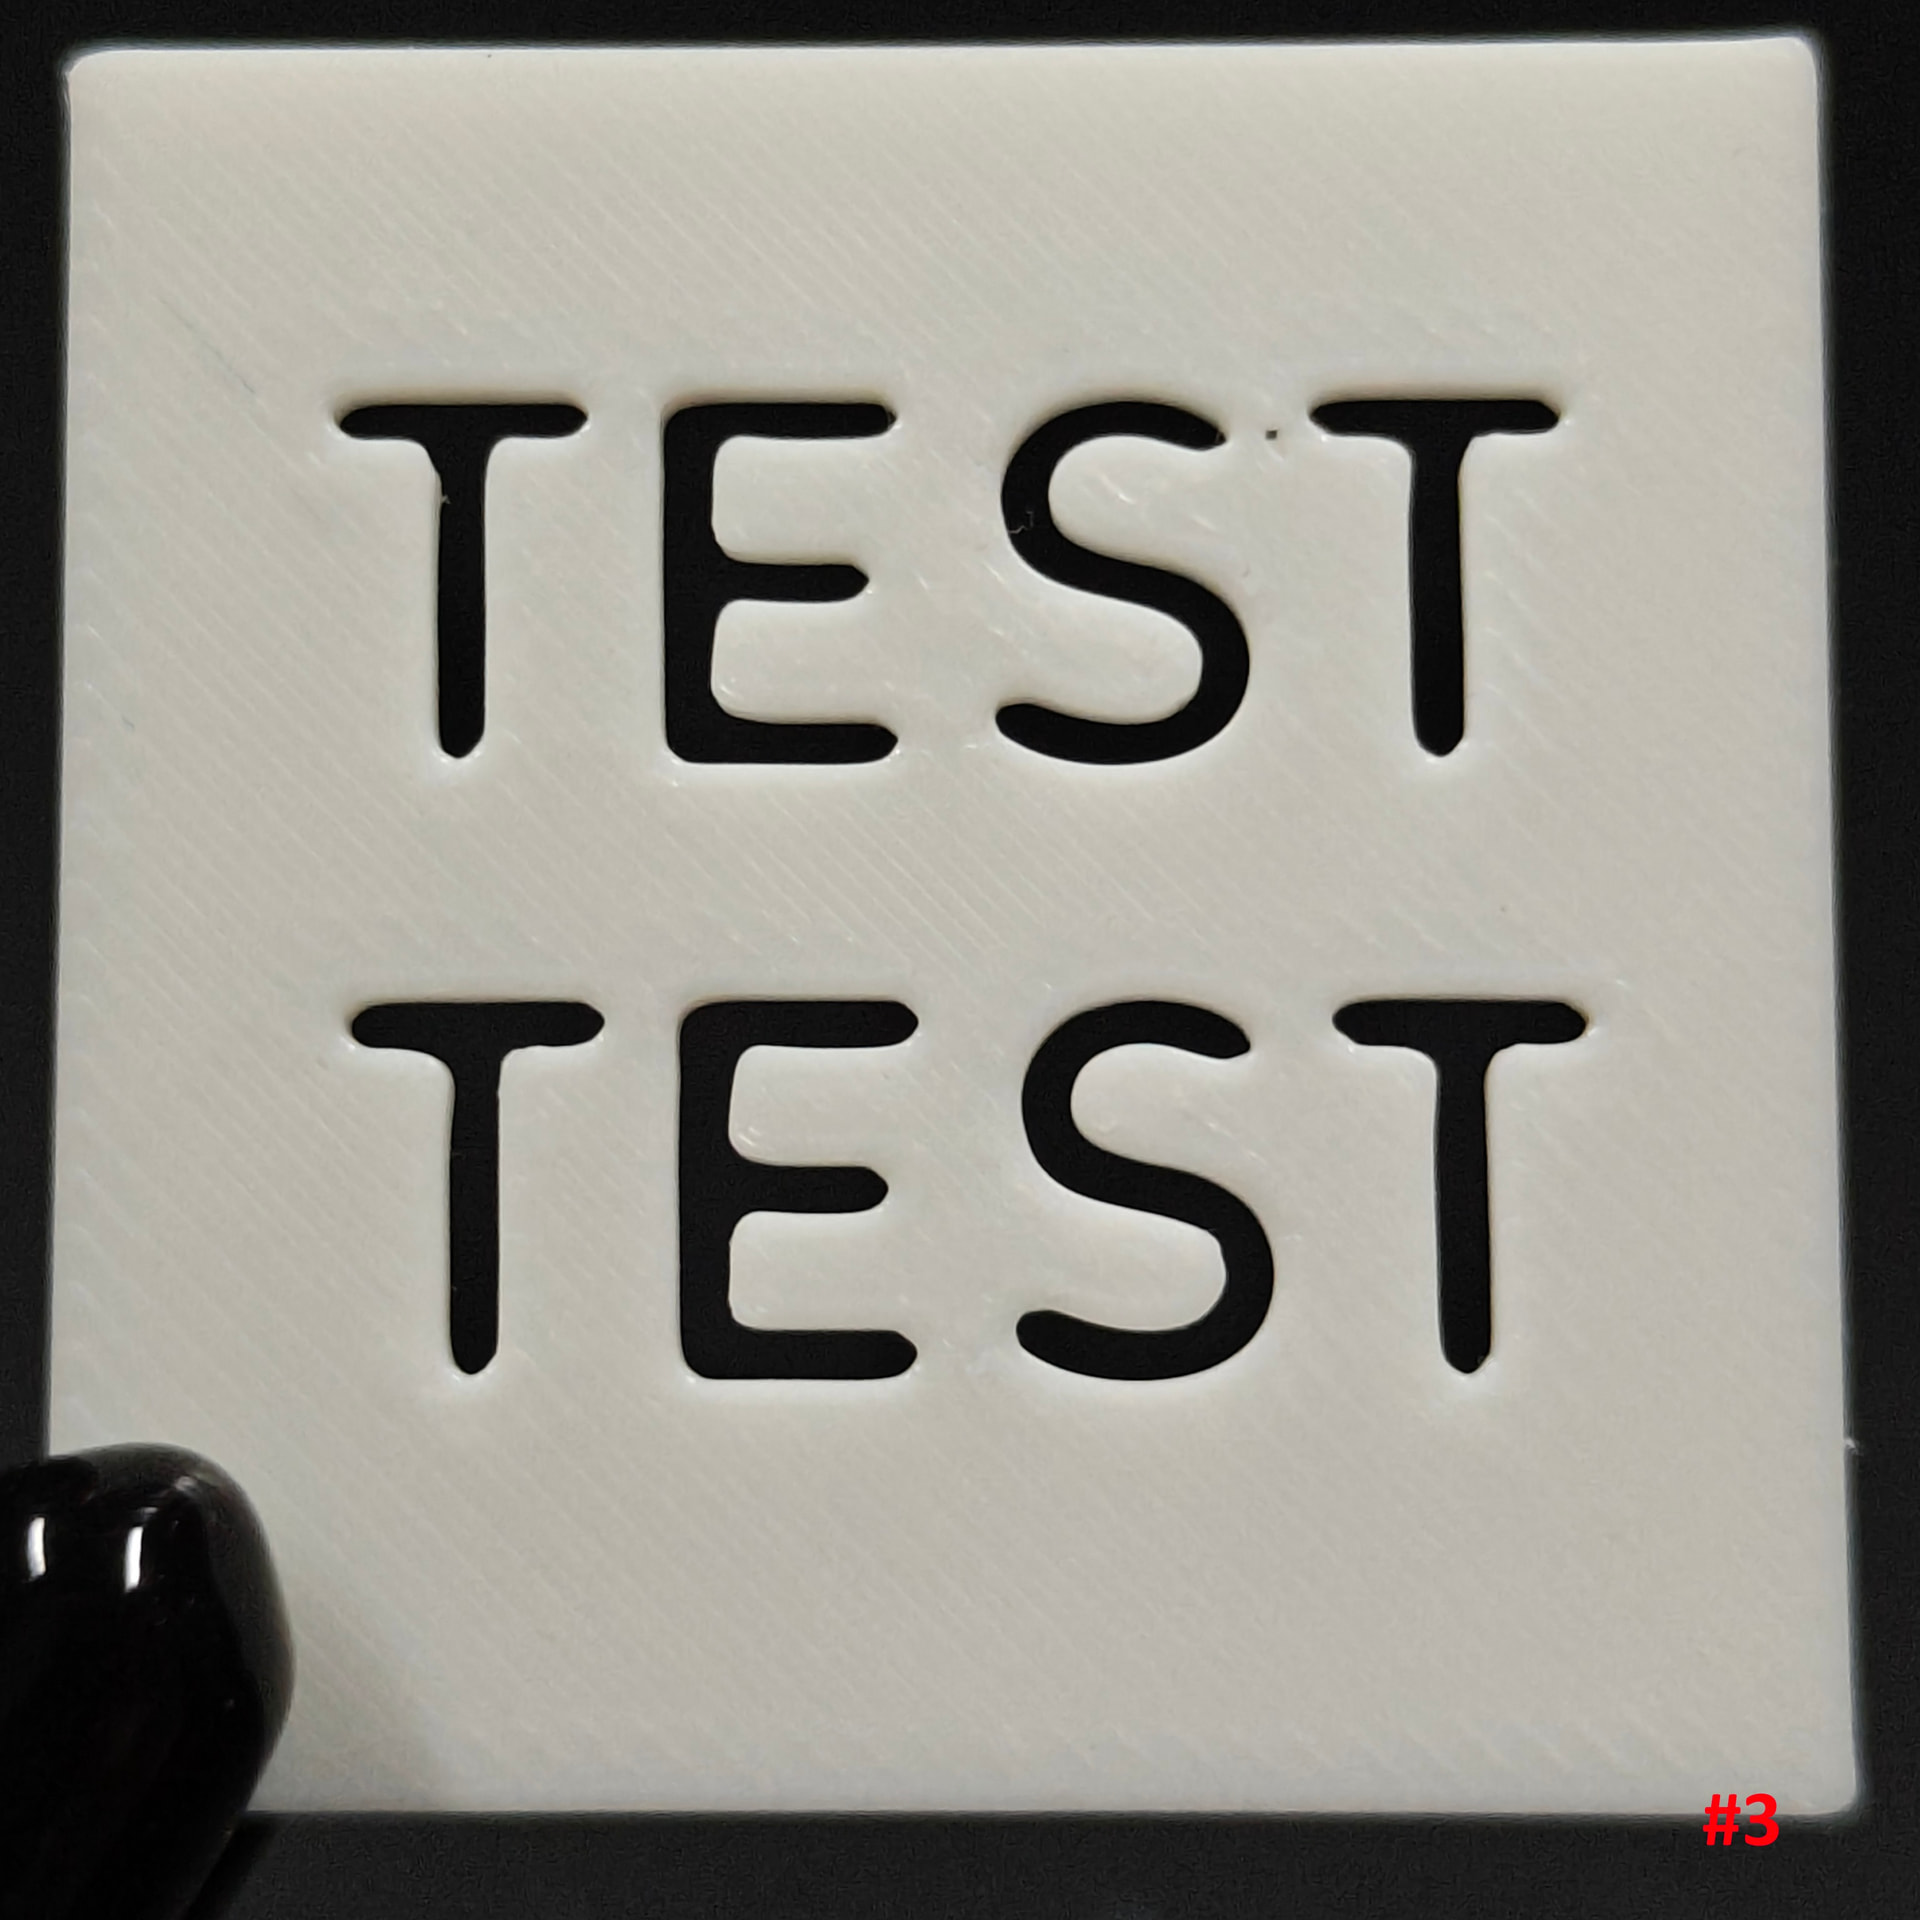
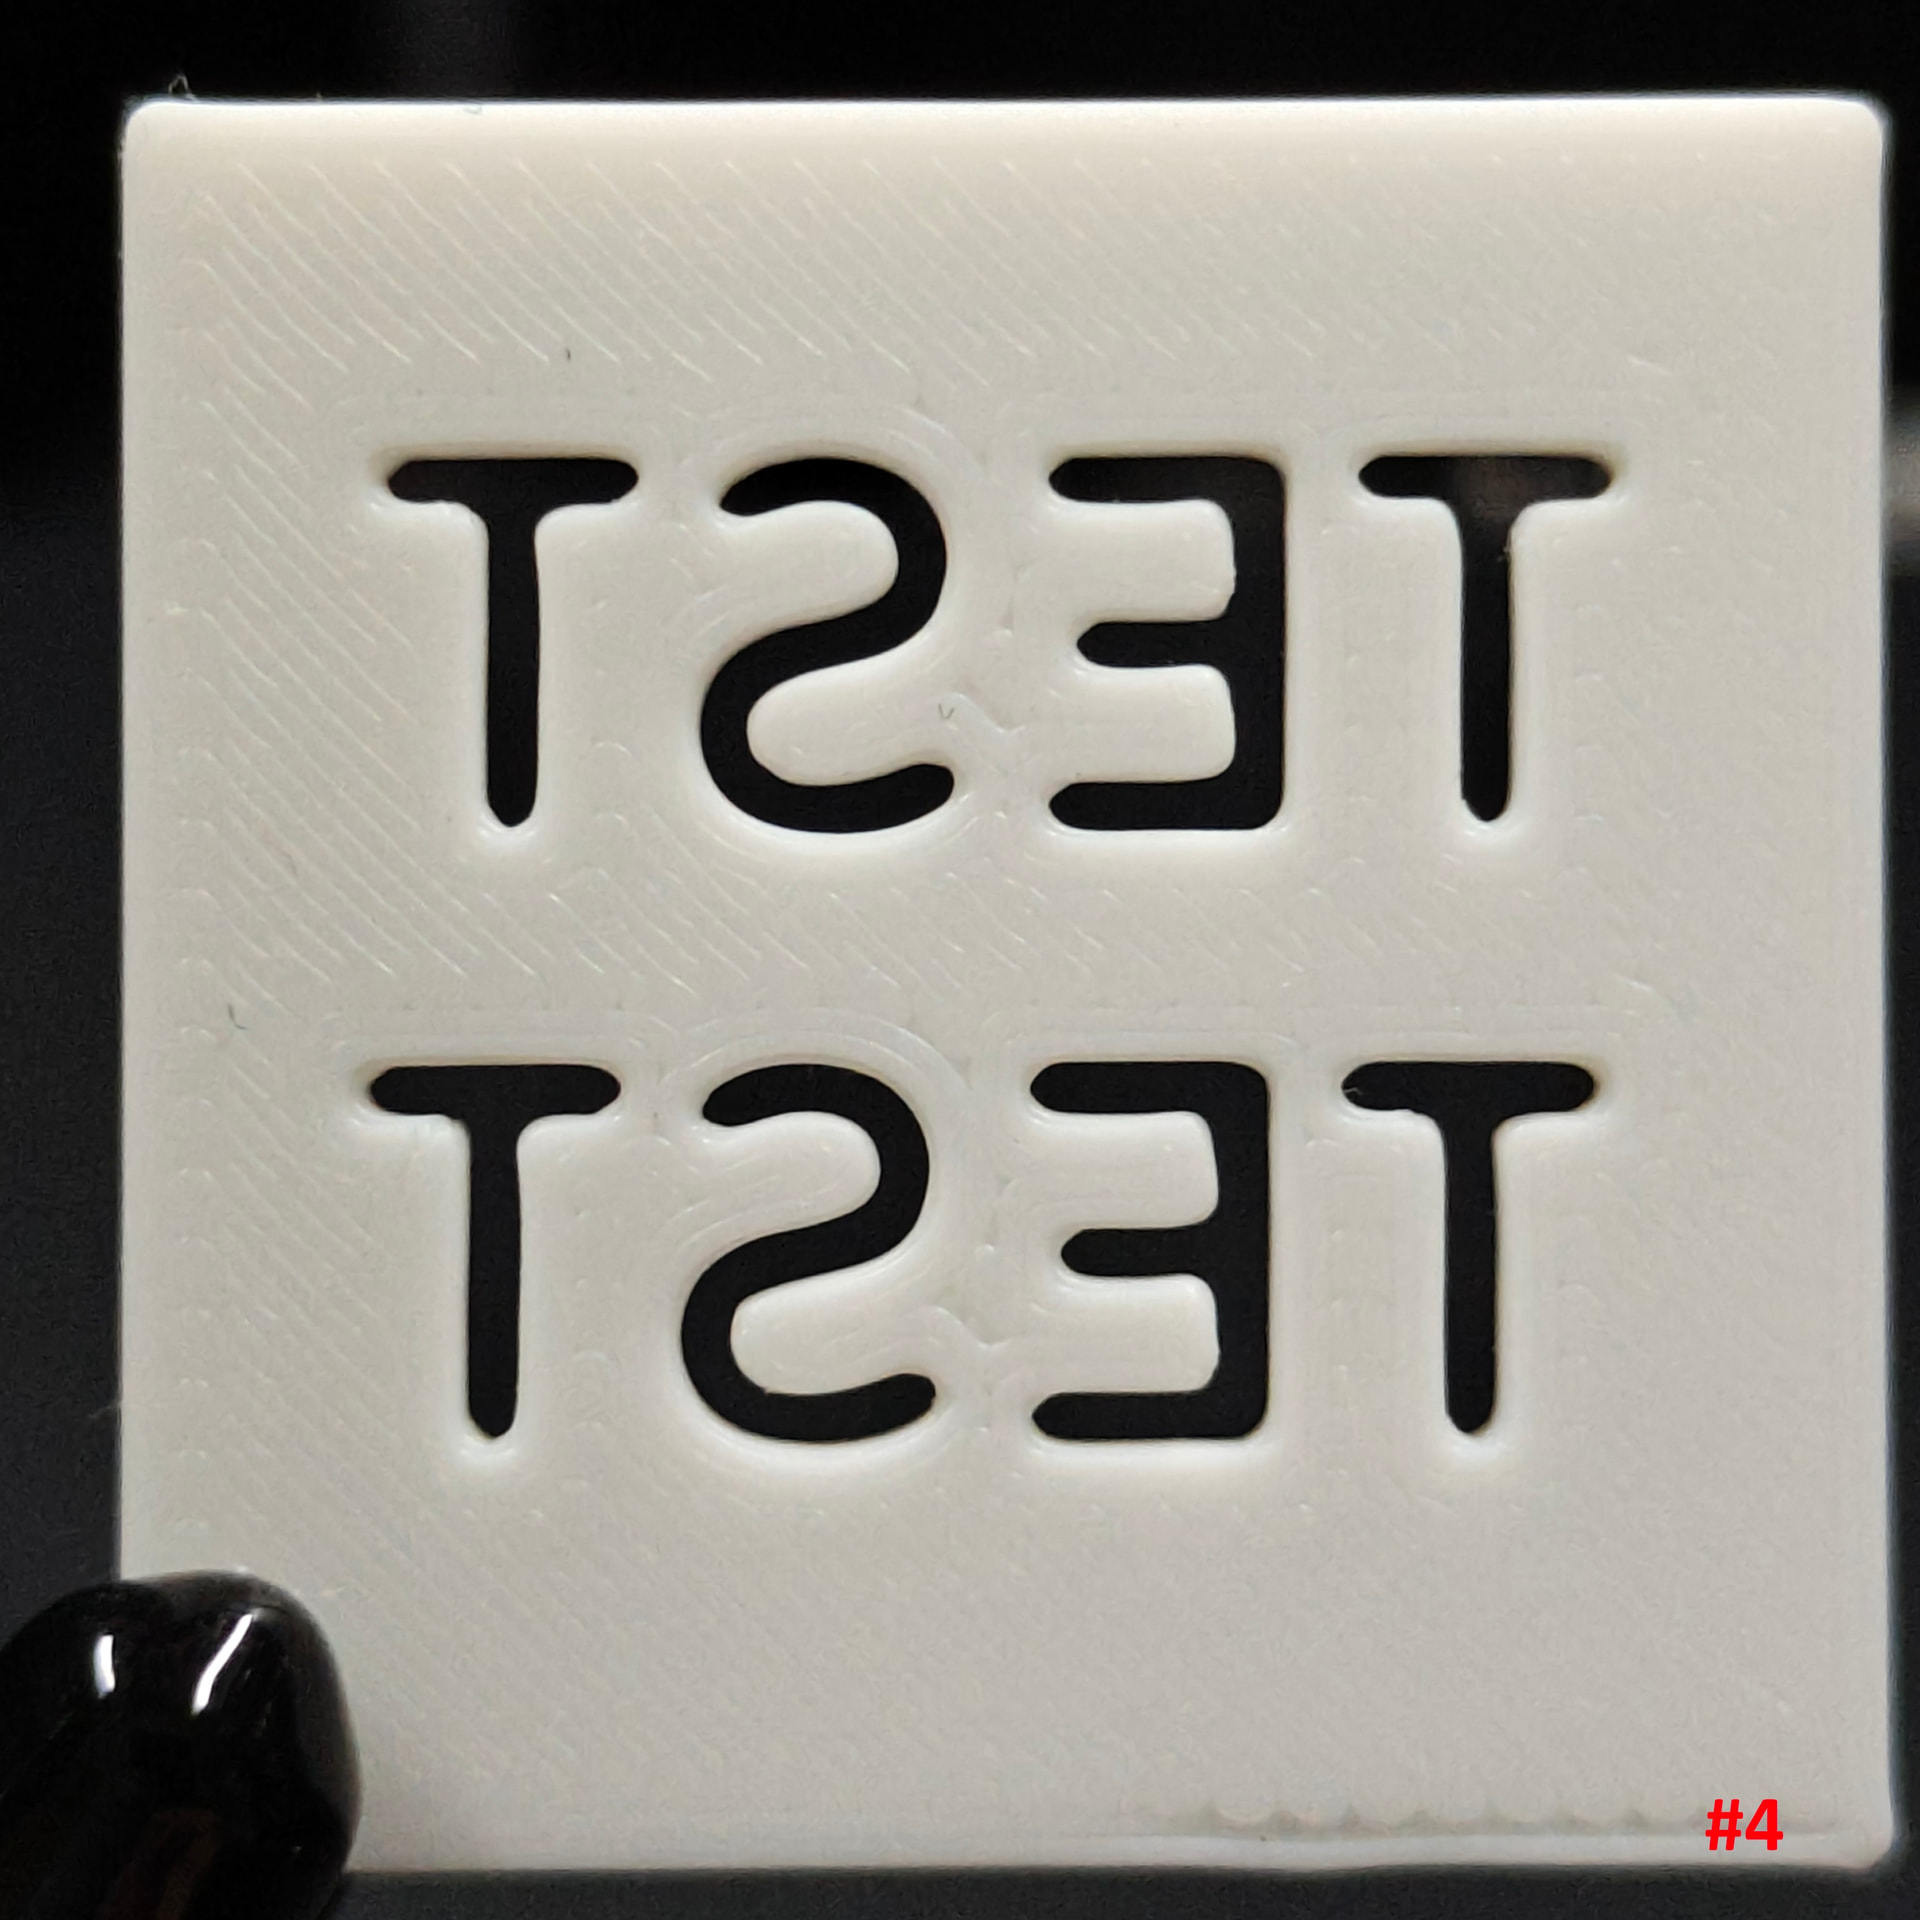
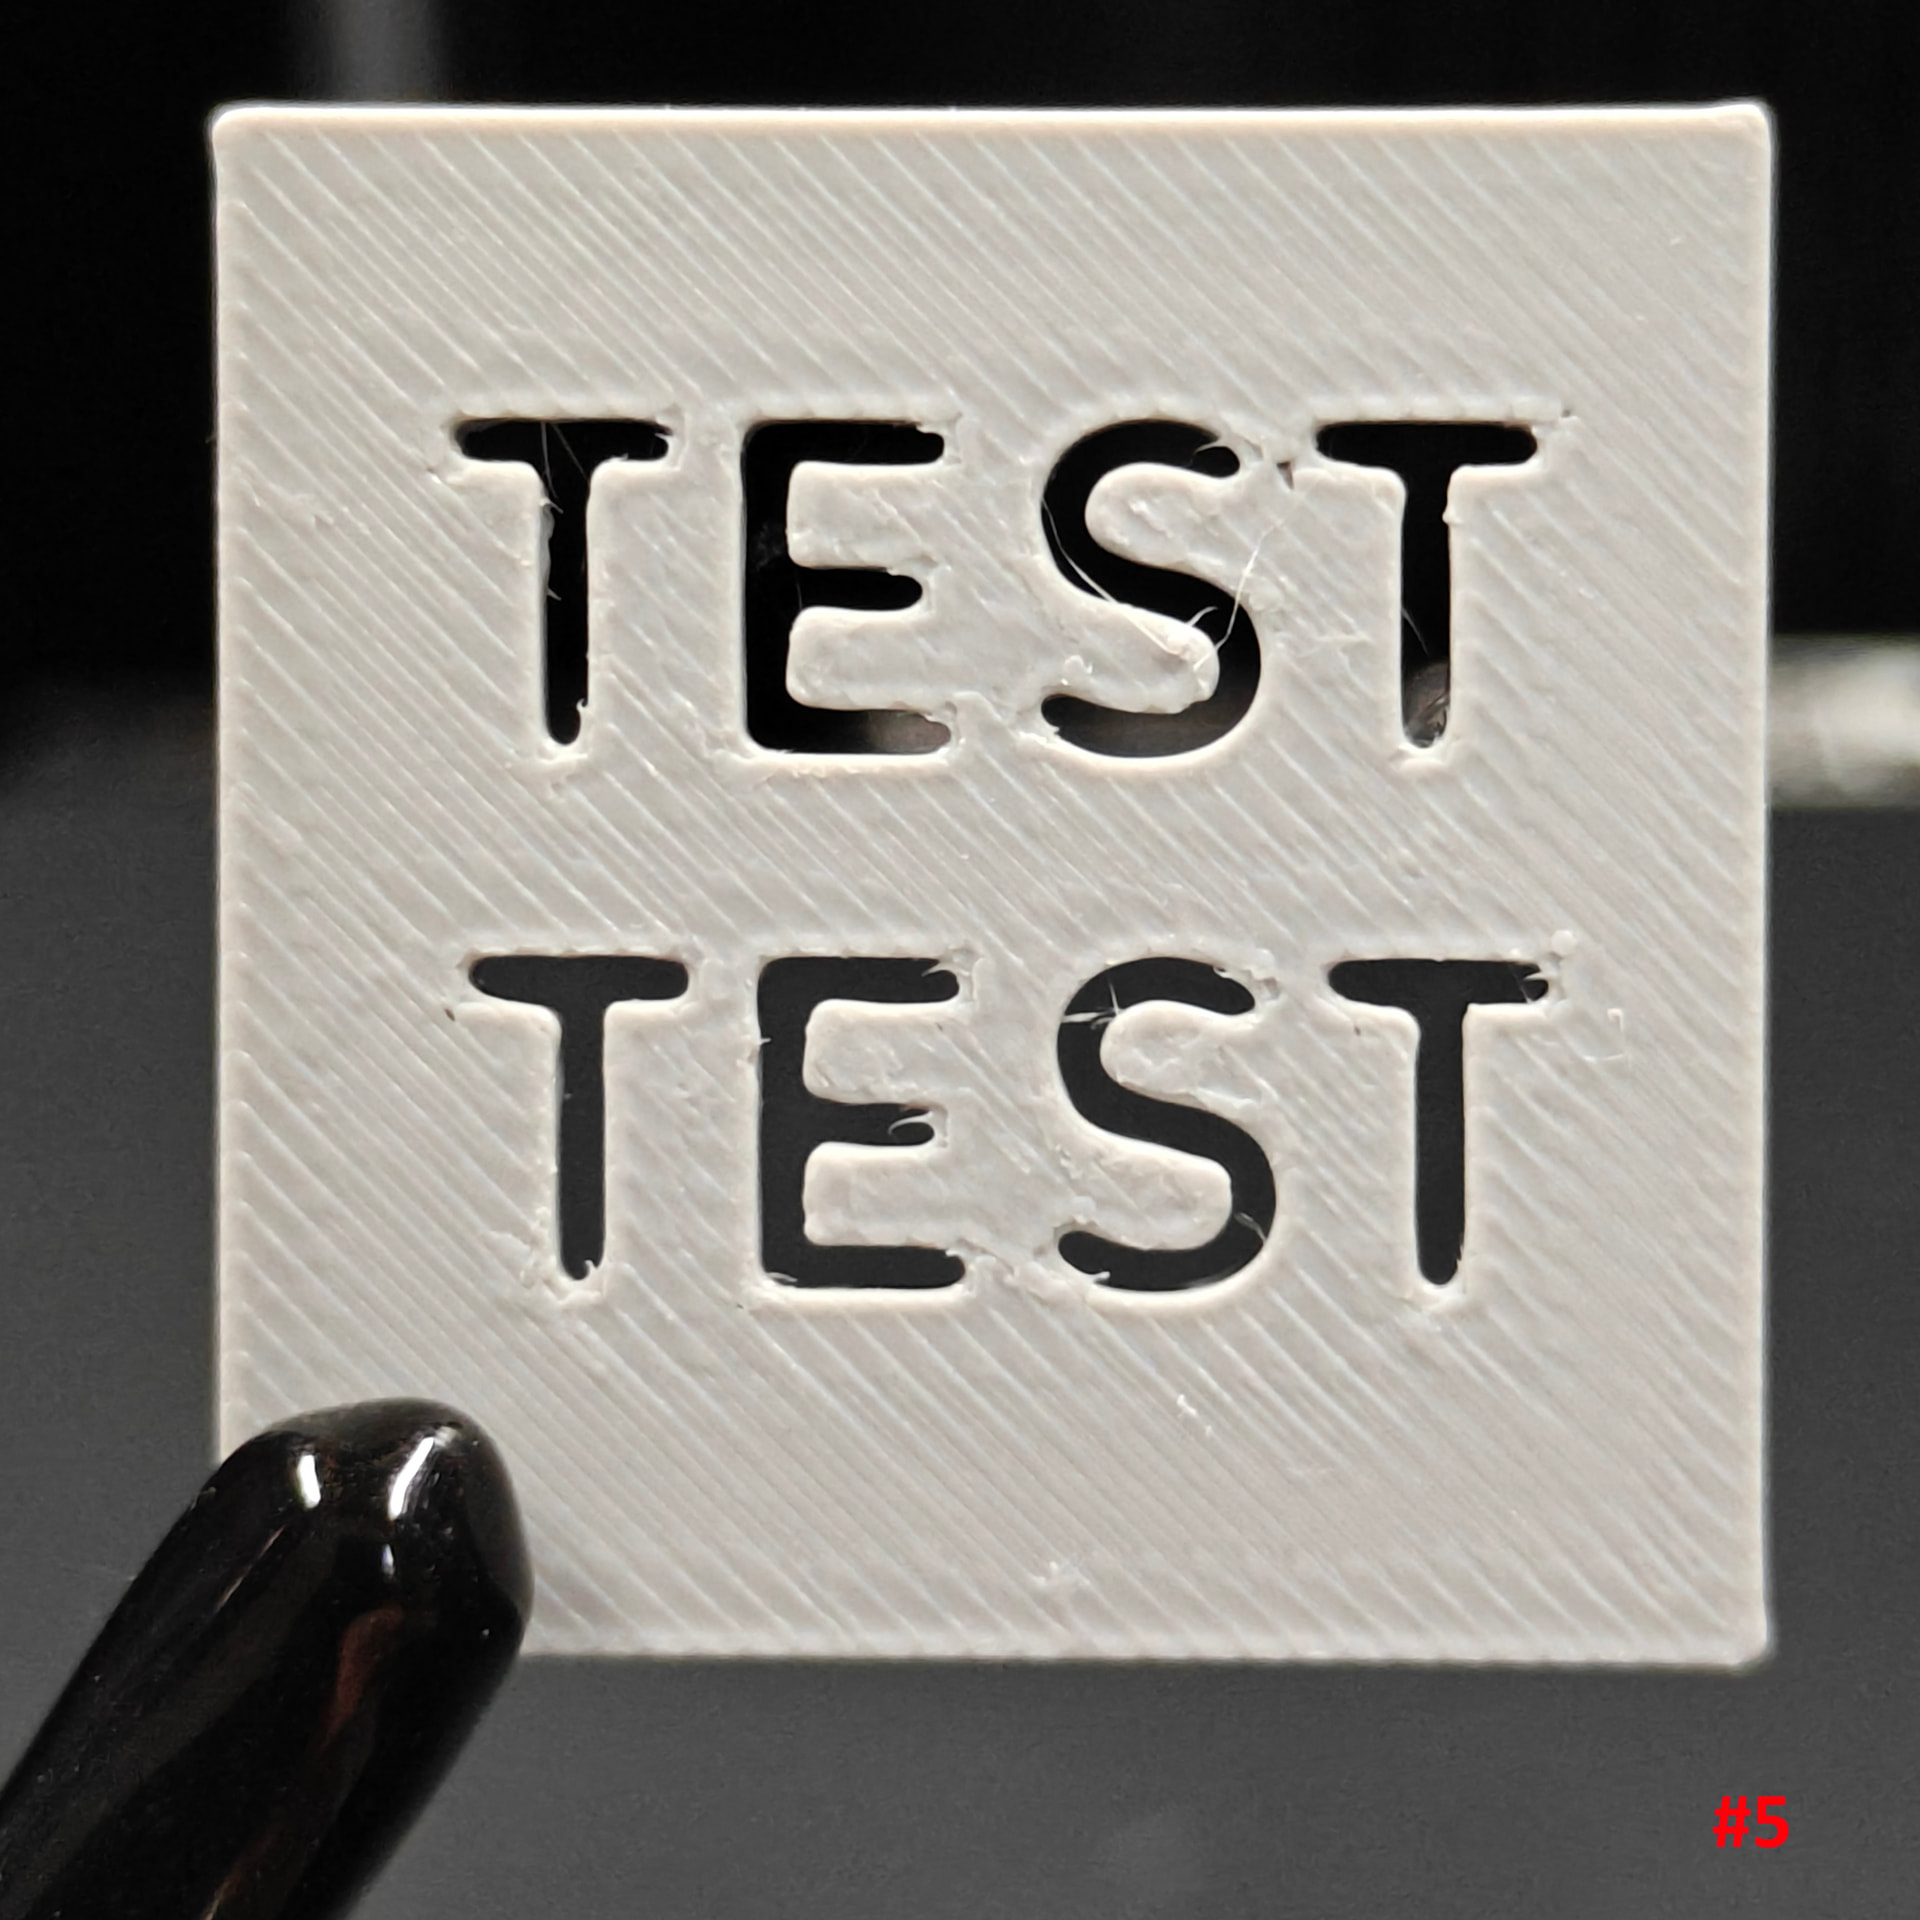
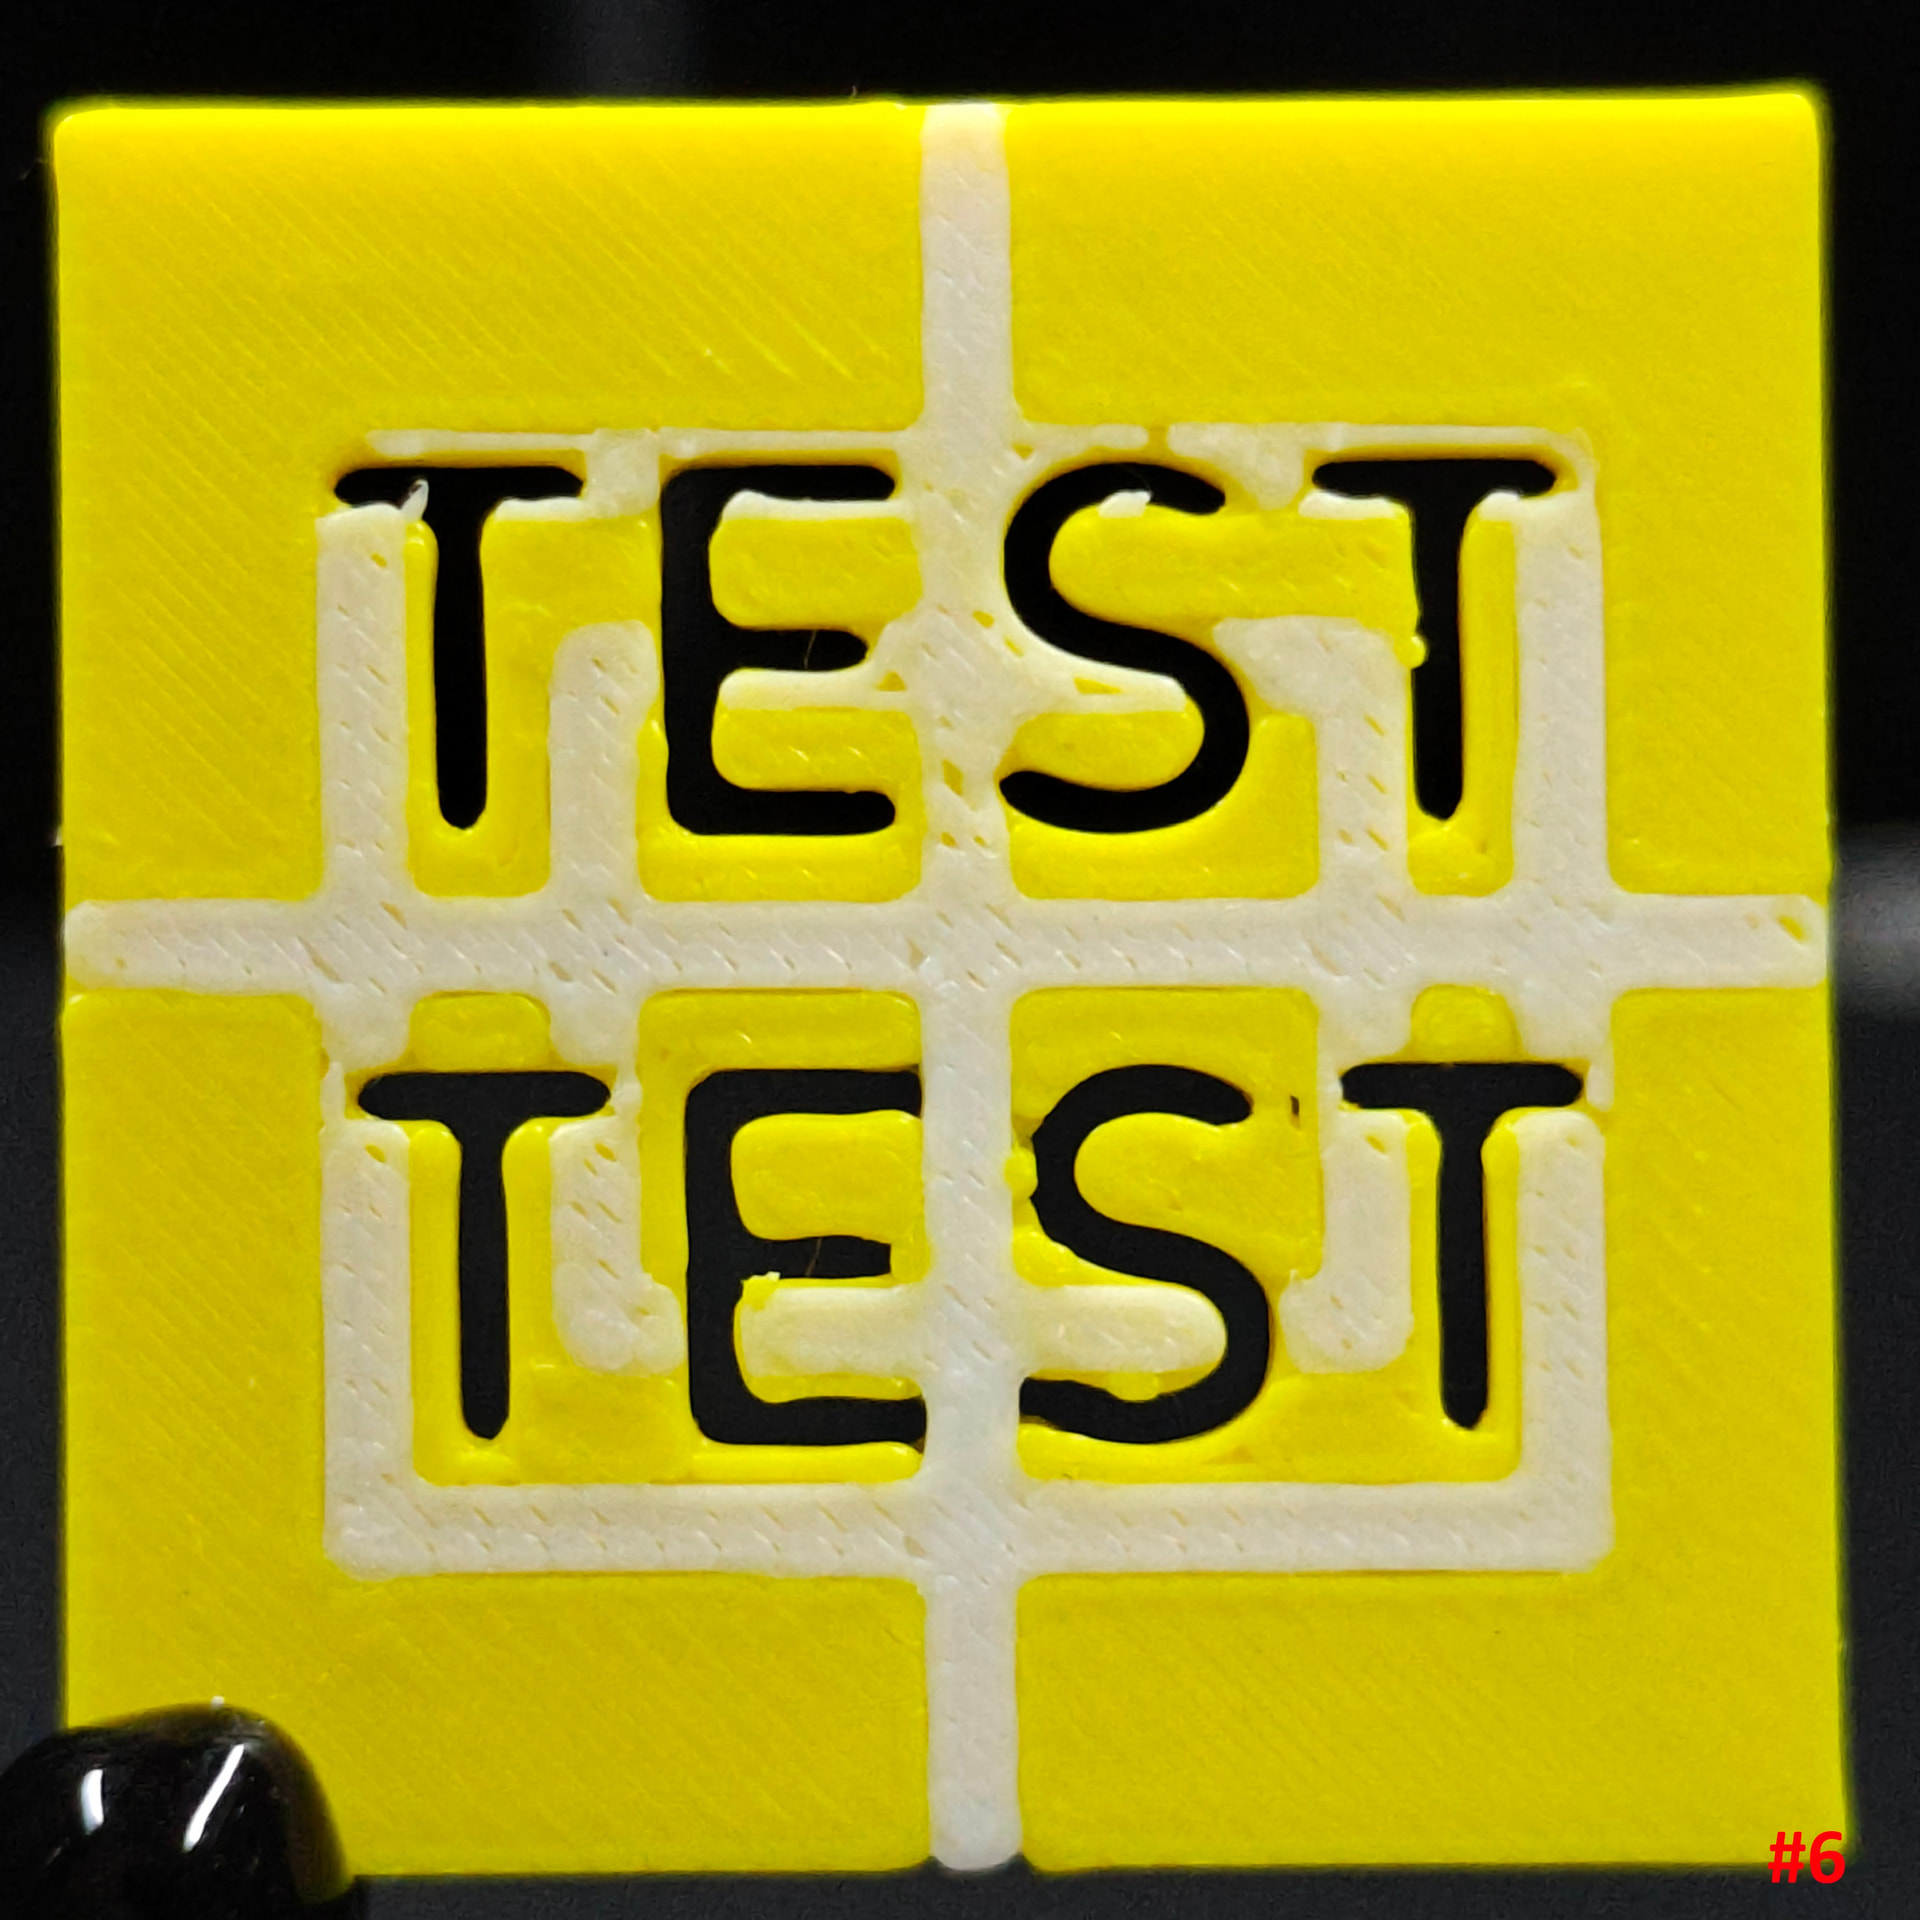
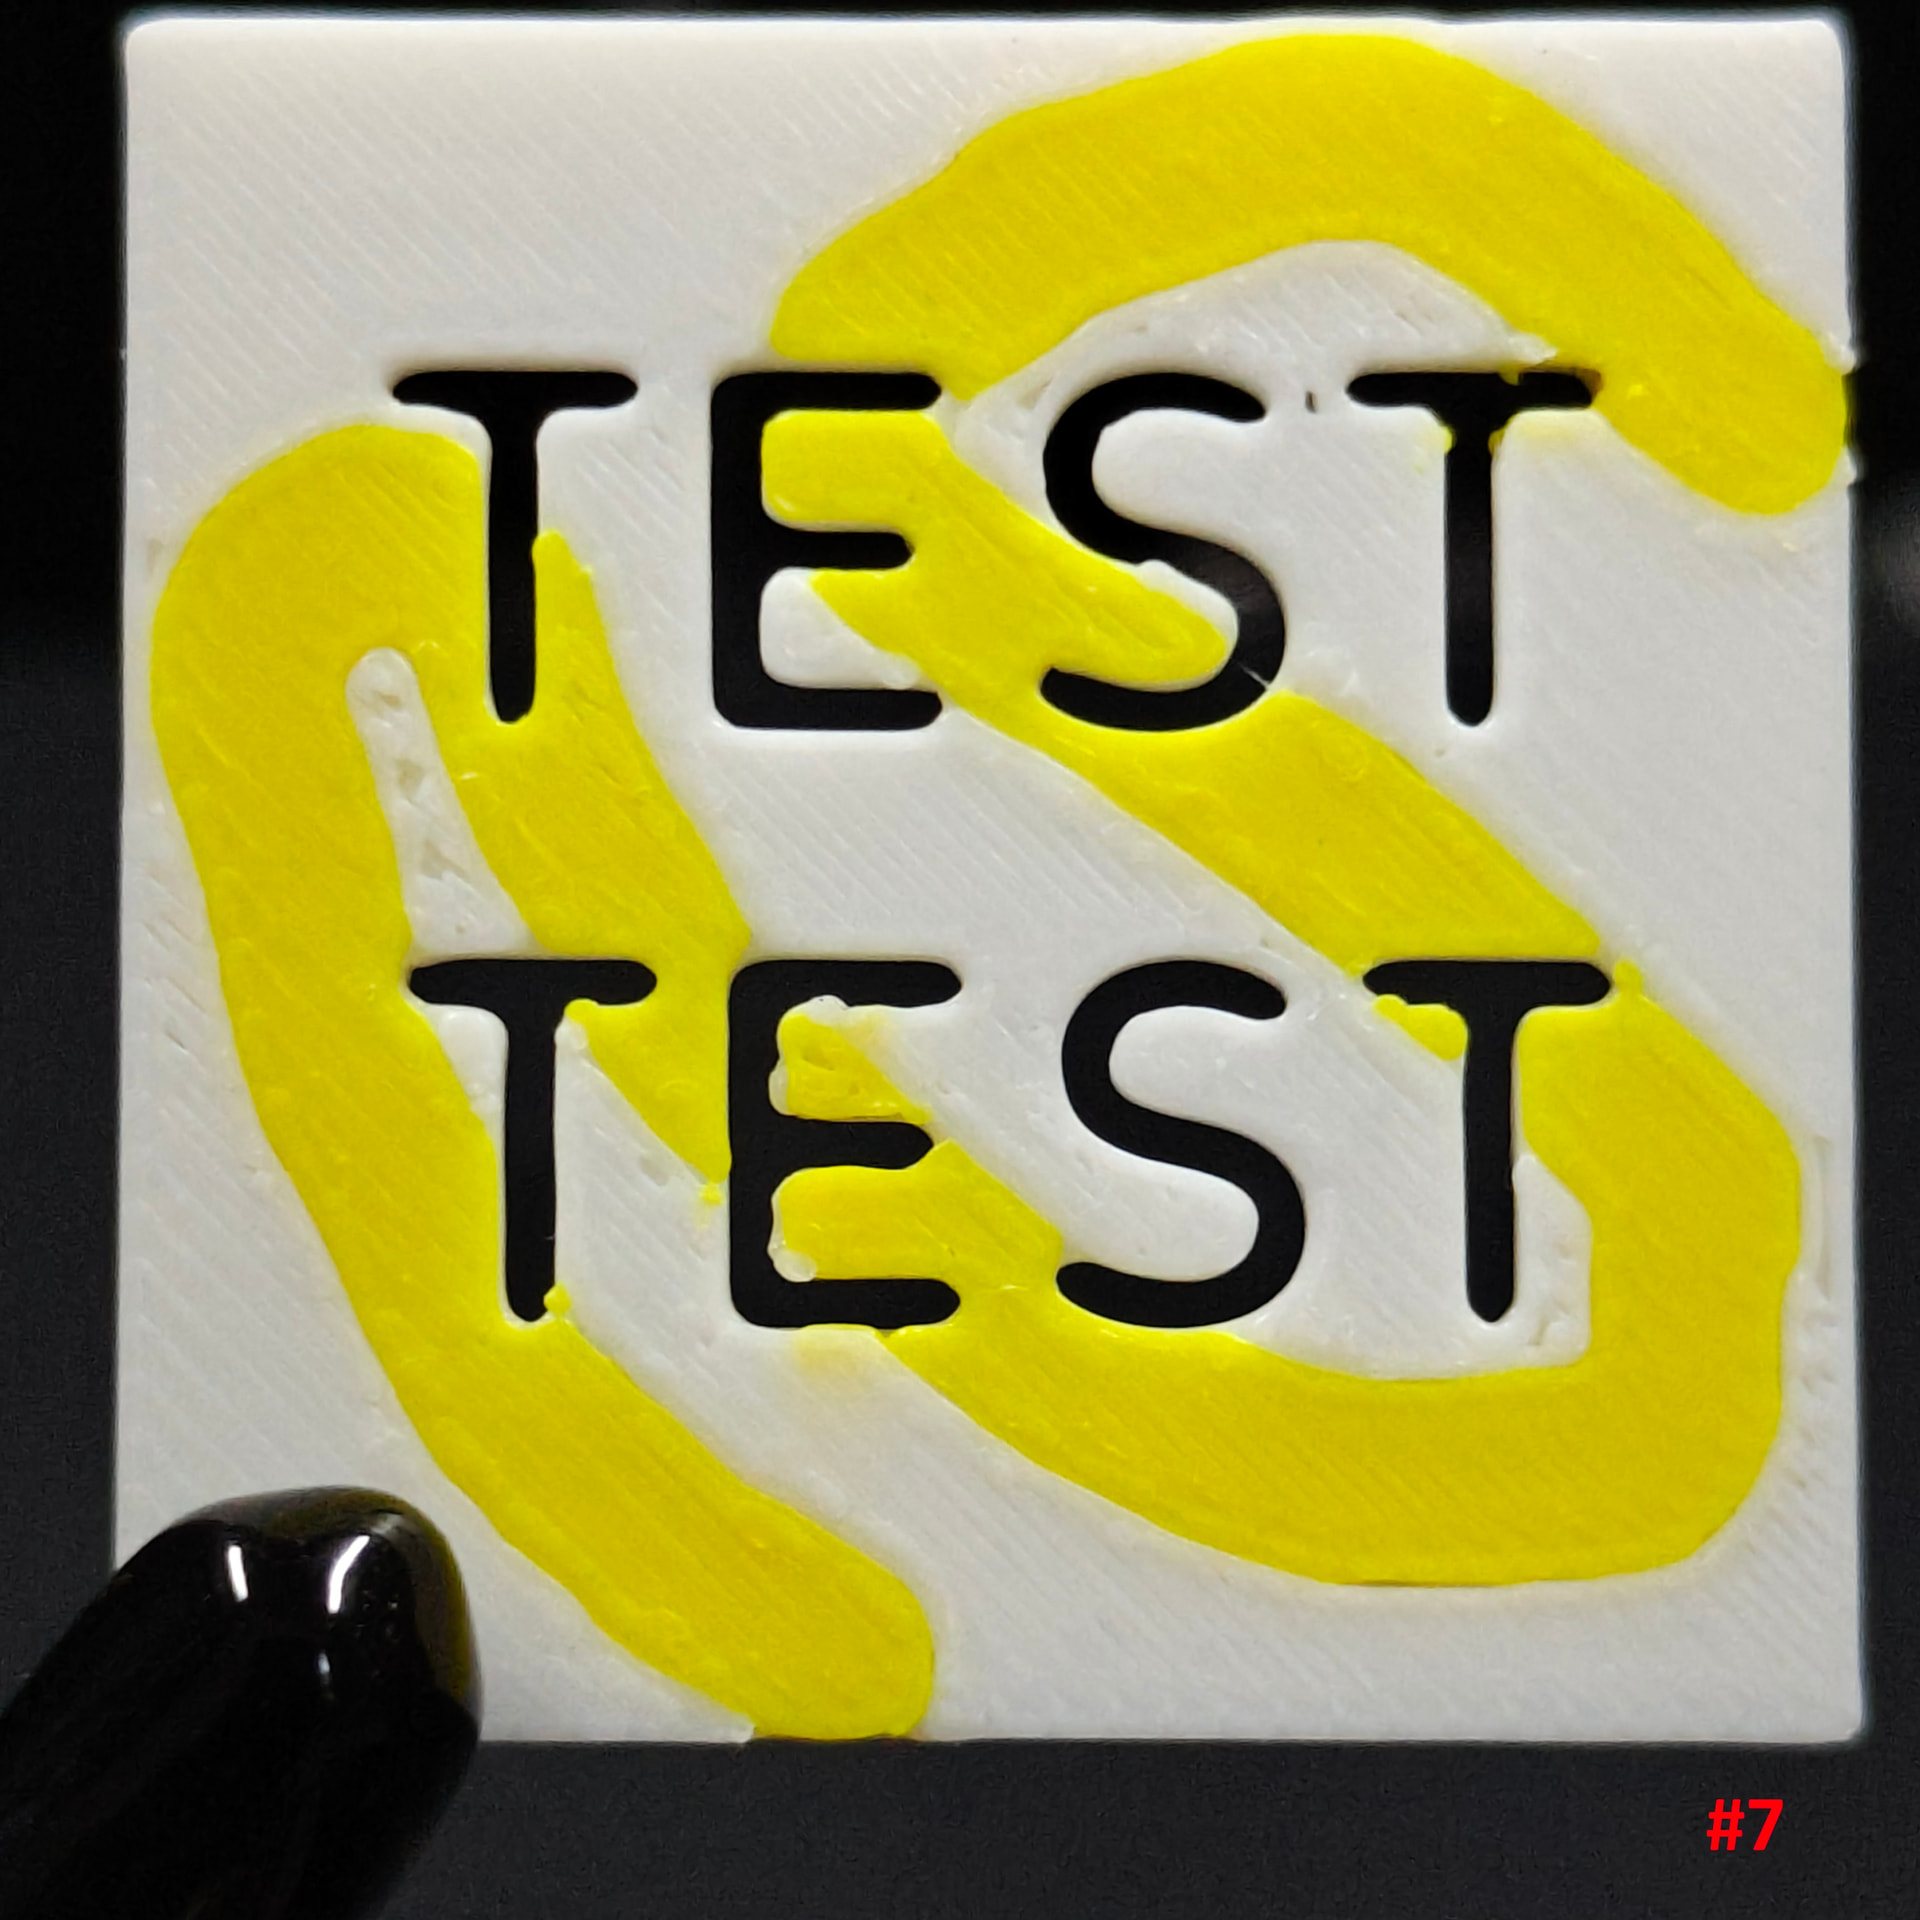
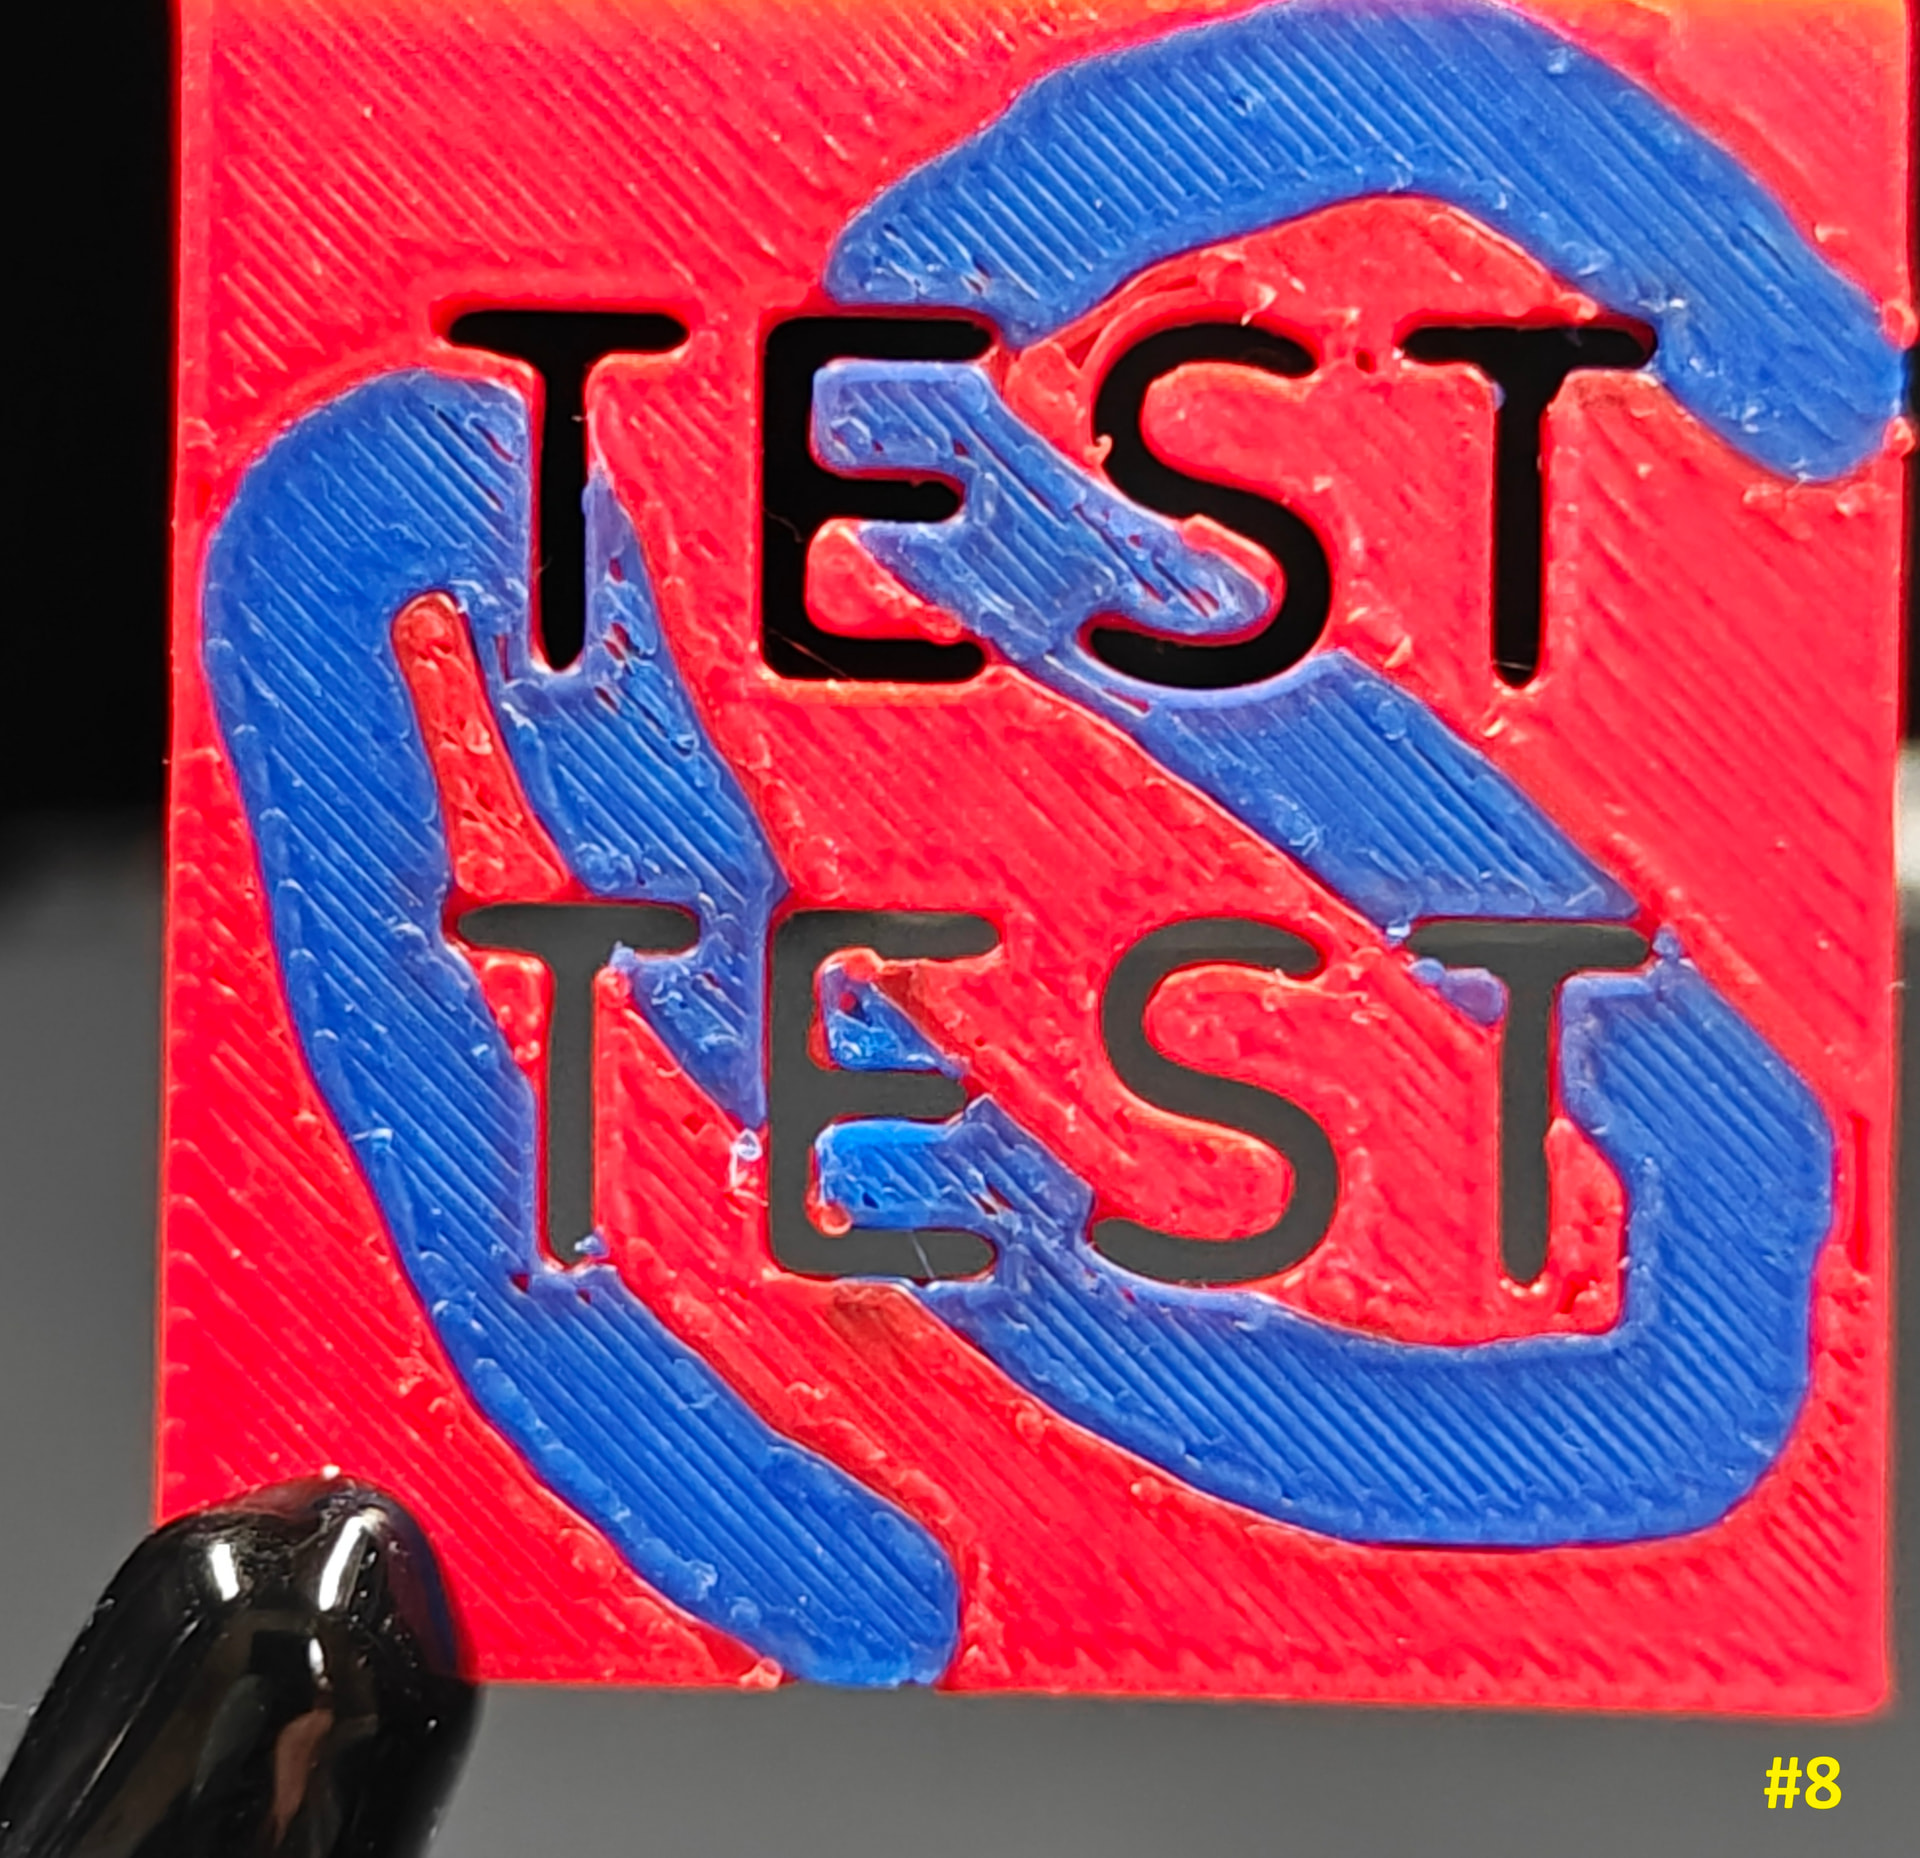
@RogueOhio The model is on it’s back in the 3mf (TEST not spelled backwards) so I also took pictures of back in solid yellow / solid white pics to show initial layer.

Default filament settings used except #5 and #8 (blue)

H2C; 0.4mm nozzle; firmware 01.02.00.00; Cool Plate SuperTack Pro; Bambu Studio beta v2.8.1.55

I used Bambu Studio paint tool for multicolor models. No other slicer settings were changed in 3mf you provided.

  1. BL PLA Basic; Flow 0.99

  2. BL PLA Basic; Flow 0.99 (back of #1 to show initial layer)

  3. BL PLA Basic: Flow 0.99

  4. BL PLA Basic; Flow 0.99 (back of #3 to show initial layer)

  5. BL PETG HF; Flow 0.9894

  6. Multi color #1 + #3

  7. Multi color #1 + #3

  8. BL PLA Basic: Red Flow: 0.99 / Blue Flow: 0.9999

I’d say your prints are significantly better than @RogueOhio . Which slicer version are you using? I’m going to print this myself now, too.