Bambu has made quite a significant design mistake in this regard. It also feels like they’re no longer focusing on print quality, but instead adding more sensors, lasers, and cutters to their printers. The print quality has actually gotten worse compared to models like the P1S and X1C. Fortunately, I also have a Qidi Max4, which handles tall prints better than Bambu—though that’s honestly a bit disappointing.
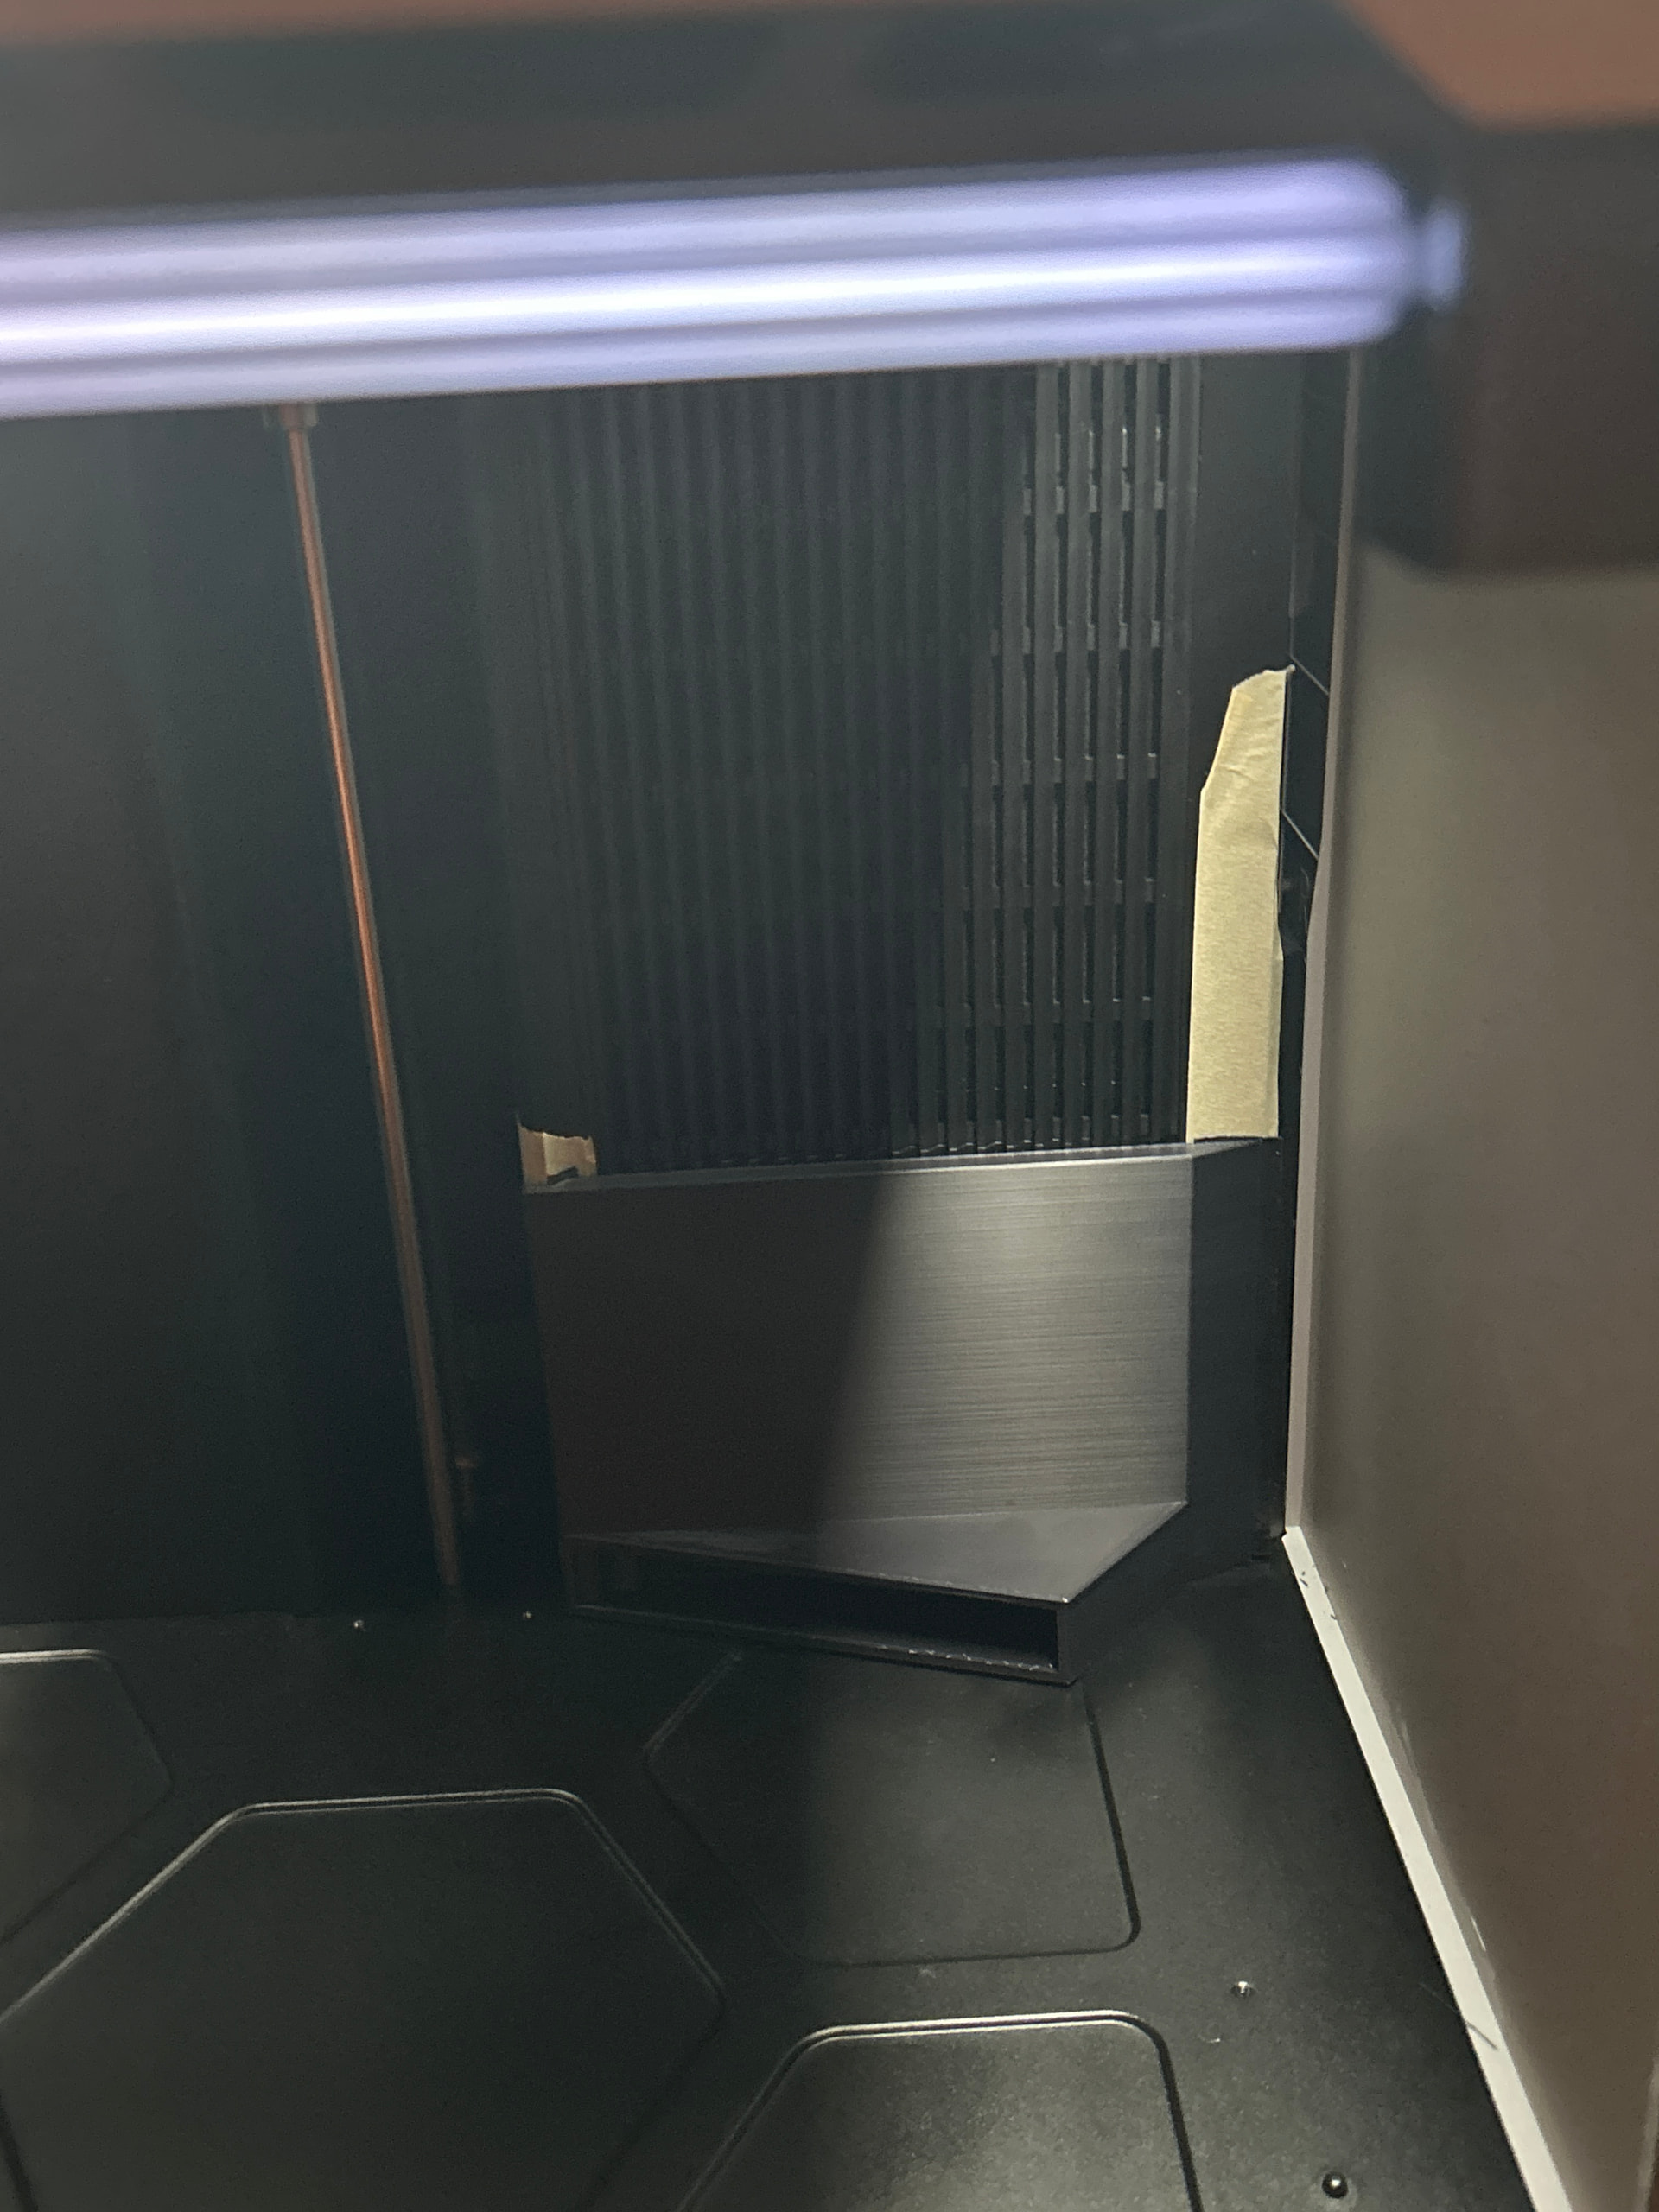
On Qidi Max4, the warm air is directed so that it doesn’t hit the build plate.
Just to build on this and hopefully save people some time and material…
If you’re seeing similar behaviour, one quick check that’s been consistent for me is to run the same print with:
chamber heater disabled
bed temperature at 100°C
enclosure closed (so you still get a passive chamber ~30–35°C)
In my case, that completely removed the layer shift through the affected height range, which at least confirms it’s linked to the chamber heating rather than a mechanical issue.
I wouldn’t suggest anyone runs multiple long tests to try and prove the issue beyond that — one comparison print is usually enough to understand whether you’re seeing the same thing.
If you do confirm it, I’d strongly recommend raising it with Bambu support and referencing this thread so they can see there are multiple users experiencing the same behaviour.
When I raised it, I was advised to use a G-code workaround and was also compensated for the filament used during testing, so it’s definitely worth logging.
The more consistent reports they receive, the better chance this has of being prioritised properly rather than just worked around.
Yeah this would be a valid workaround, but unfortunately the active heating of 60-65C makes layer adhesion around 1.5x stronger from tests i’ve done myself and seen online than a passive chamber of around 35C. Plus less warping! It’s been a few months now, @BambuLab are there any updates on this issue?
Yeah draft shield would help probably but would be unstable at the higher Z heights and would increase filament cost if you did a 2-3 wall draft shied instead of a flimsy 1 wall shield. Really good idea though I bet it would help if filament cost and print times aren’t an issue to some people.
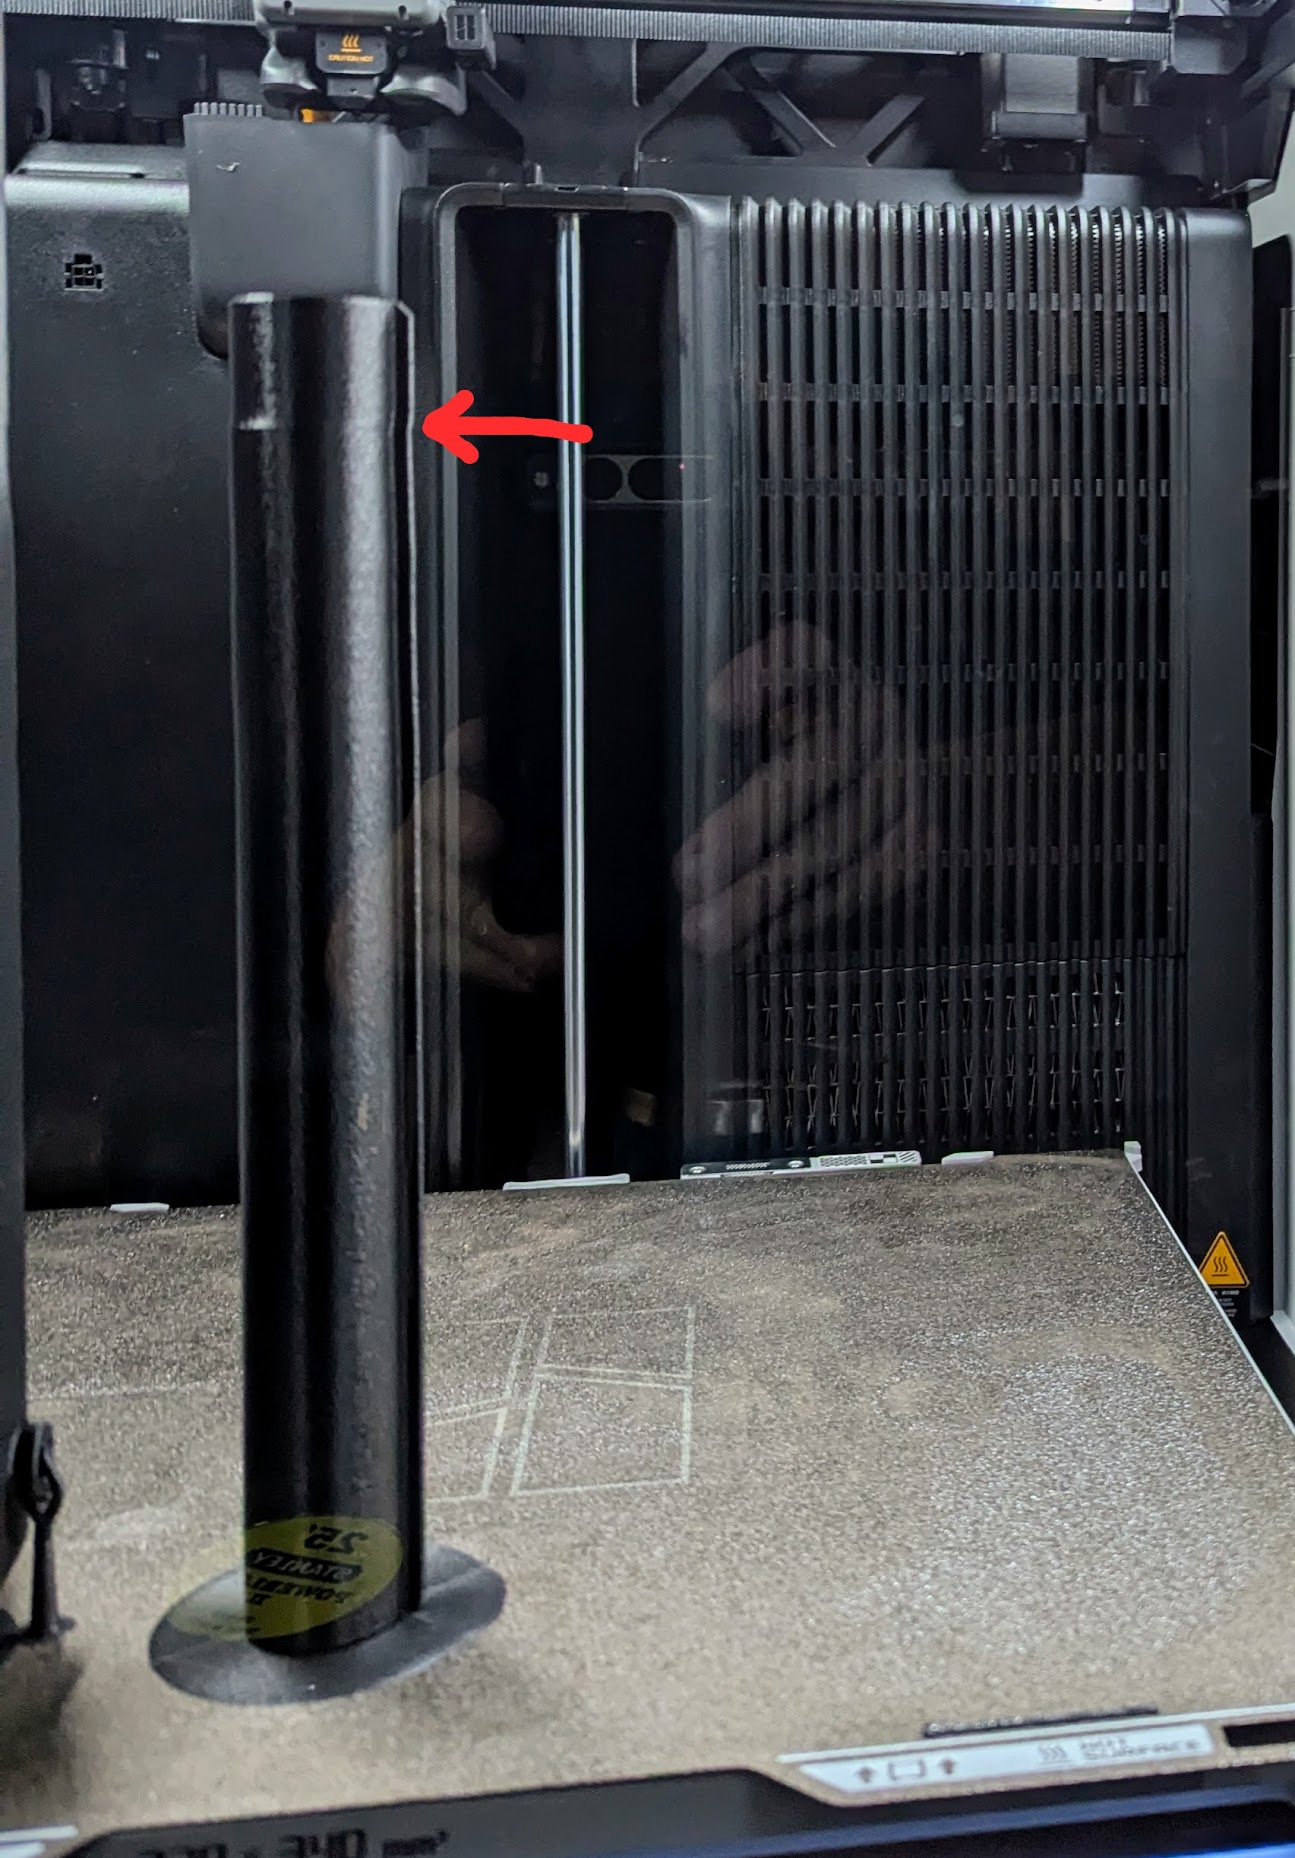
I actually just tested it out and it did not work lol, so don’t waste time or filament. bambu really needs to fix this issue because I only print with PPA-CF for my side business. It starts at 250mm and ends at 285mm then it looks perfect after that. Super annoying.
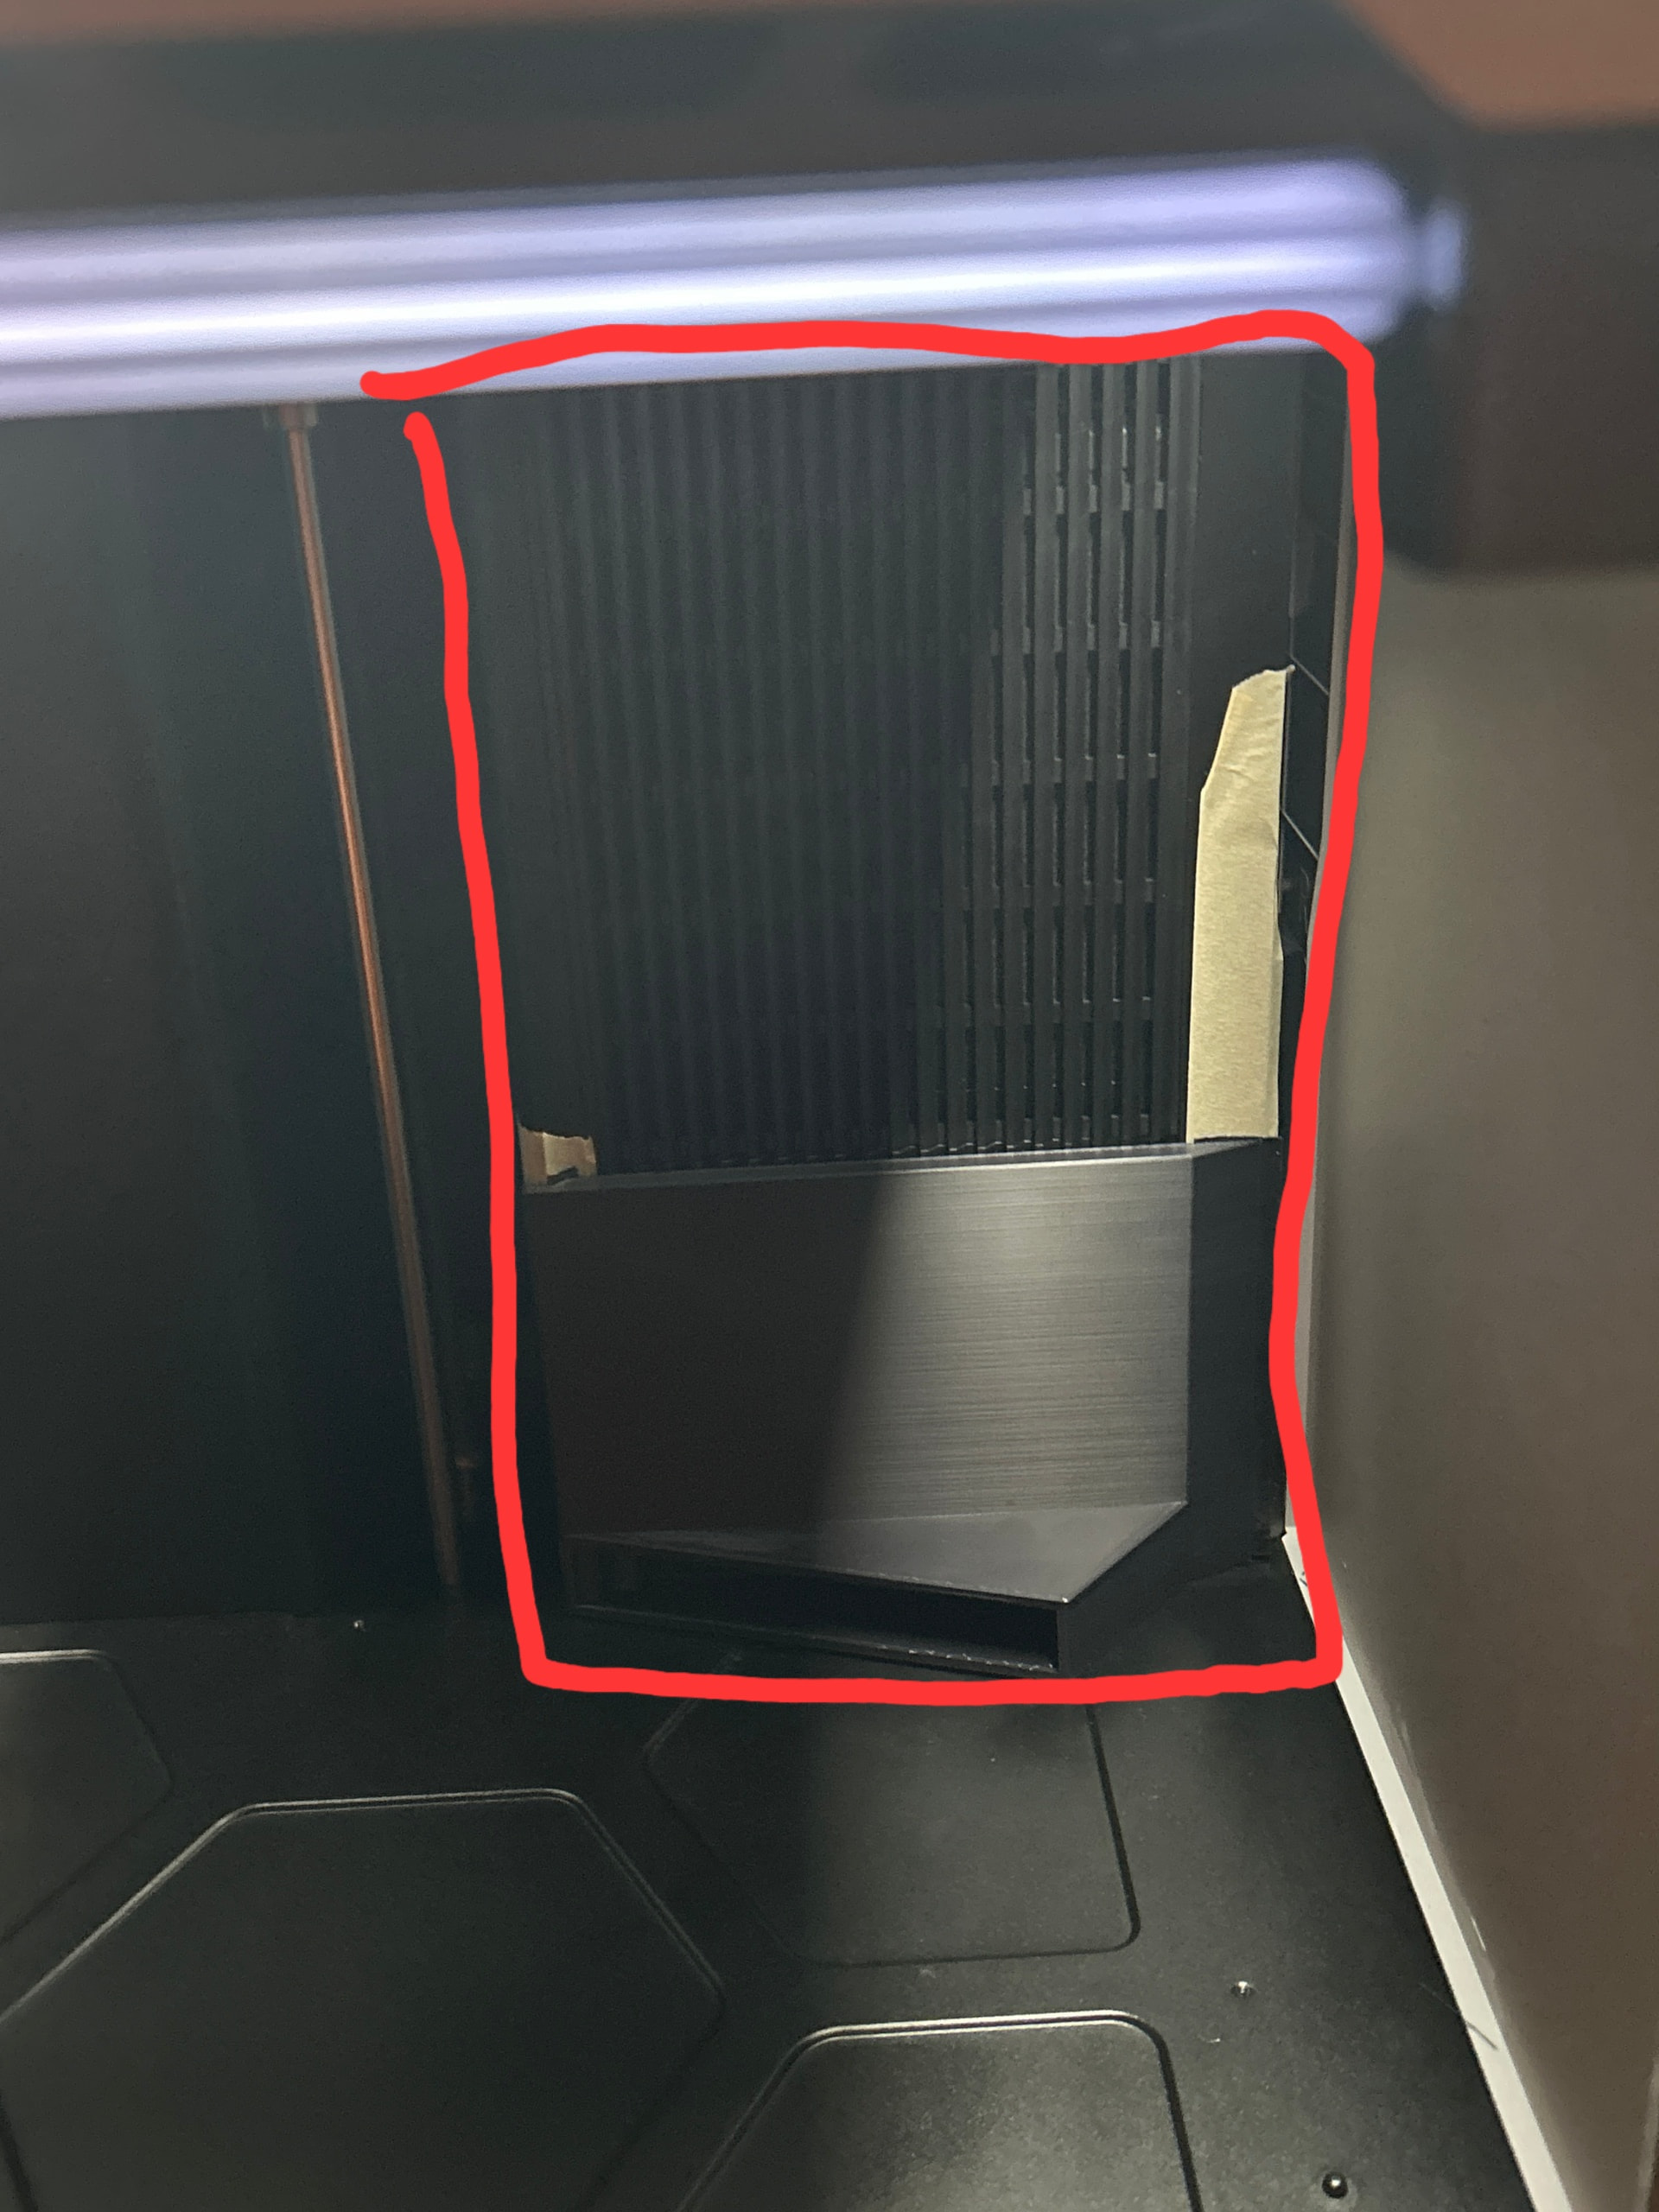
Hey guys, I ended up scanning and making a prototype for the air to be moved below the heatbed.
So far clearance works (very tight though) with 1mm thick double sided tape.
I’ll do a tall test print after confirming fitment at higher temps (thermal expansion could be an issue since the fit is extremely tight)
Will give yall an update and the file if it ends up working. Please feel free to give me any advice on if I should direct the airflow somewhere else or anything else I can improve on.
Thermal expansion ended up screwing it over a lot more than i expected lolll, even when I took the double sided tape off the inside and just overlaid it with regular tape instead. I’ll make it a good bit skinnier and retest
What if we replaced this entire plastic part with a redesigned grille? That would create more space for airflow control, especially down at the lower section.
Yeah I thought of that, but the only problem is we’d probably have to cut the lower section cover where the actual chamber heater and fan is. That part unfortunately doesn’t come off like the upper chamber filter cover does.
New update guys so the newer one I designed works, the clearance is good now. But the only problem is the upper part of the chamber doesn’t get as hot. (Measured by feel and by a infrared thermometer gun)
The lower area where the airflow was directed measures approximately 64-66C. Whereas the upper areas of the chamber measure 45-50C.
I might go ahead and redesign another prototype where some of the air is directed down like the original prototype, some at a 45° angle, and some of the air directed straight up. What do you guys think?
Im not experienced very much with thermodynamics and stuff like this so I’d appreciate some feedback
Hello, great to hear that your prototype is making some difference. It would be great to have some “insert” only if we need to print tall objects with heated chamber. Thank you for your approach to this problem.
I first raised this with Bambu Support on 6 February after seeing the same repeatable ASA / ASA-CF shift around ~250–280 mm discussed here.
After just over 3 months of back and forth with Bambu Support, including escalation, Bambu’s latest update today is that the issue is now under active R&D development for a firmware improvement.
If anyone else is seeing the same behaviour, please raise a support ticket with Bambu and include your print height, material, and repeatability so the issue continues to gain visibility and priority.
I’ll share any further updates as they come through.
I am having the same issue on a H2S I just received last week. Following the response format of a previous post:
Tall PPA-CF prints (around 300-330mm)
Consistent X/Y shift or “twist” occurring in a narrow band around ~250–270 mm
Print quality is otherwise excellent below and above this range
I am not printing with PLA (no chamber heat filaments) so I cannot comment on that.
I did not know of this error before I purchased the printer, and it did not turn up when I searched tech support. So I contacted Bambu and received the same suggested fix:
G-code:
{if (layer_z==230)}
M141 S0
{endif}
I am not happy with this solution. If I am printing parts with the chamber heater on, then I need the chamber heater to be on. Turning it off at a particular height is a band-aid solution. If I spent more money to buy a printer with a large volume, I need to be able to use the whole volume.
This is not a problem that can be corrected easily if it is indeed an airflow issue. This is a problem that should have been caught by Bambu with pre-production testing. Bambu may have a serious problem on their hands.
The immediate issue for me is I just bought this printer. I am within the 14-day return window. If I do not return the printer now, I am stuck waiting for the firmware solution, and hoping it is a viable correction.
If the firmware fix is to turn the heater off above 230mm, like in the g-code fix they are providing, that is not a viable fix.
The only firmware change I could see that MIGHT fix this is if the speed of the chamber fan is variable, and it can be reduced when the bed is below 230mm. But, that has a risk of causing other problems. I would test this myself, but AFAIK I cannot execute g-code commands in real time like I can with Duet or the like, and I do not want to trial and error slicer embedded commands with expensive filament.
As mentioned, turning off the heater completely is going to degrade layer adhesion issues. Lower chamber temperatures mean weaker bonds between layers for the higher performance filaments. This is well documented in the community.
It’s a new machine, so I’d log the ticket with Bambu now and see what they advise — they may agree that returning it within your 14-day window is the better route rather than waiting on a workaround or an unconfirmed fix.
Reference this thread in your ticket so they can see it’s not an isolated case. The more H2S owners that raise it early, the quicker we’ll understand whether Bambu see this as firmware, thermal design, or something requiring a wider solution.
I’ve already raised and escalated my own ticket. Bambu have compensated me for filament used during failed prints and testing, but I’ve also made it clear I’m not looking for a workaround or a software band-aid — I want the printer to perform as sold, across the full build height with engineering filaments and active chamber heating. If the root cause can’t be properly resolved, I may ultimately ask for my own unit to be returned.
I would add the response from customer support has been quick throughout, but you may need to ask for the matter to be escalated if you receive a standard first-line reply.
I tried printing the same part with the g-code modification prescribed by Bambu tech support. Unfortunately I saw the same distortion in the same location.
Some additional information… I watched the last 30 minutes of the print and the chamber temperature on the printer screen indicated 56C. This is with the heater off so the chamber is only being heated by the bed (at 100C) and the hot end (at 300C). This is encouraging since the target temperature is 60C, so there is a drop, but not a terrible one. However as pointed out by someone in this thread, the temperature distribution in the chamber is more uneven (no fan).
I was thinking - maybe try to put whole printer in grow tent? Cut every possible inlet/outlet of cold air from printer That way heater will use the same air with the same temperature all the time. You can also try grow tent with g-code that disables heater above 230 mm height - air inside printer should not drop because everything will be sealed in grow tent
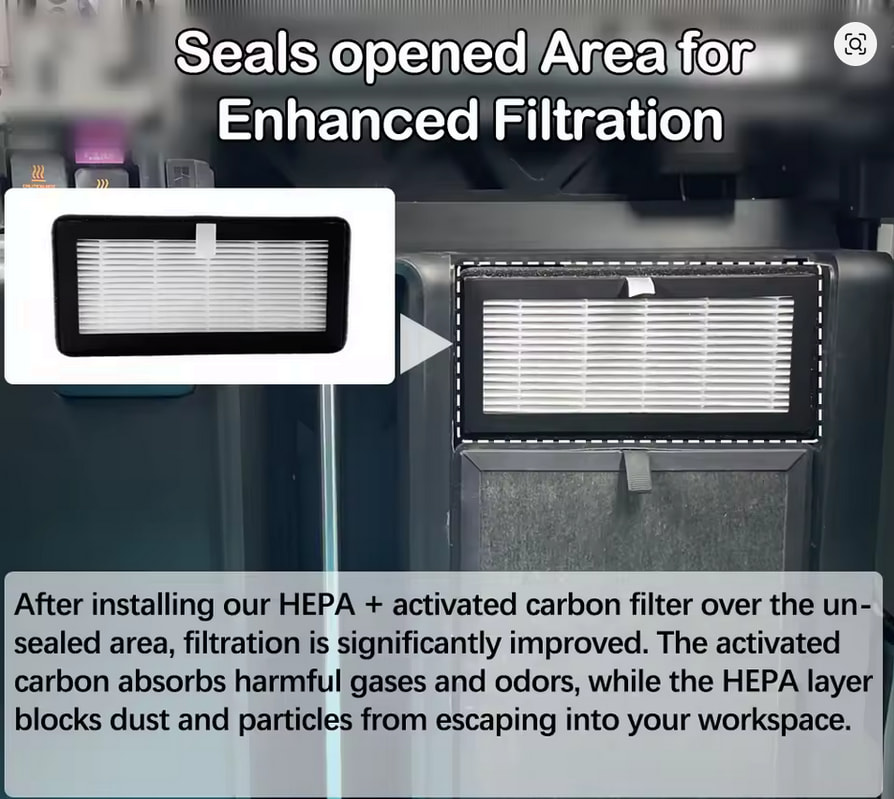
Edit - you could also try ty add additional filter like this one in picture - it (apart from adding additional filtering layer) increased my chamber temperature about 4 degrees more.