Can you share your entire print profile in some way along with the model? I would like to try it on my own machine.
Im starting to suspect this might be QC failures of some kind, perhaps extruder motor related.
Can you share your entire print profile in some way along with the model? I would like to try it on my own machine.
Im starting to suspect this might be QC failures of some kind, perhaps extruder motor related.
@JJ_Golmon I can’t thank you enough for all of your work on this. I’m new to 3D printing and only just learned that ironing is a a thing lol. I found your post looking for ironing settings to smooth out a Star Wars themed light switch plate after the stock settings were meh. Your methodology is how I operate and your detailed trouble shooting helped me understand just how complex this feature can be. While my OCD side covets the glass finish, my print will be painted which will hide most of the imperfections. It looks like the best results you found were Temp 220, 55mm/s, 15% with 15mm spacing. Is that correct or was the high quality print profile you linked to any better? Have you had any better luck with a different setting?
Also… If it’s helpful, I’d happily test print for you using your settings on my X2D. It would give you a separate machine to see if the problem is consistent on multiple machines ruling out a possible anomaly on your machine. There may be variables that make that impractical like PLA brand / prep, set up, environment, etc. but I thought I’d throw it out there.
Thankyou for this!
I’ve been trying everything, wasting loads of filament and time trying to improve ironing.
The parts I produce need to have good ironing. I’m not sure what to do, I directly chose the X2D for manufacturing small parts from engineering grade filaments, using dissimilar material support, as many of us did. I’ve wasted days on this problem.
At least I now know, it’s not me.
My X2D needs 35mm/s and 35% flow for a decent ironing with BBL PLA Basic.
I tried it yesterday and don’t worked for me
Thanks for the idea
After burning through a full 1kg spool on this, I think I’ve finally isolated what’s actually going on, and it’s more precise than my original post.
What I did:
The pattern that emerges: ironing is excellent and reproducible on SIMPLE geometry (no matter the size), but breaks down specifically on COMPLEX geometry — holes, color changes, multiple transitions. This is different from what I originally thought (small vs large surface) — it’s really about toolpath complexity, not surface area.
My current theory: this smells like a firmware-level issue in how the toolpath/flow control handles transitions and segment breaks, not a parameter problem. A perfect result on a simple shape at the exact same settings that fail on a complex one is hard to explain with “wrong parameters.”
Support has now reproduced the core issue on their end (tested on a P2S with my file), which is progress, though they’re framing it as an inherent FDM limitation for now. I’ve pushed back and asked about the simple-vs-complex distinction specifically.
Anyone else seeing this same pattern — great ironing on simple shapes, breaking down on anything with holes/color changes/complex transitions? Would be very useful to know if this is X2D-specific or shows up on P2S/H2D too.
I supose each machine has his own tolerances. My A1 Mini works perfectly with 25/15.
Yep sure, for my a1 was 35/30
Yep it’s not only you, I talked on several Facebook groups. 3/4 X2D user have problems with ironing.
I would be happy to know if H user have same issues cause they have same extruder
Really appreciate the kind words, and thank YOU for offering to test on your own machine — that’s genuinely the most useful thing anyone could offer at this point, since it would help rule out whether this is specific to my unit or a broader X2D thing. Can’t wait to see the Star Wars light switch plate once it’s done!
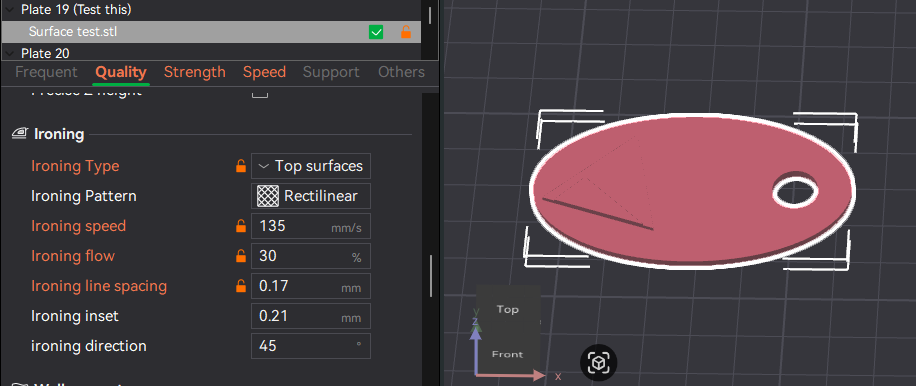
To correct/update: my optimal settings have changed since that earlier post. Current setup:
Top surface (independent of ironing): 30mm/s speed, 0.32mm line width
Ironing: 135mm/s, 30% flow, 0.17mm line spacing
Surprisingly, high speed ended up giving the best results, contrary to what’s usually recommended — a full speed/flow sweep confirmed it wasn’t a fluke.
Heads up though: I’ve found this only gives a truly great (glass-smooth) result on simple geometry. On more complex shapes (holes, color changes, multiple transitions) it still breaks down, even with these settings. Since you’re painting the piece afterward, imperfections should be much less of an issue for you either way — but wanted to flag it in case your design has holes or multi-material sections.
I just uploaded the test file to MakerWorld if you (or anyone else) wants to try it on your own printer: File with my experimation since new flow calibration
If you do get a chance to test with the settings above, even just on a simple flat piece, I’d love to know what you get — especially since it would be a genuinely independent data point (different filament prep, environment, etc.) that could help confirm or rule out a hardware-specific cause.
I’m about to try your specs on my current headache. Wish me luck.
I do wonder how many people just accept mediocre. The amount of Benchies that I see people, often youtubers, calling ‘perfect’, look horrible to me. I manually tune every new filament I get and record it all on a spreadsheet  I’ve found the Bambu auto PA tuning to be very inconsistent, and it easily gets confused by glossy surfaces.
Seems like H2C has the same ironing journey:
Same extruder, and relatively new printer
Hope a firmware patch this
Wow. I too just upgraded from a P1S with absolute perfect ironing with minimal effort to an X2D and I’ve been pulling my hair out all day with flow calibrations, ironing tests, etc. Then I stumbled on this thread and read the entire thing. Thank you so much for all the detailed work and documentation you’ve put into this. I’m going to run a ironing calibration model you linked from MakerWorld and then try your most recent final results you have here.
I’m a bit disappointed that the X2D is on the struggle bus with this issue, but I think the work you did here is incredible. Again, thank you so much for this effort you put into it and I’ll see what results I can get tomorrow and post an update.
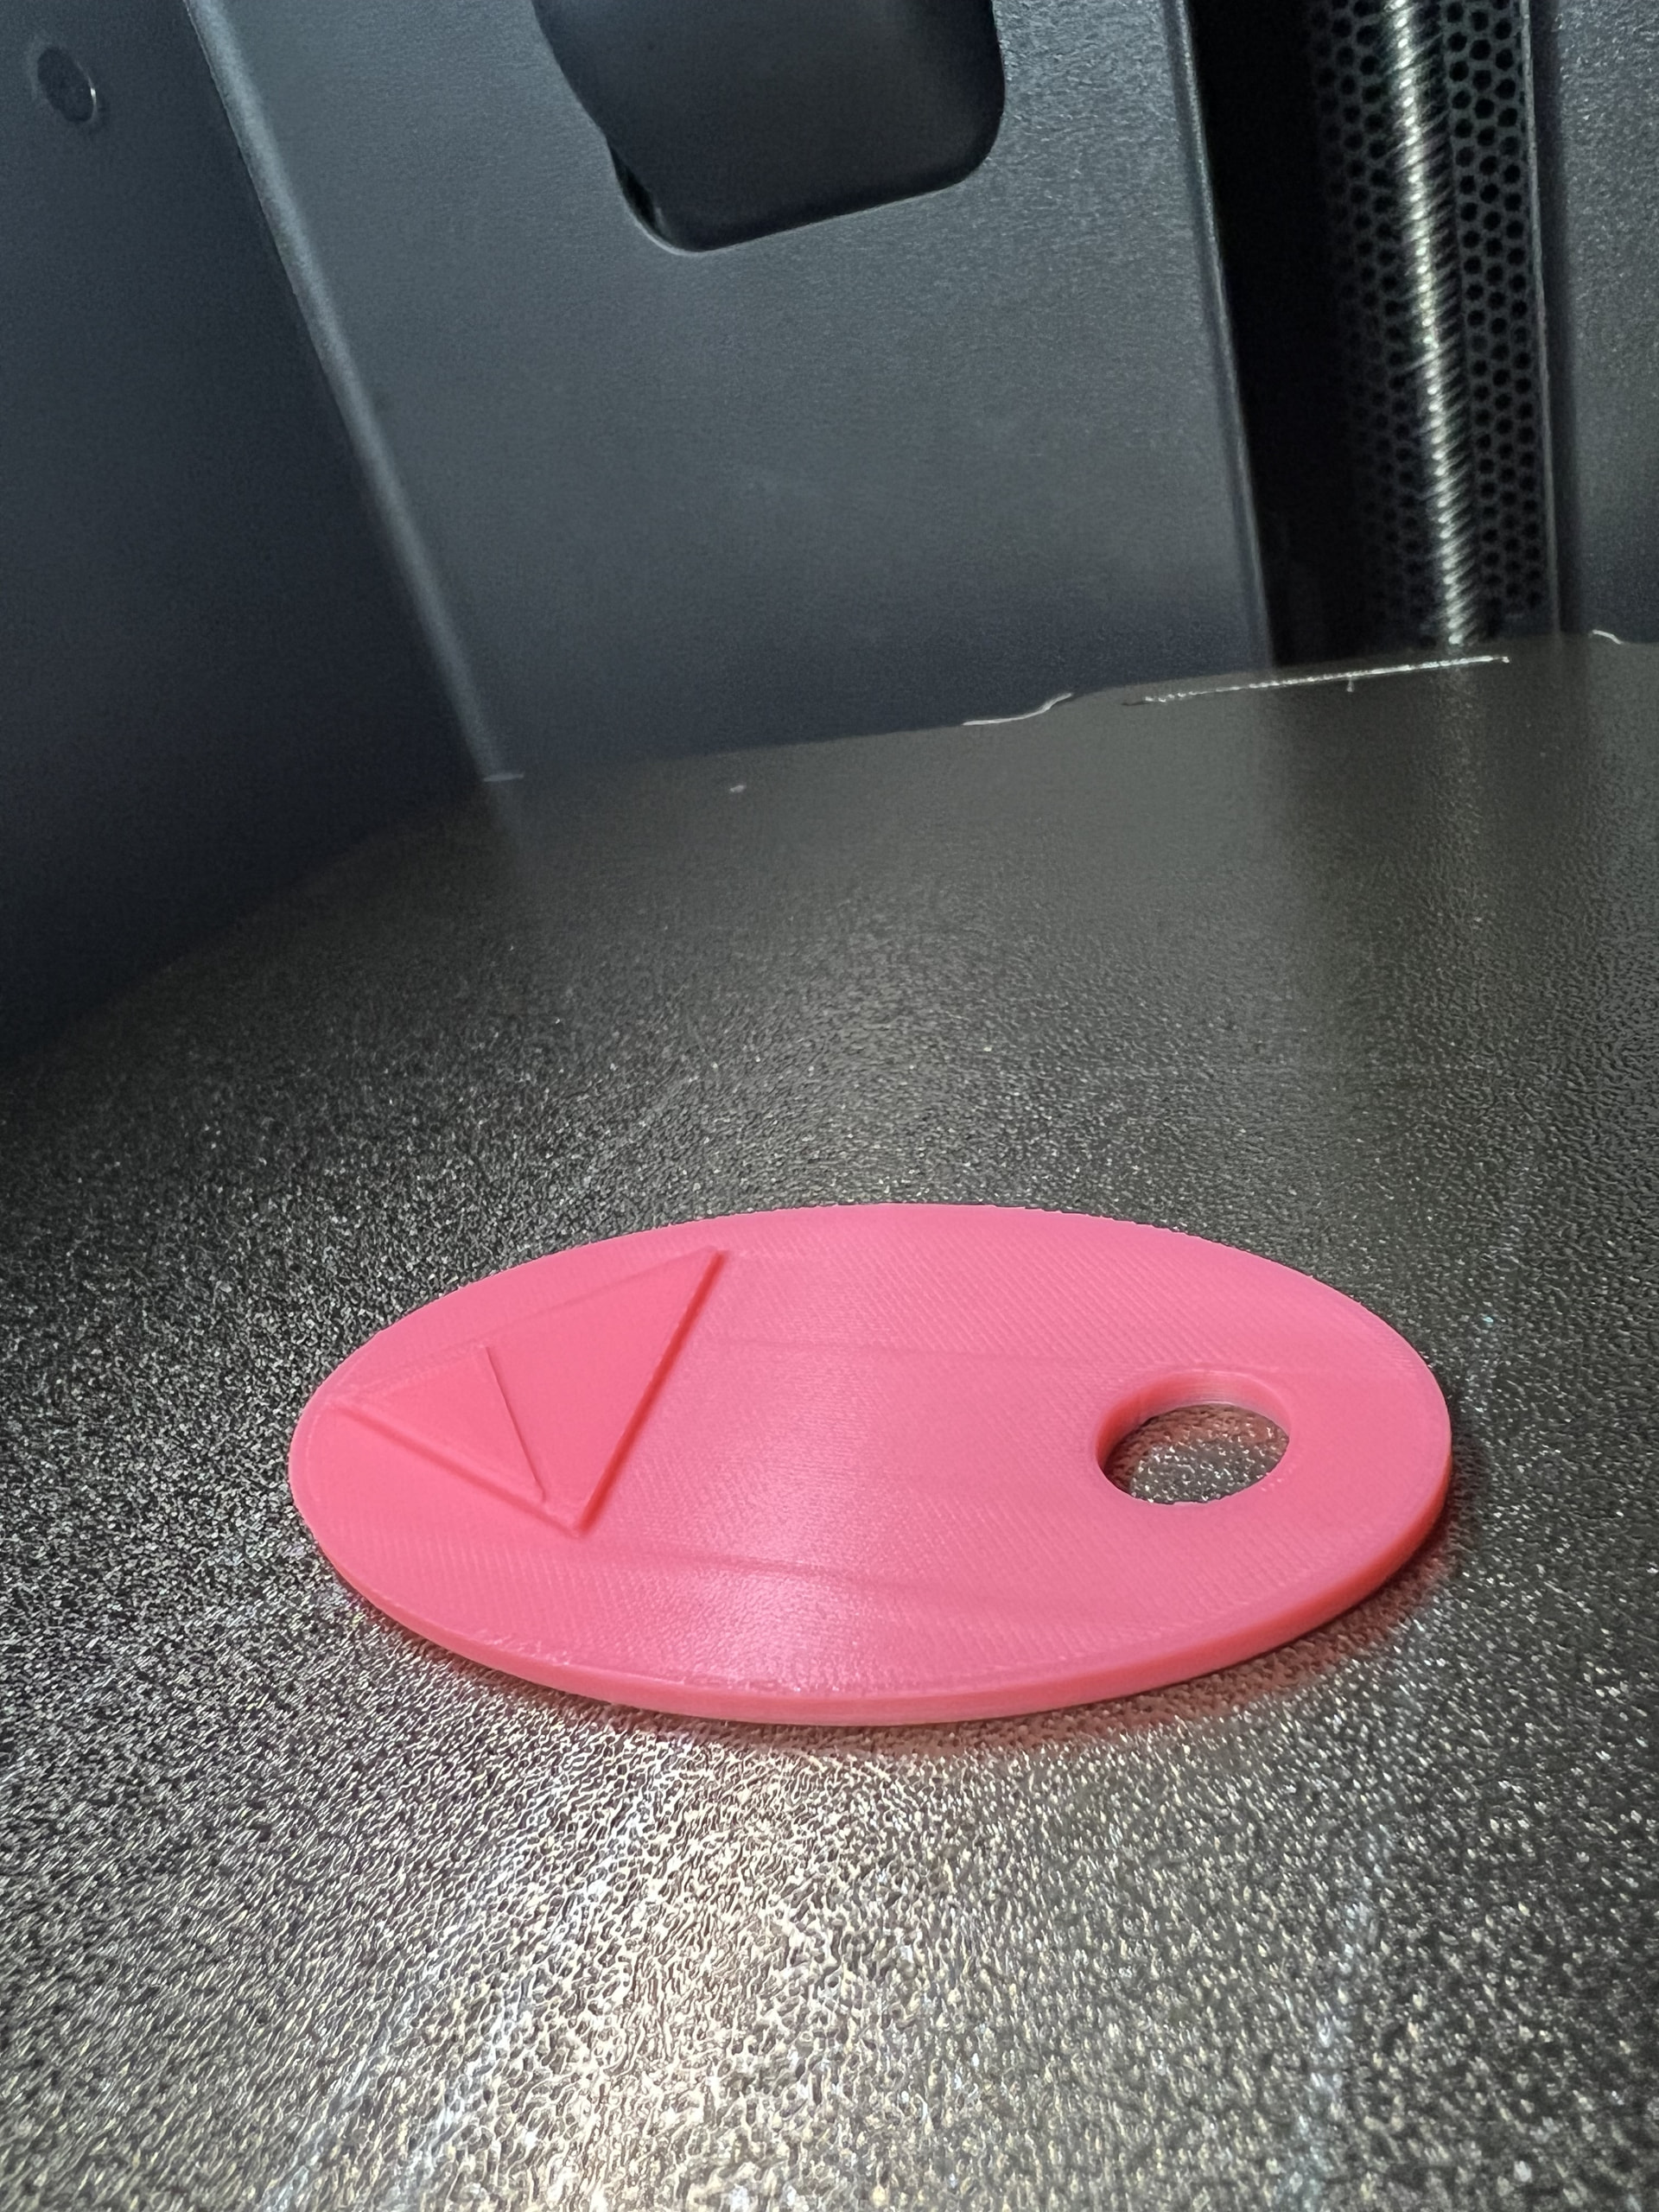
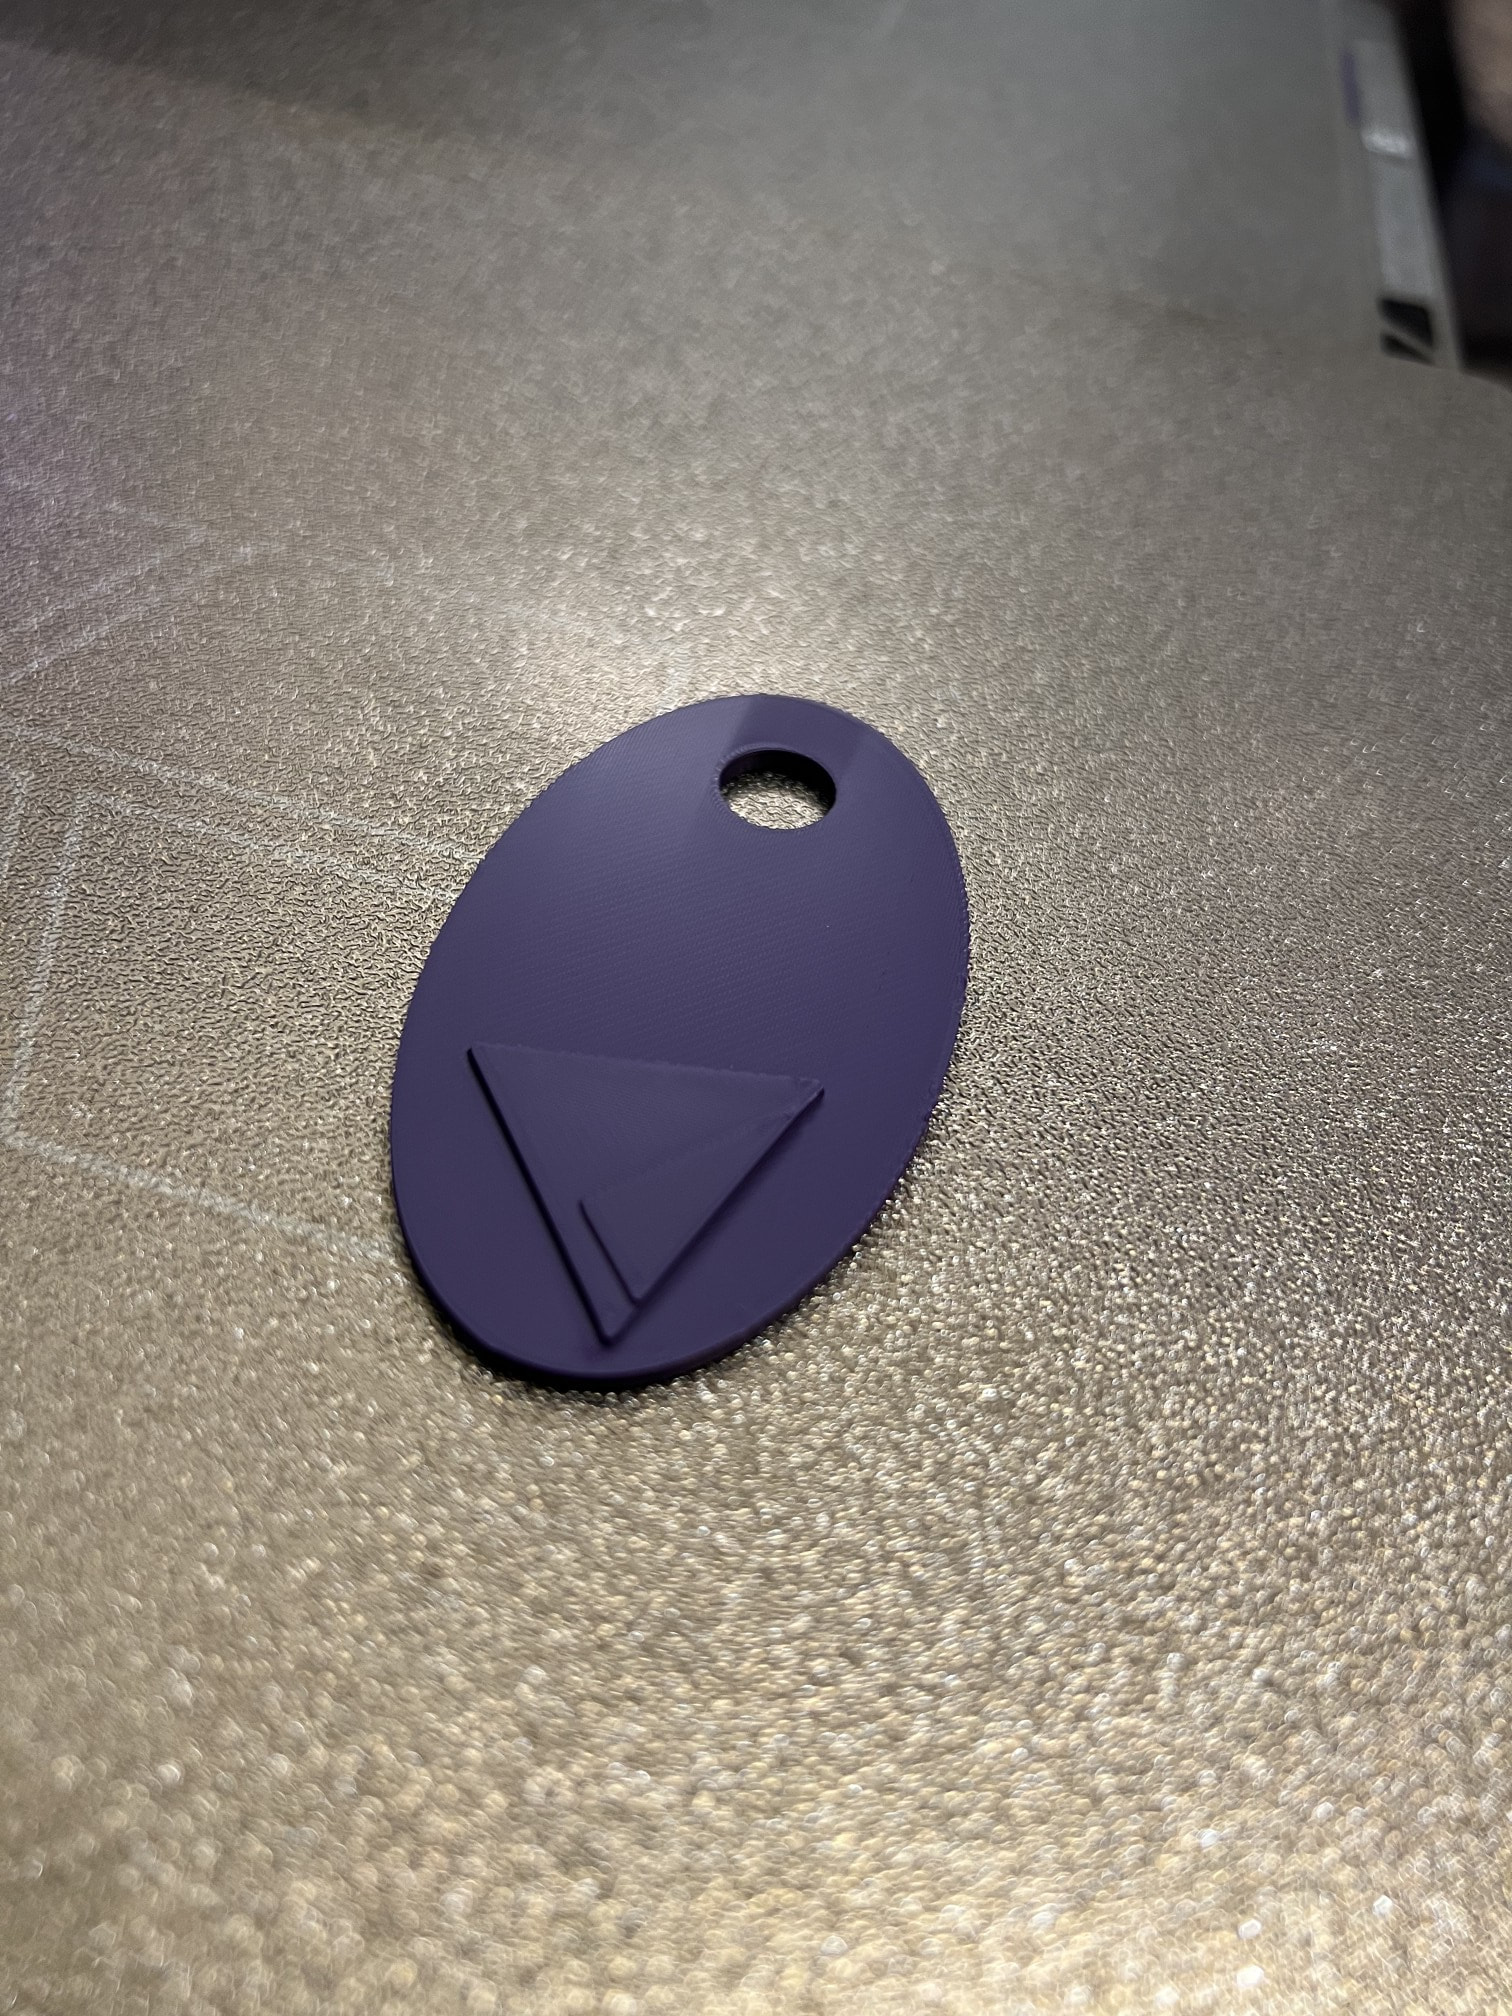
@JJ_Golmon I got too invested and had to run your quick test model tonight. Here’s it fresh off my X2D with your latest settings. It looks like the best ironing I’ve yet too see coming off the X2D, but it’s still pretty rough. I think you’re right that faster is way better. I’m almost considering trying a few silly tests tomorrow at some even faster speeds.
At this current quality I think having ironing off and leaving the normal top surface finish is just as good  . Tomorrow I’ll run it on my P1S to get a side-by-side comparison.
Apologies in advance for choosing pink, but it was the PLA Basic I already had loaded up from an earlier ironing test. If I run more I’ll choose a darker purple so it’s easier to see  .
I got one of the early X2D printers, and the issues have been crazy. Definitely needed some time, especially with the Bowden extruder. I’m not so concerned about the Bowden idea, but I have had a lot of issues with this.
Thanks again to @Dabo who’s engaged with this thread, mentioned pink filament earlier, honestly it looks great too 
Following up on my last post: I asked support directly about the simple-vs-complex pattern I found. Here’s their explanation.
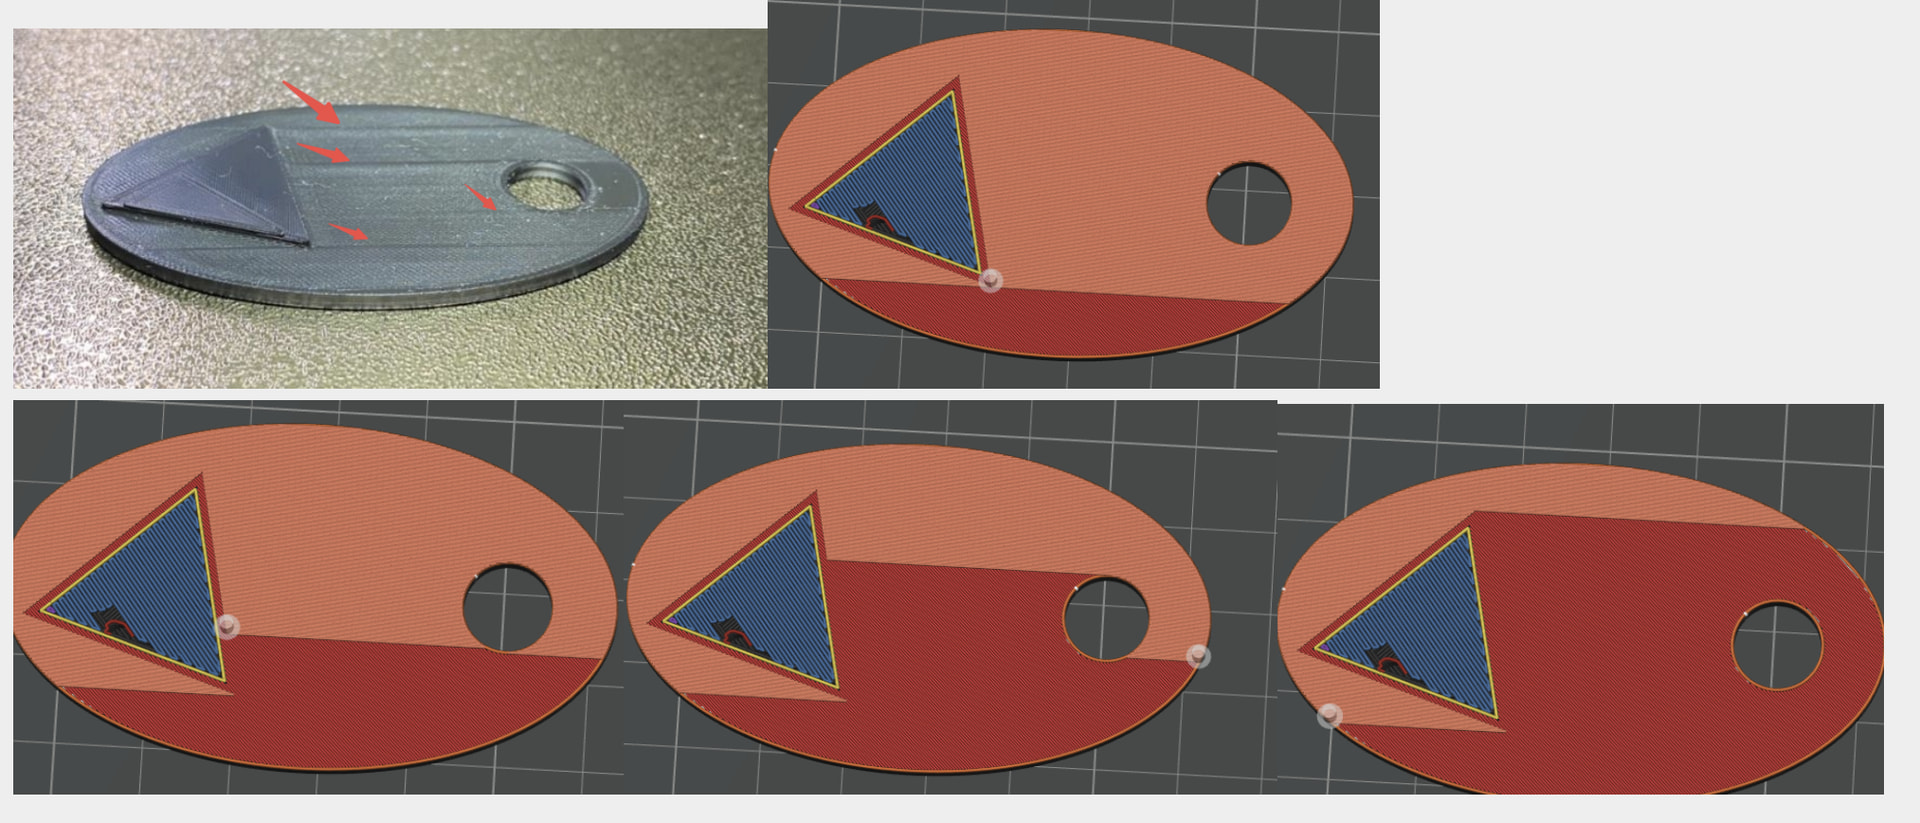
Their answer: the shadow lines are tied to how the slicer sequences printing when a model has perforations or multiple zones in the center. When there are holes/cutouts, the print order of the surface layers changes — and in the slicer preview, the zone transitions line up exactly with where the shadow lines appear. This sequencing is calculated by their algorithm as the “optimal path” and generally isn’t manually adjustable.
Their conclusion: they don’t consider this a firmware bug or hardware fault — more that ironing is inherently hard to perfect, and without precise tuning it can degrade quality instead of improving it. They said meaningful improvement may be difficult right now, but offered to run parallel tests if I send more files.
So this actually confirms the pattern I described in my last post — the “column that works, column that fails” behavior on the multicolor piece, and the shadow lines at the hole tangents, both line up with their explanation of zone-transition sequencing.
Still pushing on whether this is X2D-specific or shows up the same way on other Bambu machines with a similar toolhead. If anyone wants to test my uploaded file on a different model, that’d be genuinely useful data.
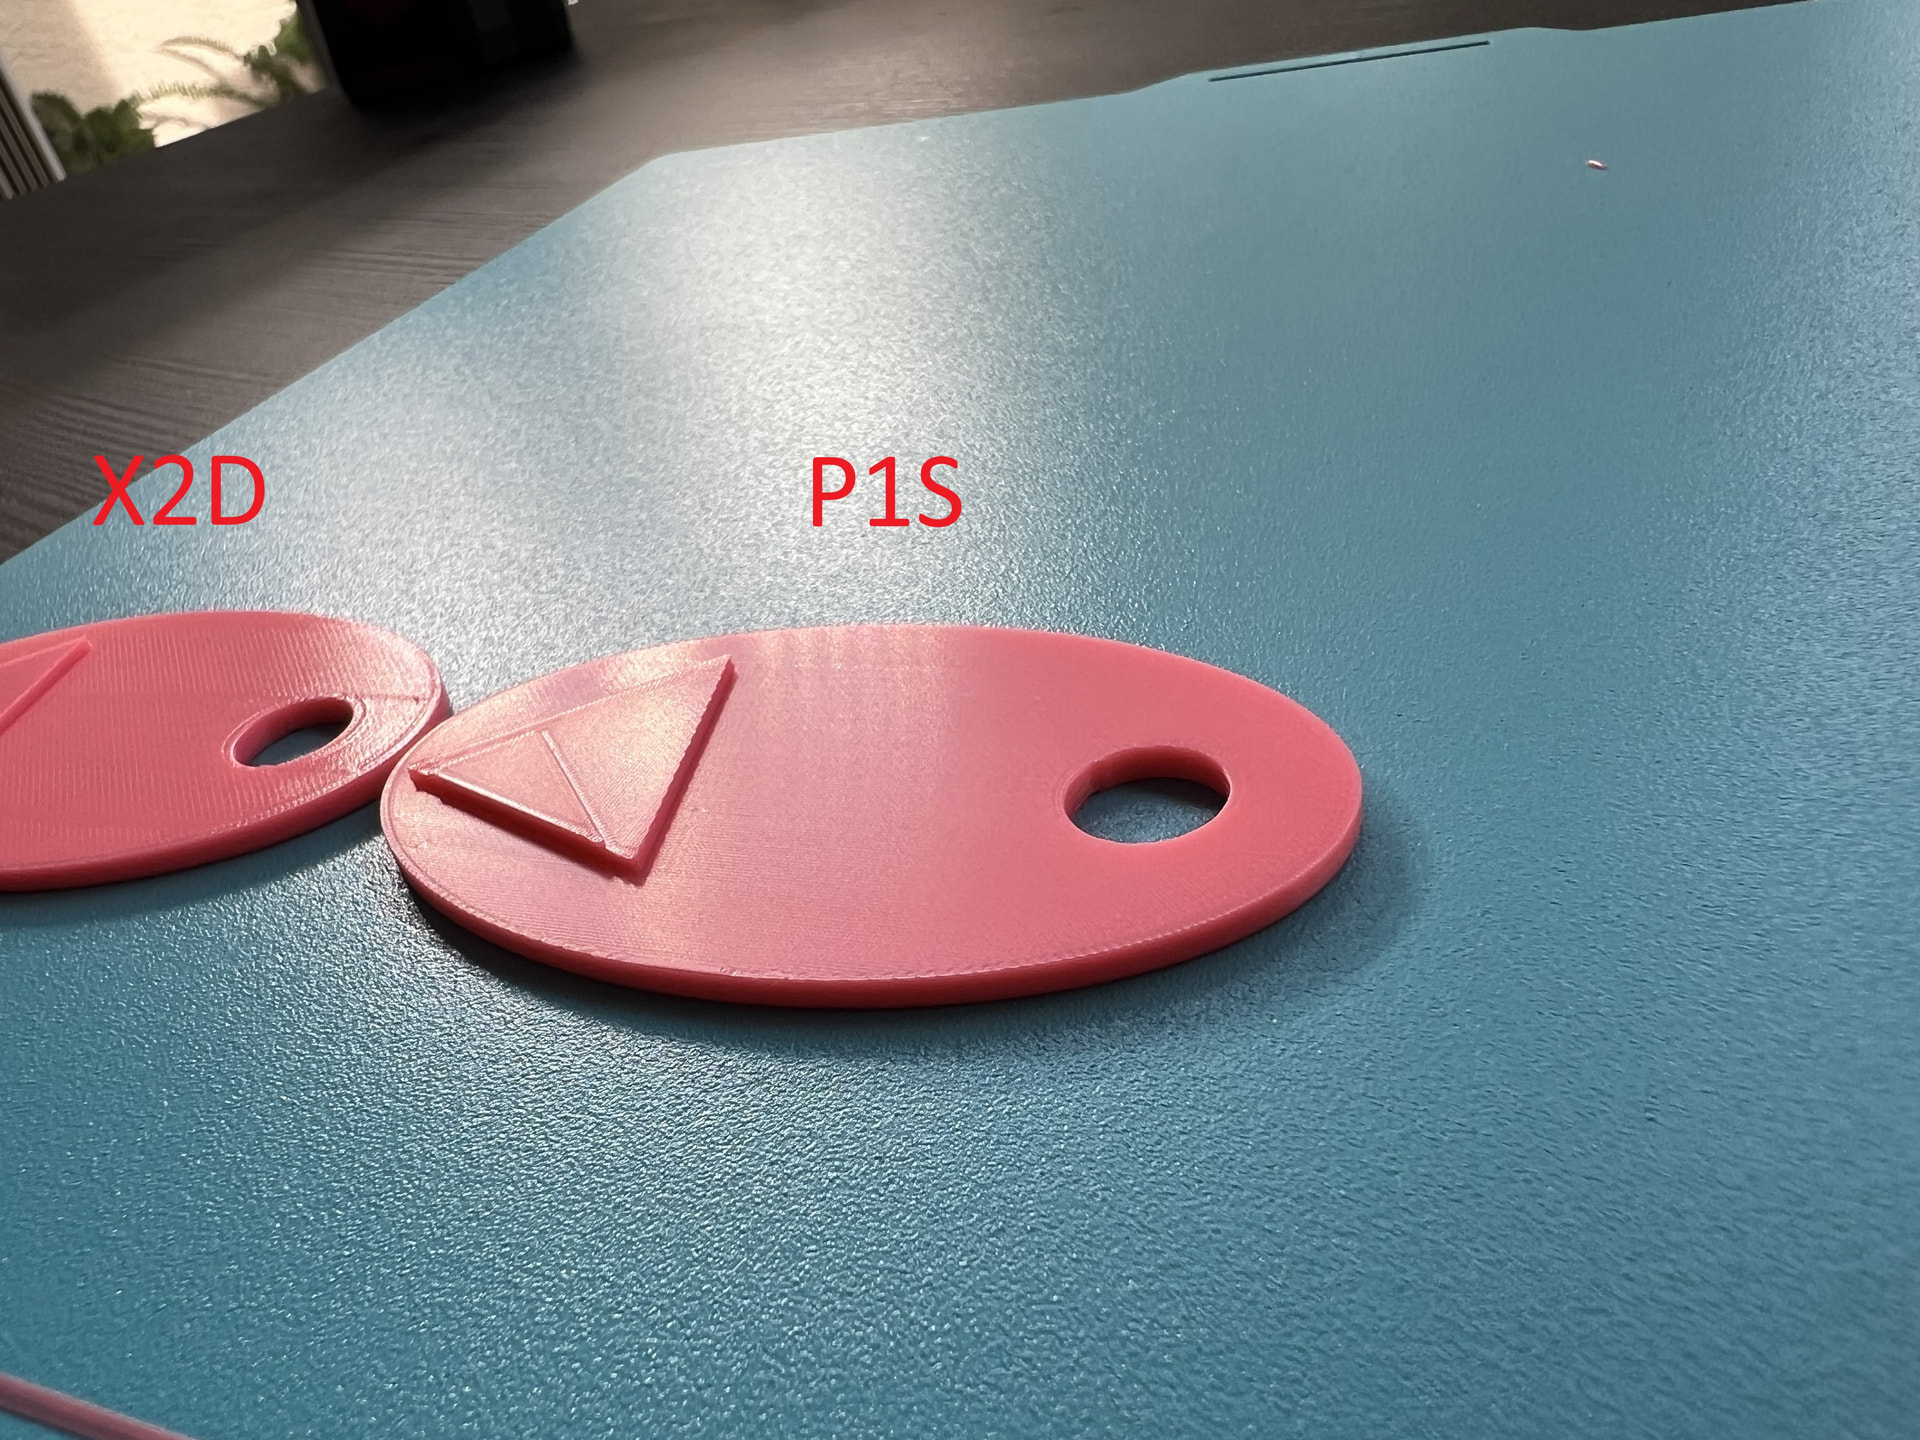
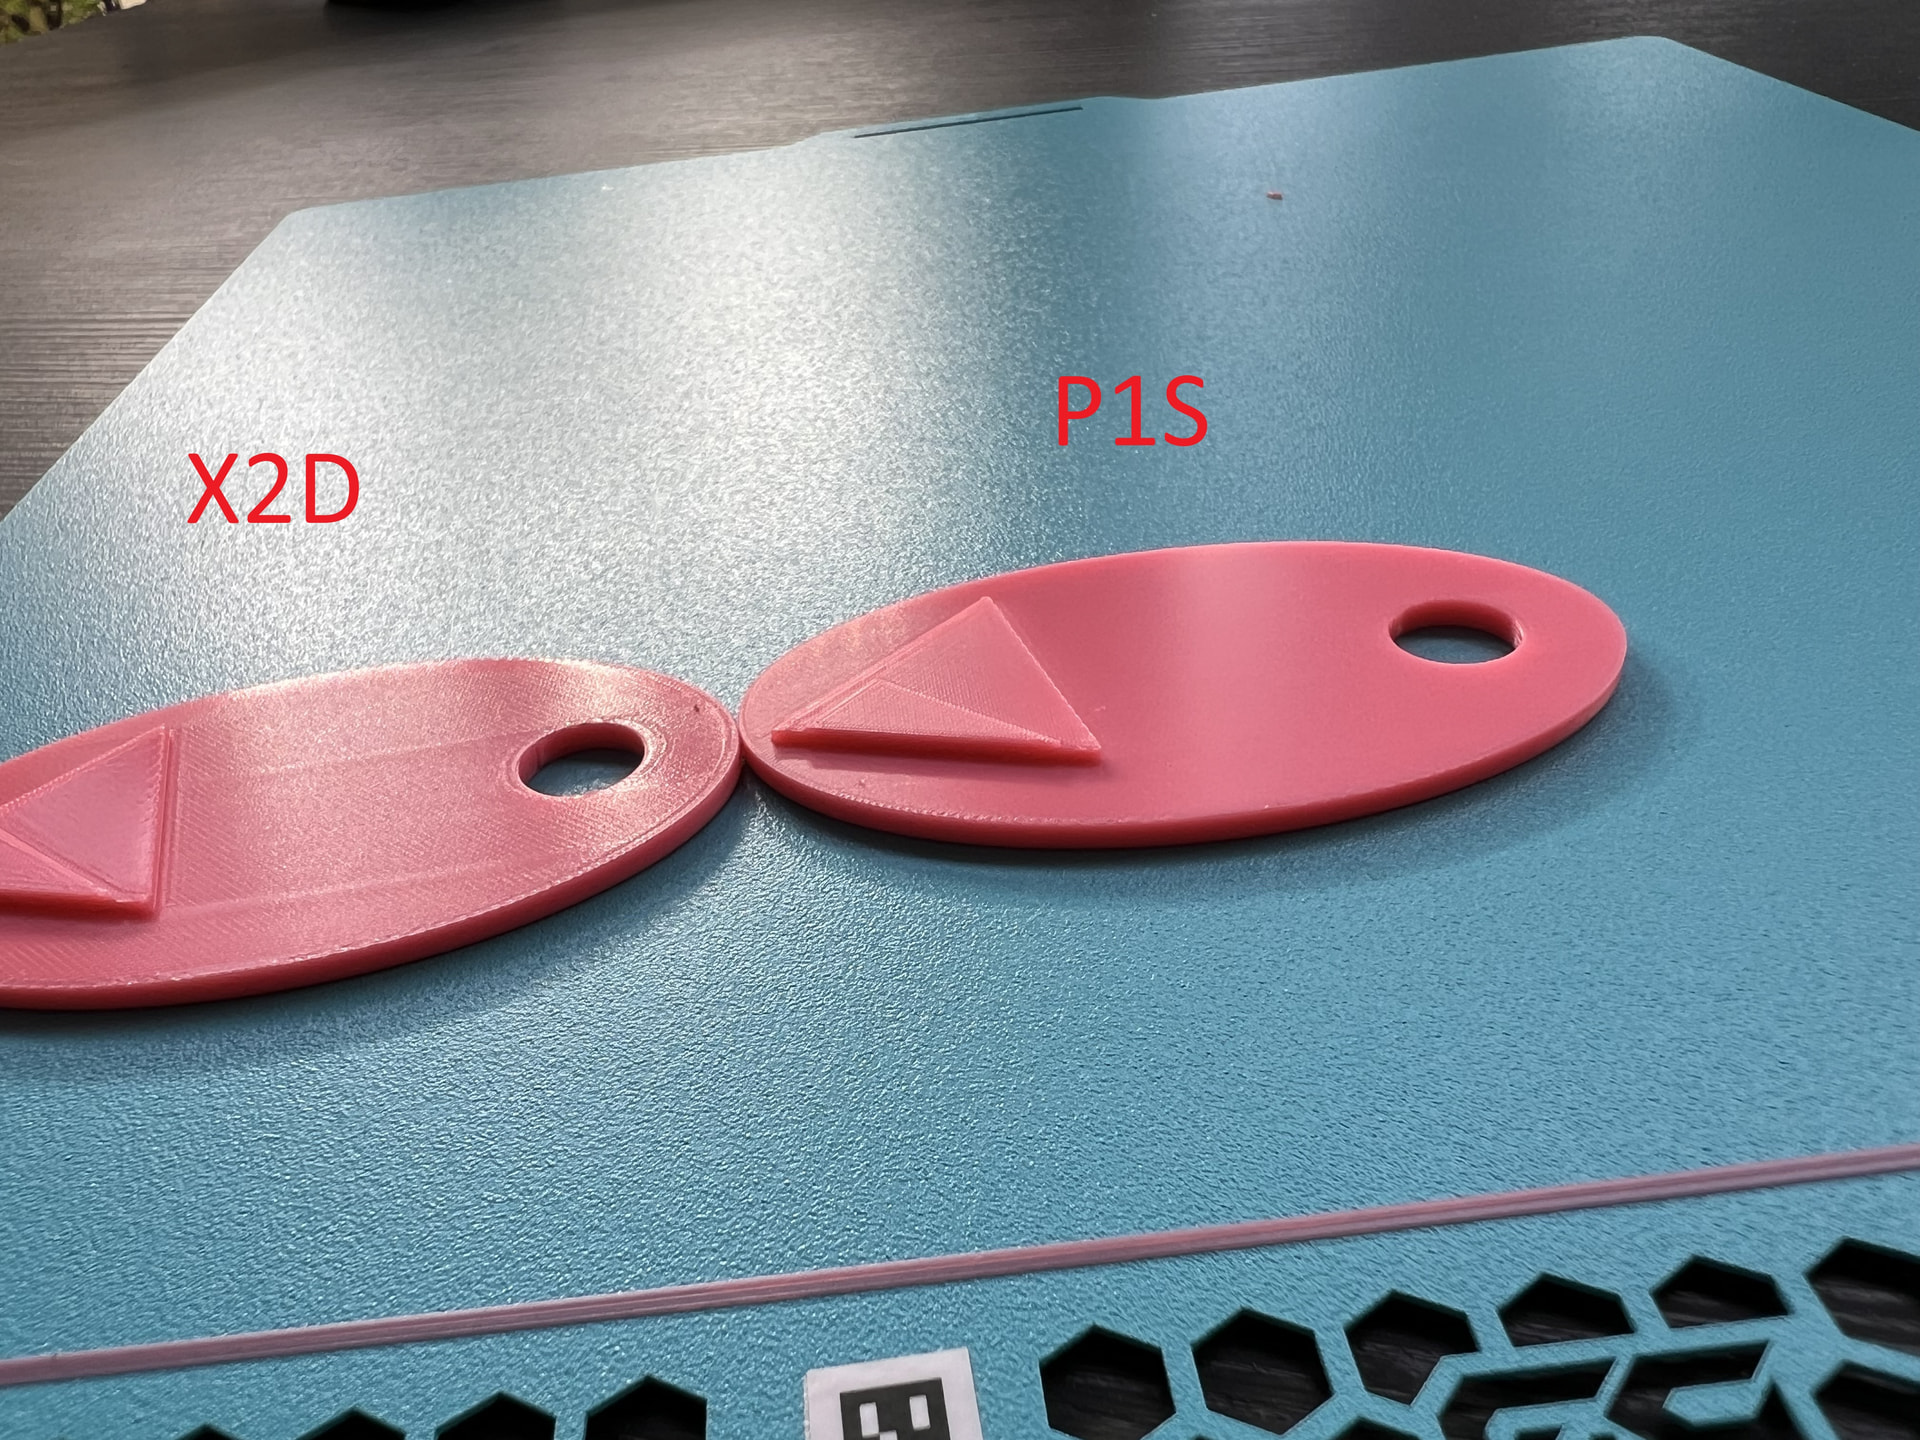
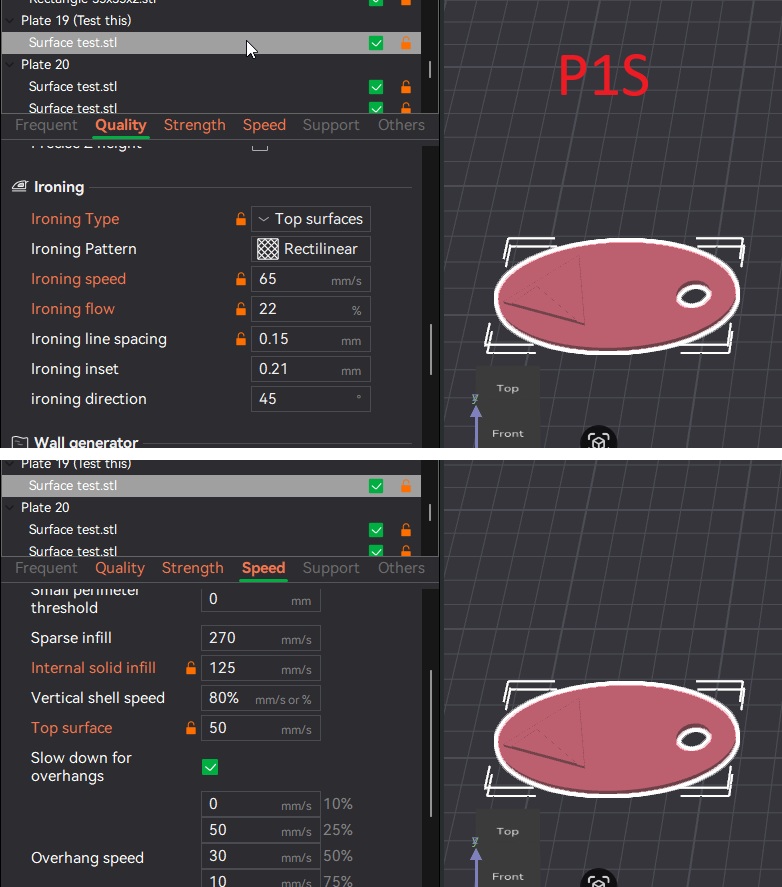
I’m in the middle of trying to dial in X2D settings for this, but I ran this part on my P1S with my normal ironing settings and it looks fantastic on the very first try. It’s very difficult to show this in pictures, but the P1S print is a smooth mirror finish and came out perfectly. I’ve printed and ironed more complex features on my P1S and I’ve never had an issue with complex geometry before. So this side-by-side sanity check backs that up.
I’m attempting to try and dial it in on the X2D right now, but I’m very confident this issue of “complex geometry” is not a present problem on the P1S.
Edit: @JJ_Golmon Idk if it’s useful or helpful, but feel free to send these pics to Bambu on your ticket showing this part works and irons fine on the P1S.
Thank so much for your work
It looks perfect on your p1s ! Amazing job !
On your picture we can see “shadow line”/“cooling line” for x2d.
What is your protocol/method to find solutions on x2d ?
How did you calibrate your flow ? or did you use Bambu settings ?
Thank you so much for your work ?
I send pictures to support
So I had attempted to figure this out on my own slowly tweaking the profile I used on my P1S (flow rate, speed, top layer, line spacing, etc). And that just ended up with me wasting a bunch of time and filament.
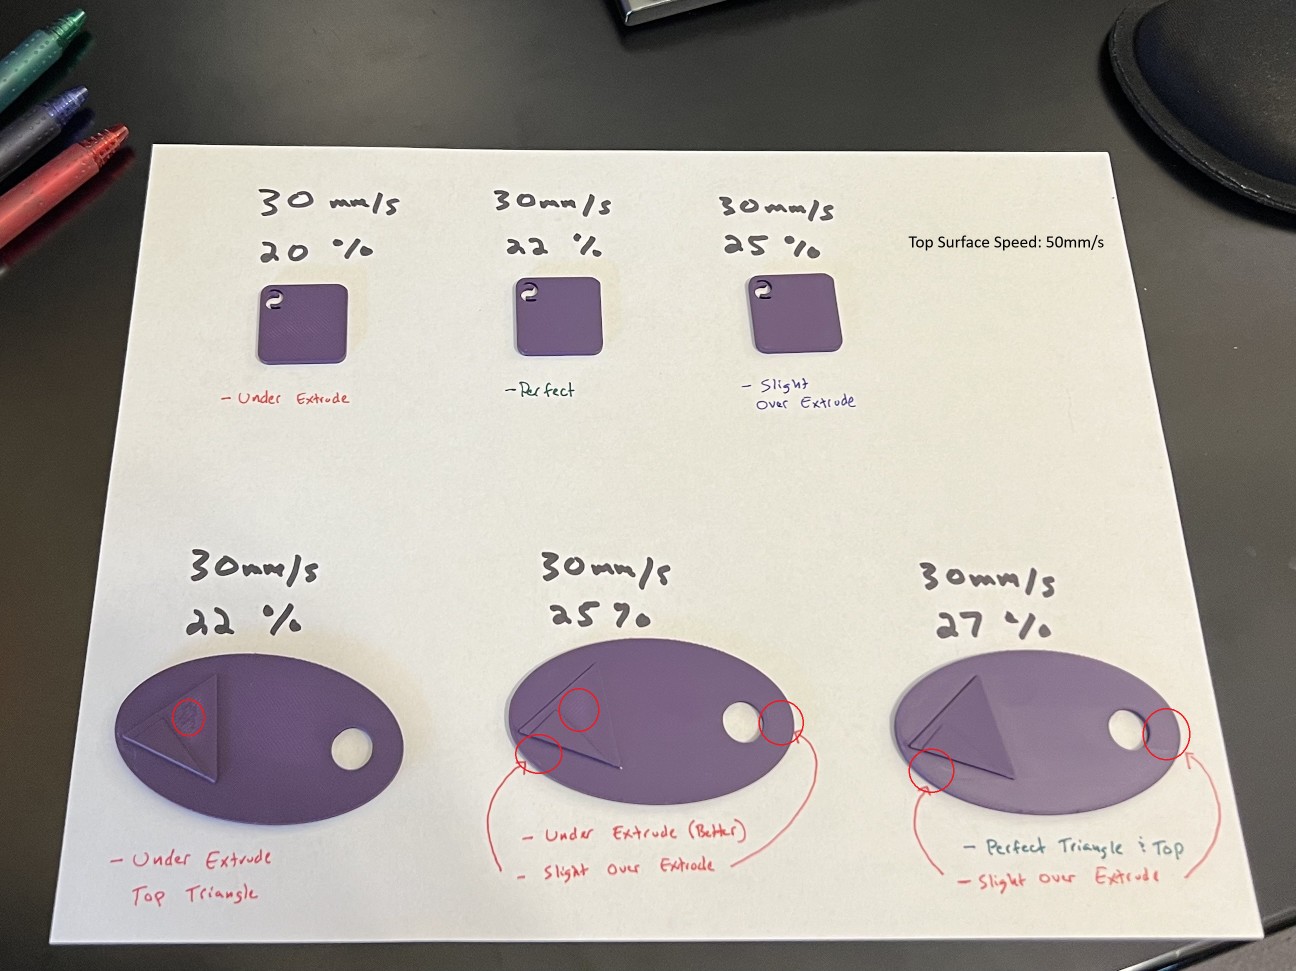
So I started fresh with a very broad ironing calibration model, my sample filament swatches, and then your complex model:
I’m trying to figure out where to go from here. The simple swatch and your complex part aren’t really in agreement here. So, so far for me the best result is a combination of the swatch and complex model:
Top Surface Speed: 50mm/s
Ironing Speed: 30mm/s
Ironing Flow Rate: 26%
Everything else Bambu Profile default
This doesn’t even get me to the same ironing level that I had on my P1S, but it’s at least the best I’ve been able to get to thus far. So I guess for now, until there’s an update from Bambu, that’s what I’m going to use.
Here’s an image of some of the more meaningful tests and results. I also have another handful of filament swatches and complex models not shown in this picture that was me tweaking a few other things to see if it made a difference or was reproducible if I did the same test a second time (it always was).