When asking for help, please provide as much information as possible about your inquiry.
This will help everyone to better understand your problem, and provide you with the best solution.
- Detailed description of the problem
- Printer model used
- Slicer settings used
- Type of filament used
- Photos that clearly show the problem
- .3mf file (if the file can be shared)
- Any potentially useful information that is related to the problem
Hello!
Been printing with Bambu P1S’s for about a year now and it has been a while since a problem popped up that is giving me trouble.
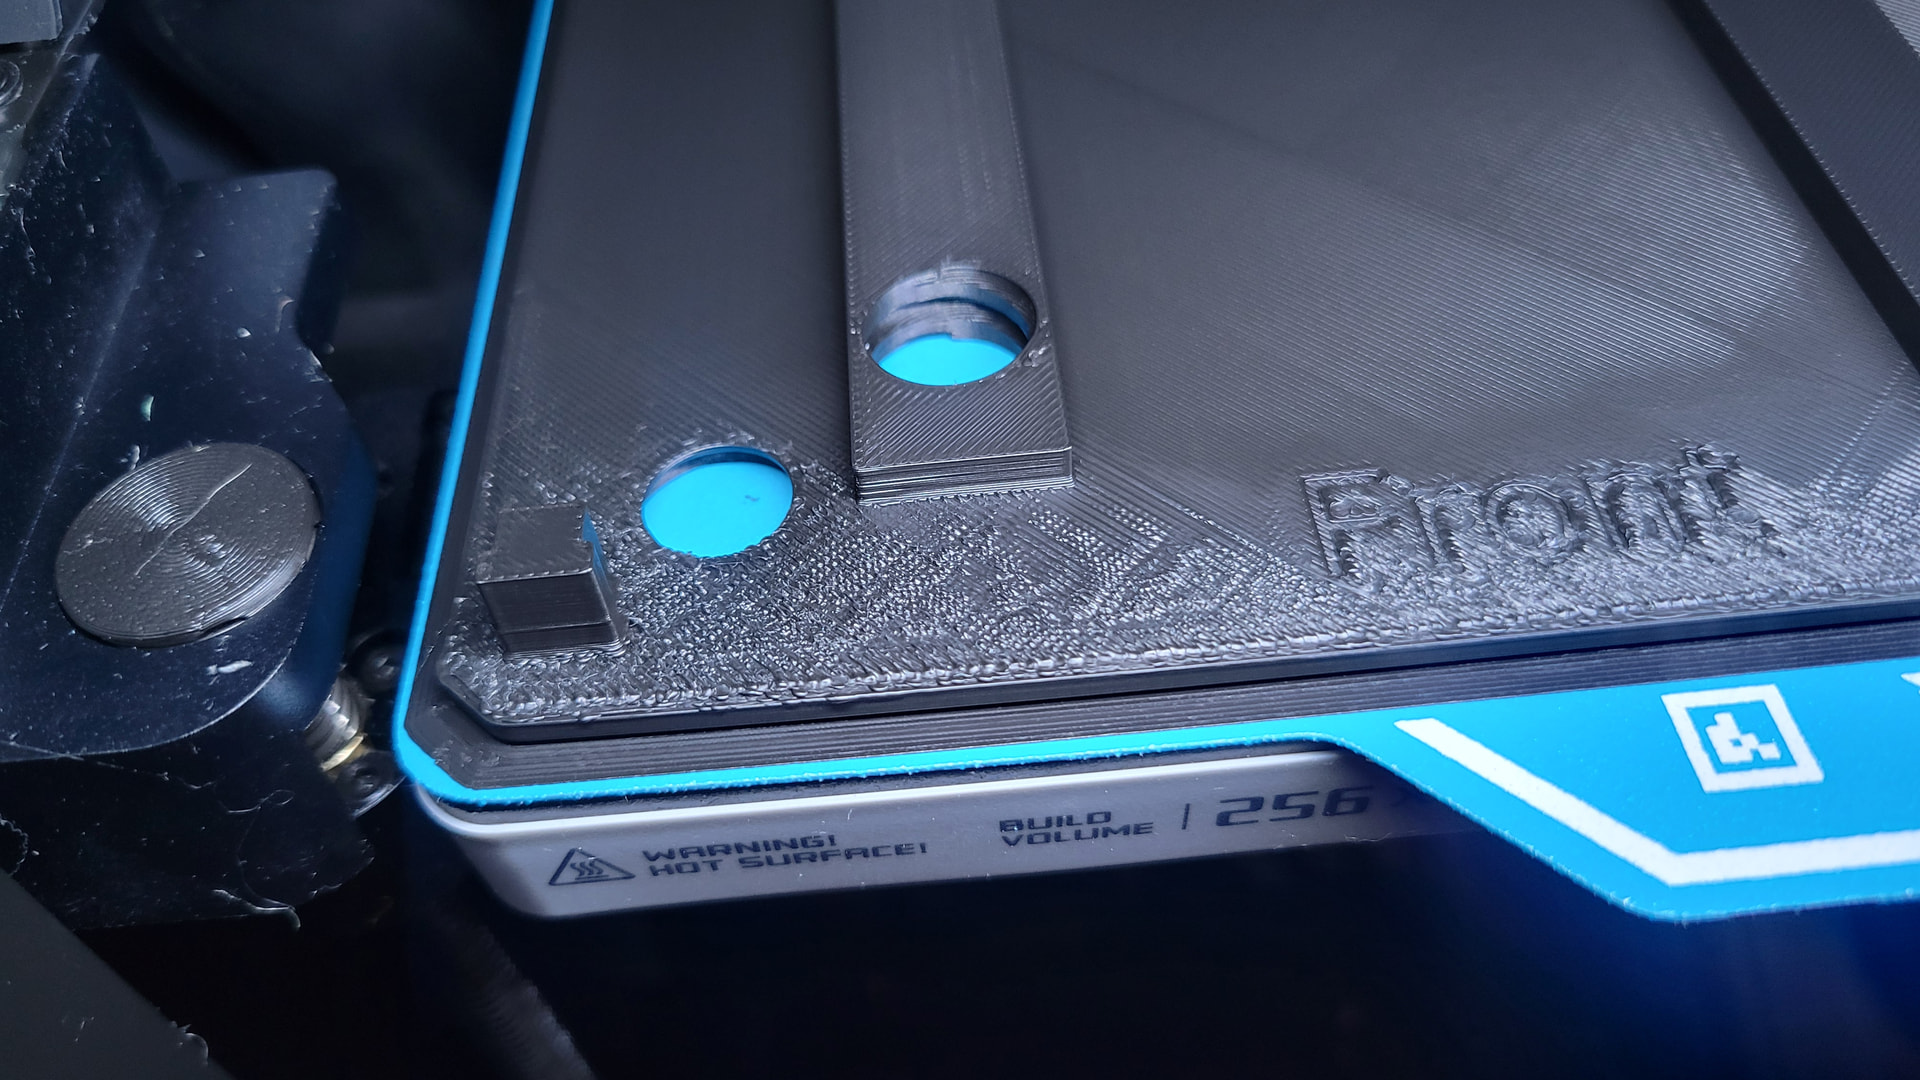
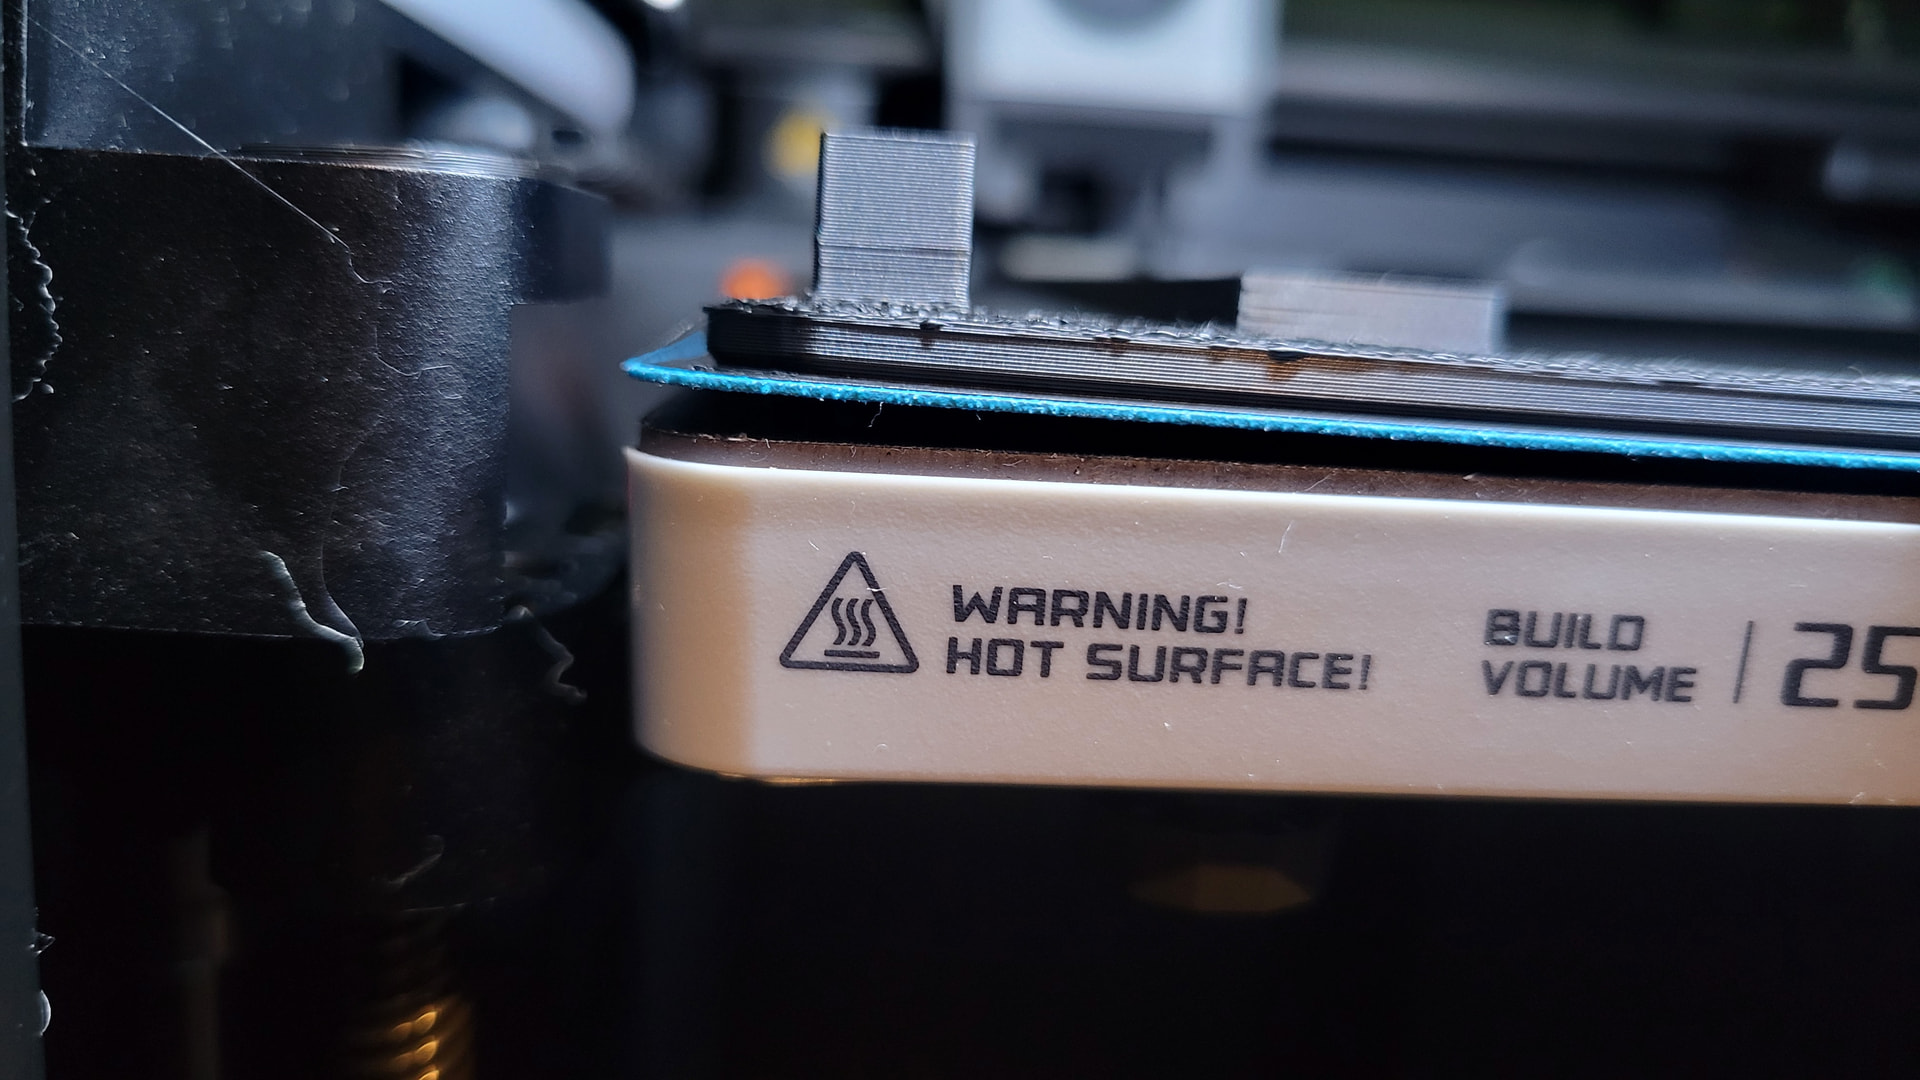
Large PLA prints (lids/bottoms for a Gachapop machine) are warping/pulling up on the corners to the point of making the print unusable.
It isn’t an adhesion problem as it is pulling up so much the plate is actually being pulled up from the bed while the print remains completely attached to the plate.
I can’t rotate/move the print at all due to the overall footprint of it (nowhere to move/rotate it to).
I have zero issues printing anything else in PLA, spent my year of doing this working out settings and what not to get everything working great.
I use cool plates (both Biqu Frostbite and Darkmoon), first layer temp is ~55-60, after that it is set to 1 and the ambient temp stays around 32-34, all first layer speed is set to 25, AUX fan is set to 5%, part fan 100%, unsure of chamber fan speeds, first layer print temp is 220 then 215 after.
About to try one of the parts with the bed temp staying at 60 the entire print as I think that is the last thing I can try, figured I’d post here in the meantime for advice and other’s experience.
Since the warping is due to too fast cooling (shouldn’t be my issue) and temperature differences in the existing printed part and filament being printing I’m thinking the bed being only ~32 instead of 55-60 is causing too much of a temperature difference and the warping.
Oh, I generally only use Bambu filament.
Thanks!
Do you dry your filament prior to these large prints? What are you doing to clean your build plates?
Filament is dried and stored sealed w/ desiccant prior to use.
There is zero lifting of the print from the build plate, it adheres so well it actually pulls the build plate up from the bed in the corners, but I clean Biqu plates with soap and water (they say no alcohol), Darkmoon I follow their instructions and only use water.
Interesting.
Would you mind posting one of your 3mf files? May be a settings issue.
Didn’t know you could post 3mf files o_o
Which settings could cause warping outside of filament settings?
This reminds me of an issue about a year ago. In the end, the user managed to get a usable print but warping could not be fully avoided despite using build plate clamps to keep the edges down. But physics being physics, instead of a u-shape, warping and clamps gave an m-shaped bottom.
Key to warping is usually to go for the root-cause(s):
- Filament dried specifically ahead of the print (It does not matter if it was kept in a dry environment as you don’t want to do this after having tried everything else. Easier to be sure on a complex print like this)
- A warm chamber (I try to keep my X1 at just below 35°C for PLA. Above that, heat creep is a hughe risk)
- Less obvious: Lower layer height: This injects less heat into a given layer => More even cool down
- Even less obvious: Slower speed: This too injects less heat into the layer => More even cool down
- If desparate: Consider Carbon filled filament to distribute the heat more evenly
 &

Hello
I have experienced this quite a bit and no matter what settings I adjust I learned the best solution was to alter the model.
Slant 3D on you tube talks about all kinds of problems including large prints. https://youtube.com/@slant3d?si=5YHZD_7y22vHIe0-
This video should be the one talking about why it happens. https://youtu.be/iPZoDltS30A?si=olk44Ck-IFcUsu5F
It has to do with the cooling taking place between the out walls and infill and as the height increases it all starts to pull inward.
I have started to design relief lines in my models so it’s not a fully flat surface on the plate. If you manage to find his video he has more complex solutions, but they would require building in during design. I bring up the relief lines since you are trying to print someone else’s model, and could probably make them in the slicer by adding small negative rectangles about 0.4mm wide by 0.6mm tall for the whole width of the bottom surface. I would place them every 20mm or so.
If you’ve tried everything else it’s worth a shot! Good luck.
It’s entirely dependent on part geometry.
When thinking of printed sections in general, you have “length” and you have “thickness”. Length is simply how long a straight section is, and thickness is either how wide (how many walls) it has, or how tall it is.
Think of length as “how far it wants to shrink” (shrink is always expressed as a % factor) and think of thickness as “how much it wants to shrink”.
So you could have a very short section with minimal walls and height, and have zero noticeable shrinkage.
Longer runs with single walls and minimum height? Minimal shrinkage. Same goes with thicker sections that aren’t very long.
Long runs with thicker sections though? That’s maximizing the amount the part wants to shrink, and how much force it generates due to the shrink.
For your parts, you could use shorter sides, or fewer walls, or make the sides of the parts much wider and use more infill and fewer walls, so the inner and outer walls are far apart.
You could deliberately seek out very low shrink % filaments (both type and mfg)
You could try to anneal them in an oven on a very flat surface to see if they “droop” into a flat state.
@EnoTheThracian has some excellent points and @JABO_Designs has a very good idea about control cuts in long walls to disrupt the shrink forces.
Upped the bed temp to 65 for the entire print and everything printed 100% perfectly. Made no other changes at all.