Yeah… that’s what i thought, but the pattern issue is present in almost all complex shapes, and as far as i know a lot of people printed that model on x2d without a problem 
why does overtime I use the carbon fiber pattern build plate on my A1 Mini does the print fail? I keep getting the blob of death every time. on Bambu studio I have it set on Smooth PEI Plate/High Temp Plate
There are a few things to keep in mind with the effect plates:
- They need to be cleaned much more frequently
- They need a temp increase of 5 to 10°C as per the little note on the shop page (increasing 1st layer nozzle temp by 5 to 10°C can also help)
- Occasionally, new plates need some “breaking in”. In my cases, I have had good success with just heating them on the heat bed for half an hour per side.
 &

Maybe this isn’t the place for this, but I can’t seem to rite a standalone first post. Bought an X2D, first 10 prints flawless, then one failed. Next one even did something where the plate came up too high and knocked the front cover of the nozzle container (?) print head (?) - sorry very new!
Now every single print fails. Have washed plate and recalibrated machine.
Help!
I am very new to printing, it is petg straight from ams pro2 to my h2c and its ■■■■■■■ up the print it is set on quality 20 in bambulab and ironing on what could be the issue? You can see Some spots perfect and then like top corner really bad and Some other parts aswell, then the middle is as smooth as ice..

Welcome to the forum.
The top corner looks like an adhesion issue which the majority of the time is related to oils on your build plate. Clean it with dish soap and hot water.
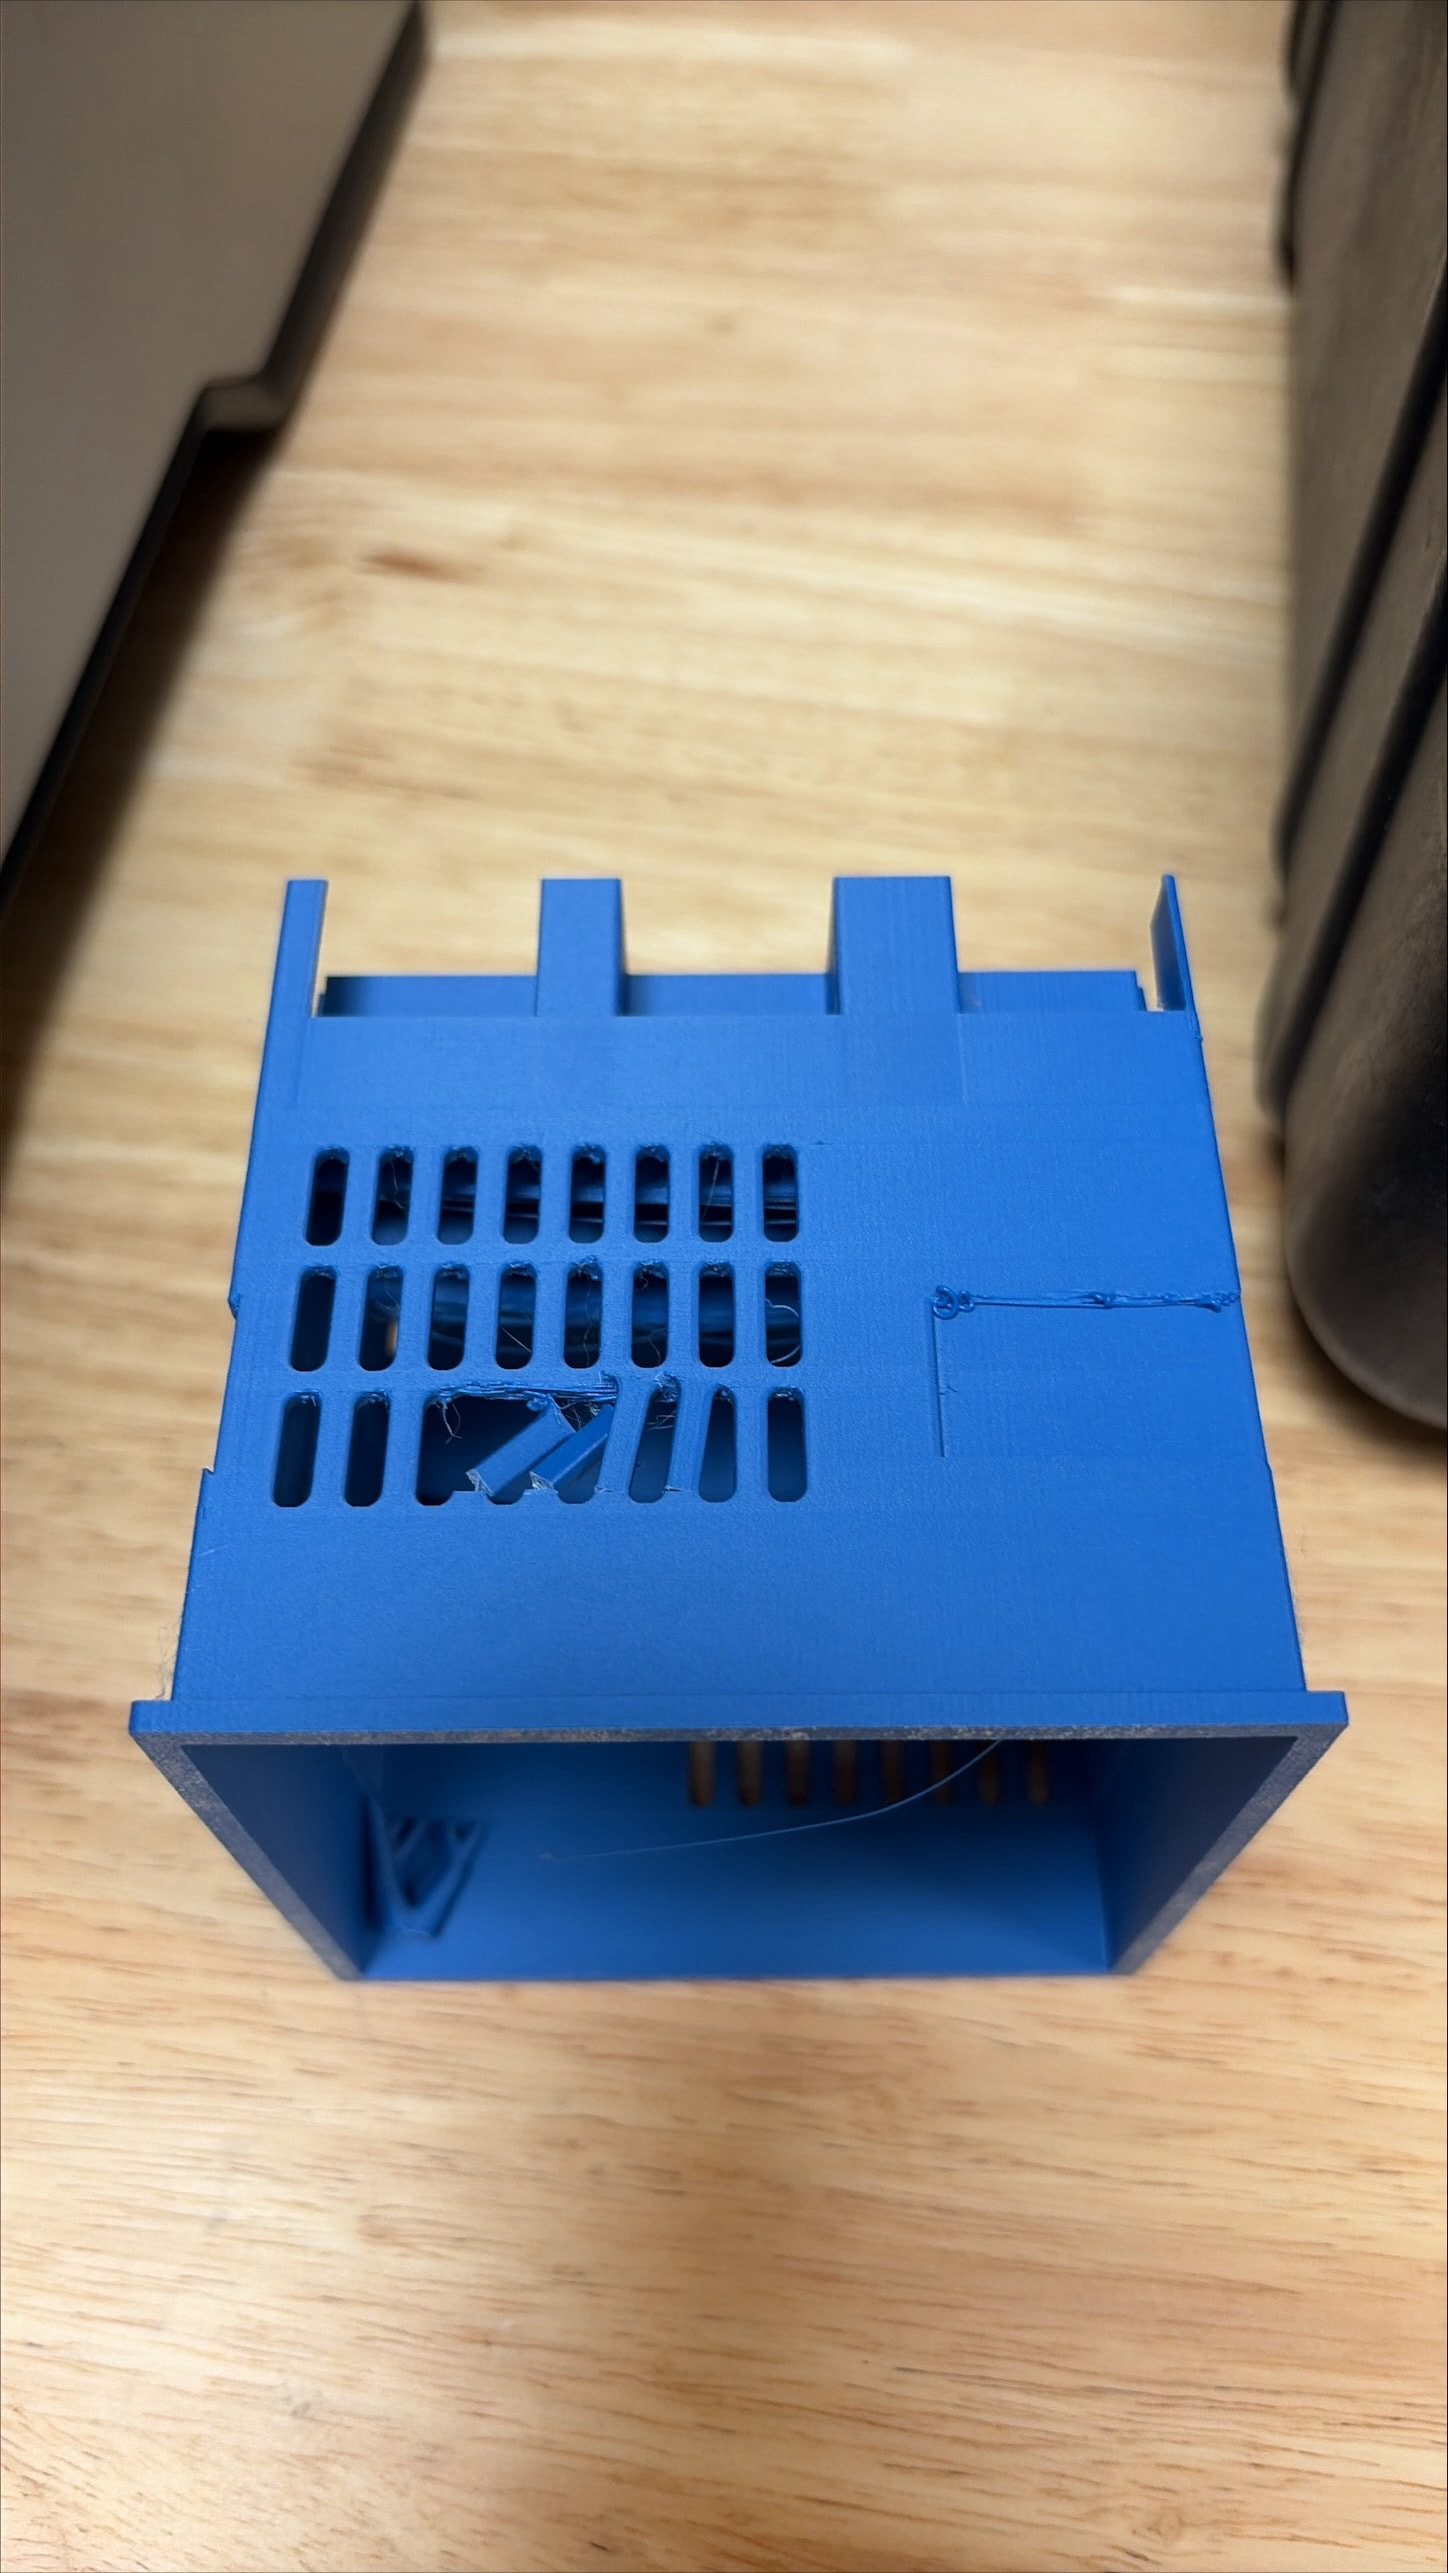
Printed a case from PLA matte on a H2D which requires air vents on each side. It seems has failed on 4 ridges. The vents on all others sides are in good condition.
I printed with TPU for the print before it so the top cover was still removed, and I have noticed a lot of stringing on the print. First thing I’ll do is dry the PLA and try to print again. If anyone has an idea what caused this please let me know.
I am 3D printing some bathroom trays that feature an internal recess. However, the external walls—specifically at the same height as the recessed surface—are being printed with a greater thickness (in Bambu Studio, they appear straight along the Z-axis, as they should be). I’ve tried various settings, but I haven’t been able to get the external wall to come out smooth. Does anyone know what might be happening?
Without seeing the part in question I can only offer this suggestion. Try using a fillet for the transition at the recess spot. The issue you are describing is usually caused by shrinkage of the material as it cools. Increasing the wall count/thickness can also help.
I have tried everything. I’ve had the x1c for a year now and I’m still having issues. I’ve cleaned plate, ive adjusted settings EVERYWHERE. I’ve adjsuted temps, tried printing with the door open, tried different filaments. I’ve made sure my files are good and repaired. I’m at a dead end and i need prototypes printed within 2 weeks. Please help. My issues are, bad bed adhesion , stringing, supports leaving my prints looking disgusting. i’m just beyond frustrated..
I’m using x1c with anycubic pla+ and I’m printing articulated action figures in parts. I even do one piece at a time. No matter how i position the hand, i get issues. I’ve tried painting supports and all other support settings and again, same issues. I’d post pic but it’s not letting me.
Fingerprints. Wash the plate.
Thank you… i think that is a hull line…
Hi Everyone,
I have an Issue with a Filament, i guess. I’m really new to 3D Printing and don’t know much about the settings and troubleshooting and such.
I tried to print something out with PLA Translucent in Blue - the prints filed everytime but one. It’s either clumping or the nozel somehow knocks the print/part of it off the plate. The knocking off happened a couple of times eith other filaments, but with this one it’s basically all the time… I also have done some prints with PLA translucent pink and didn’t have any issues.
Am I doing something wrong? Can i do something about it?
thanks
I’m having the same problem with PETG when I’m using PVA support - PVA filament breaks at the hot end entrance, preventing the PETG from loading. The printer doesn’t notice this and continues printing as if nothing is wrong.