I am having issues with my latest model I created and am printing. So it seems that my print is experiencing what I have found online to be variable cross-section layer lines. But I want to get a second opnion and get some tips on how to reduce this via slicing settings in bambu studio.
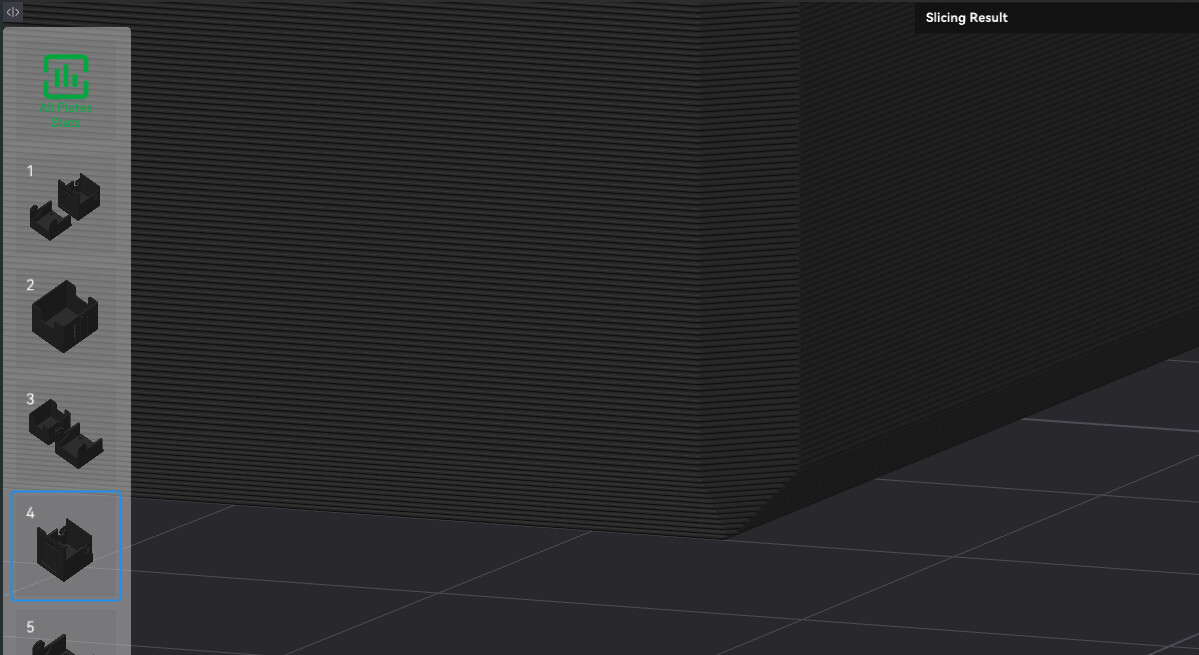
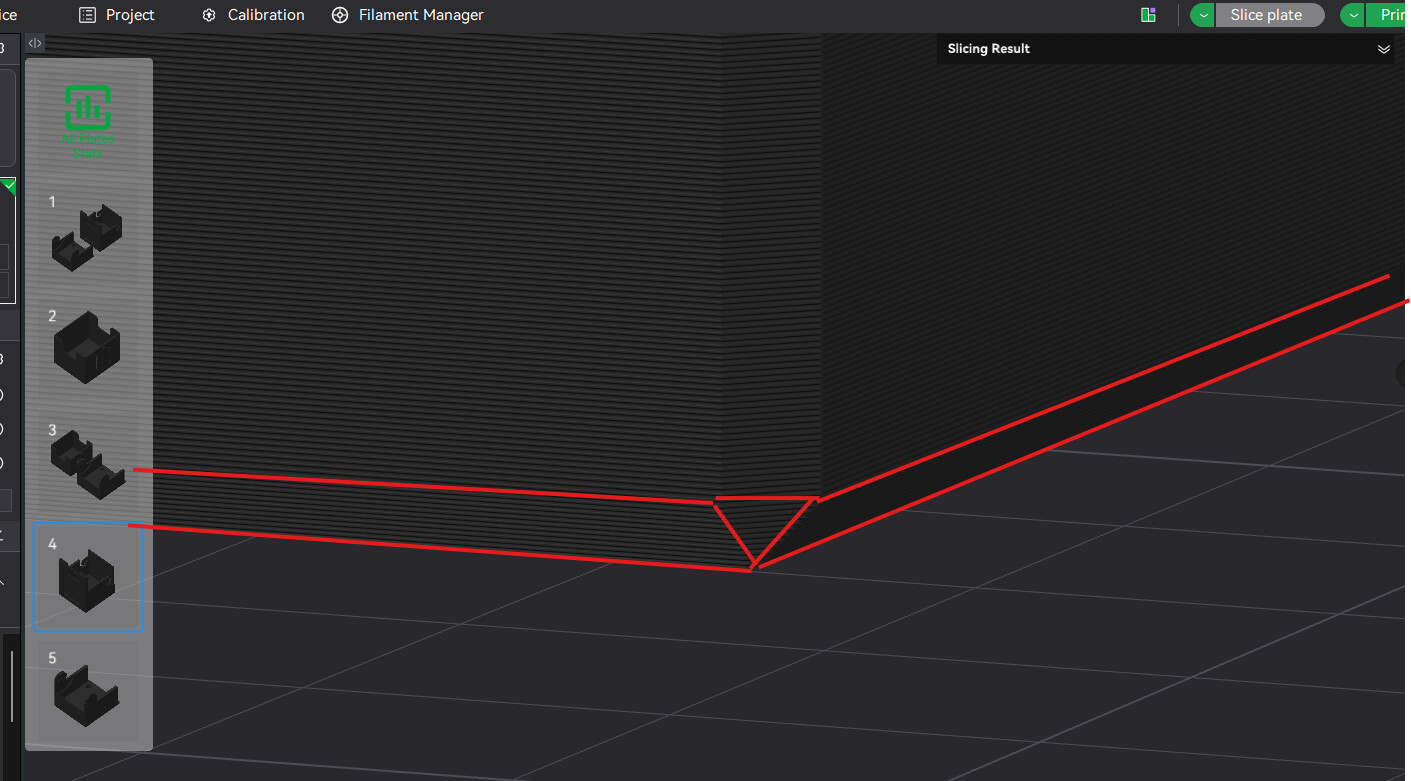
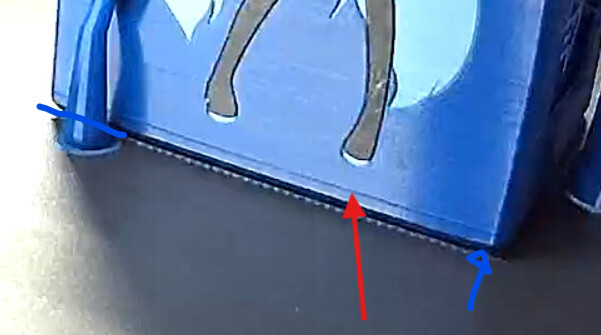
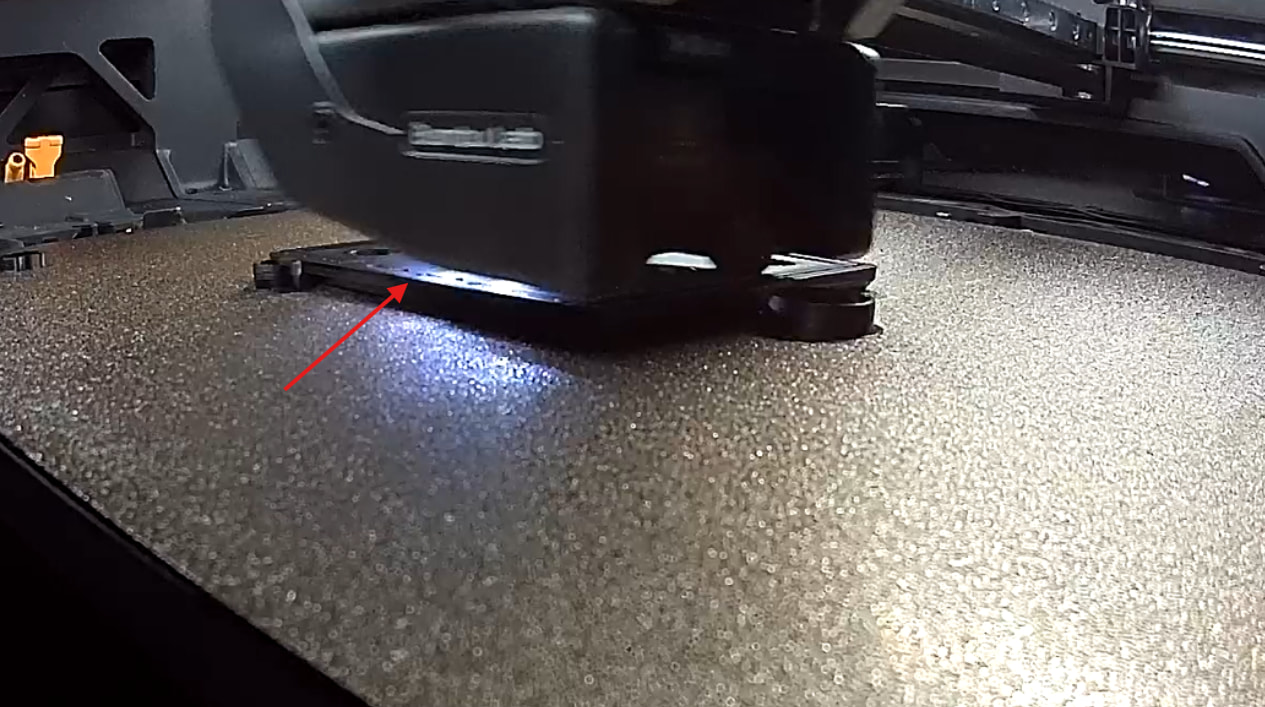
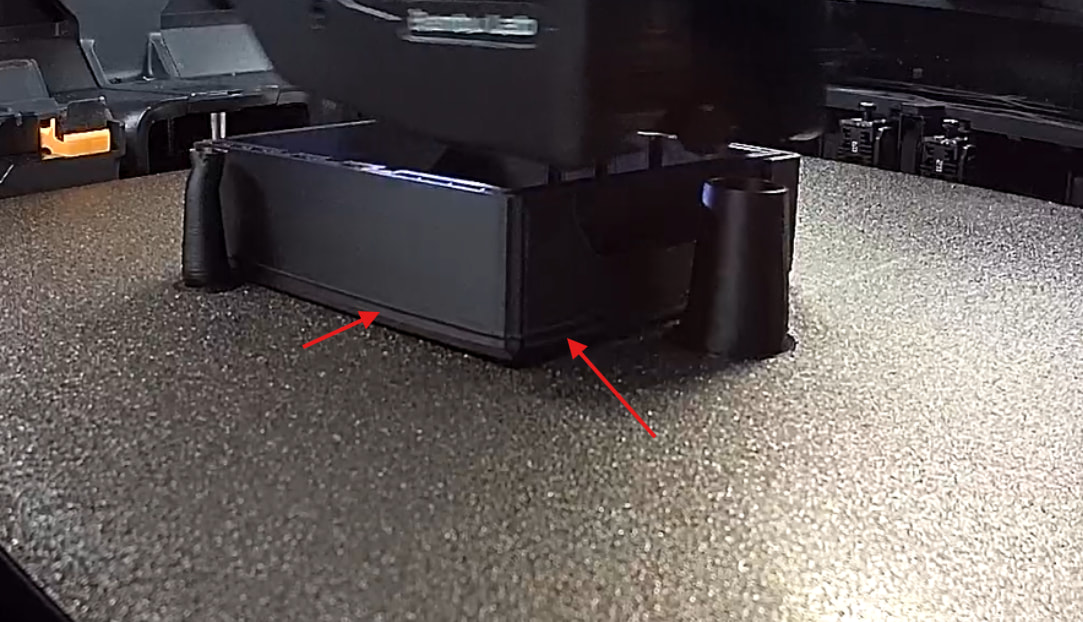
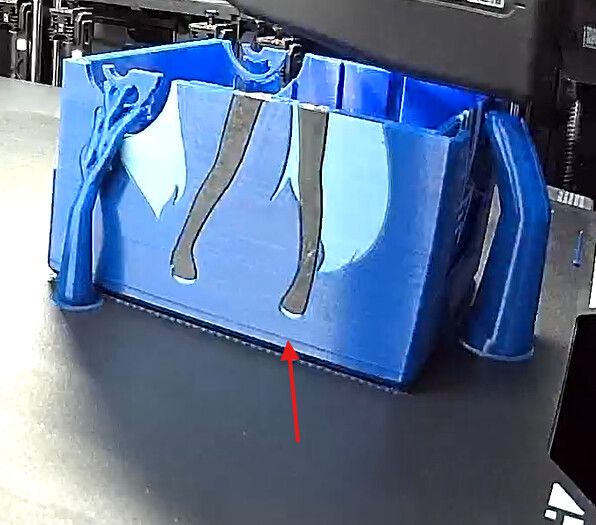
As you can see in the pictures there is a protrusion that seems to always seems to show up when it goes from flat to printing the walls of the “box”. The only thing that makes me confused if its a cross section layer line, is that the protusion is coming out rather than a line/hole going inwards which is what happens with shrinkage. Or at least thats what I thought. Even used a brim to make sure it wasnt the model slipping or warping.
Any help would be appreciated.
Printer - H2C
Using Bambu and Overture PLA, get this issue
To me, it looks like a classic hull line where internal features change rapidly. It’ll show up quite prominently in the layer time preview.
Countering it is quite tricky.
Print related help is to use very well dried filament, print slow and with a warm chamber.
However, to really effectively remove that effect, design changes are usually needed.
Smooth out vertical geometry by applying internal chamfers or fillets
Break up the strain paths from large internal surfaces by adding, for example, edge trenches on inner surfaces
&
PS: From the pic’s, it lools like your print is also experiencing warping. Well dried filament, warmish chamber (depending on filament) already help a lot. For difficult cases, slowing down and/or lowering layer height can again make a big difference.
In at least the first picture, your part is lifting in the corners. You have substantial material shrinkage and the forces are overcoming the bed adhesion and causing the corners to lift.
Make sure your filament is very well dried and your print bed is very clean - dish soap, hot water, scrub with a nylon brush and dry with paper towel afterward.
I discussed minimizing shrinkage extensively in this thread:
(Sorry for bad pics, will be at printer and have actual model and not just gcode preview later in the day)
I always make sure my print bed is clean. Always dawn dish soap and hot water srub the textured plate before each print, then wipe with a microfiber cloth. I probably do need to dry my filament again, it has been a hot minute. But the blue one was opened fresh and dried the day before.
I dont see the warping you are mentioning but I have not had many prints that had warping so subtly. What makes it hard to tell is that its not a straight cube but the sides and the corners are chamfered edges so the camera angle isnt the best. Im not currently home so I will take better pics later.
In the preview, I dont see the hull line unless my settings are set right to see it. First thought it was seam placement causing issues as well but changed it to the back to get the same results.
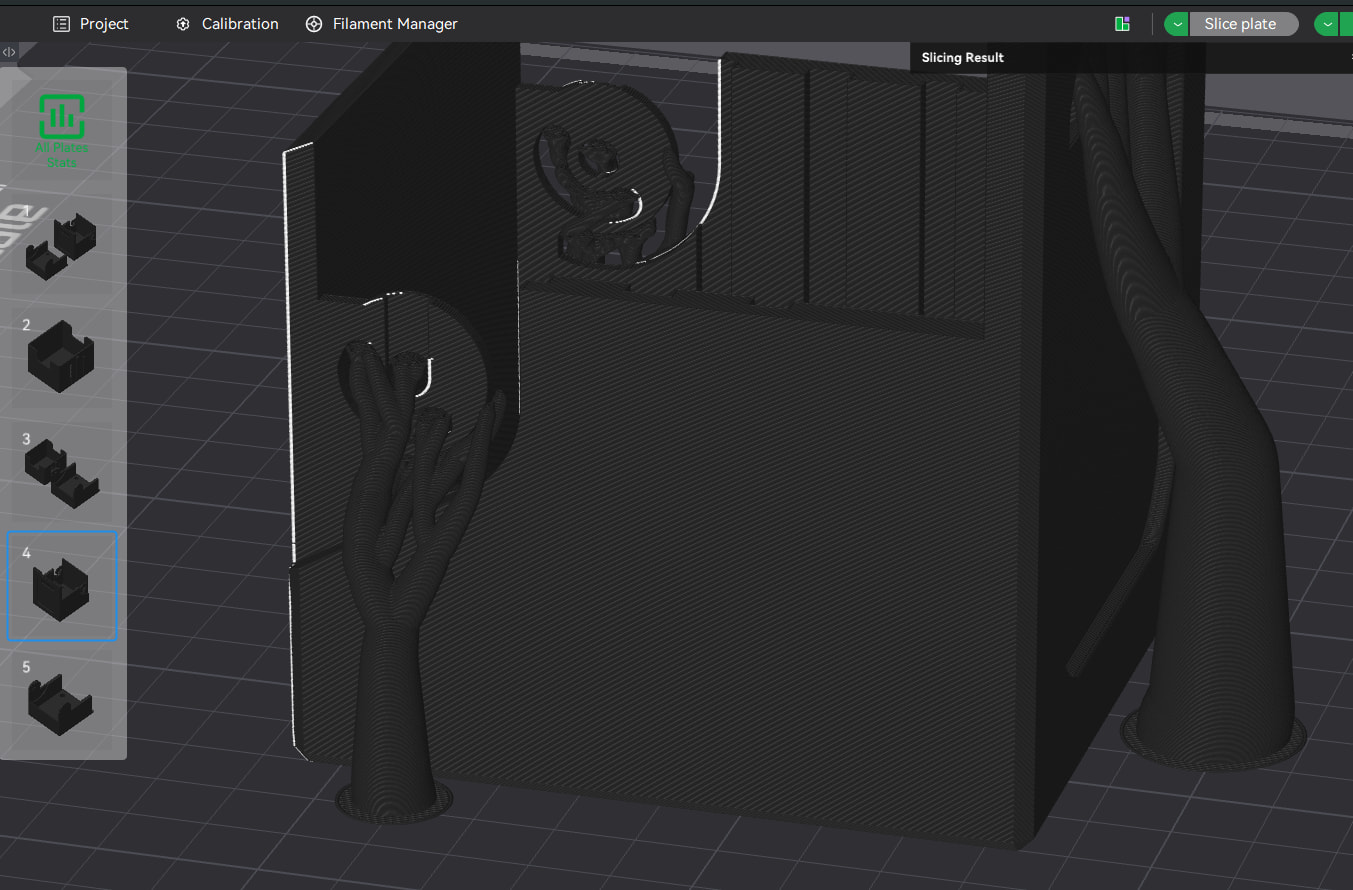
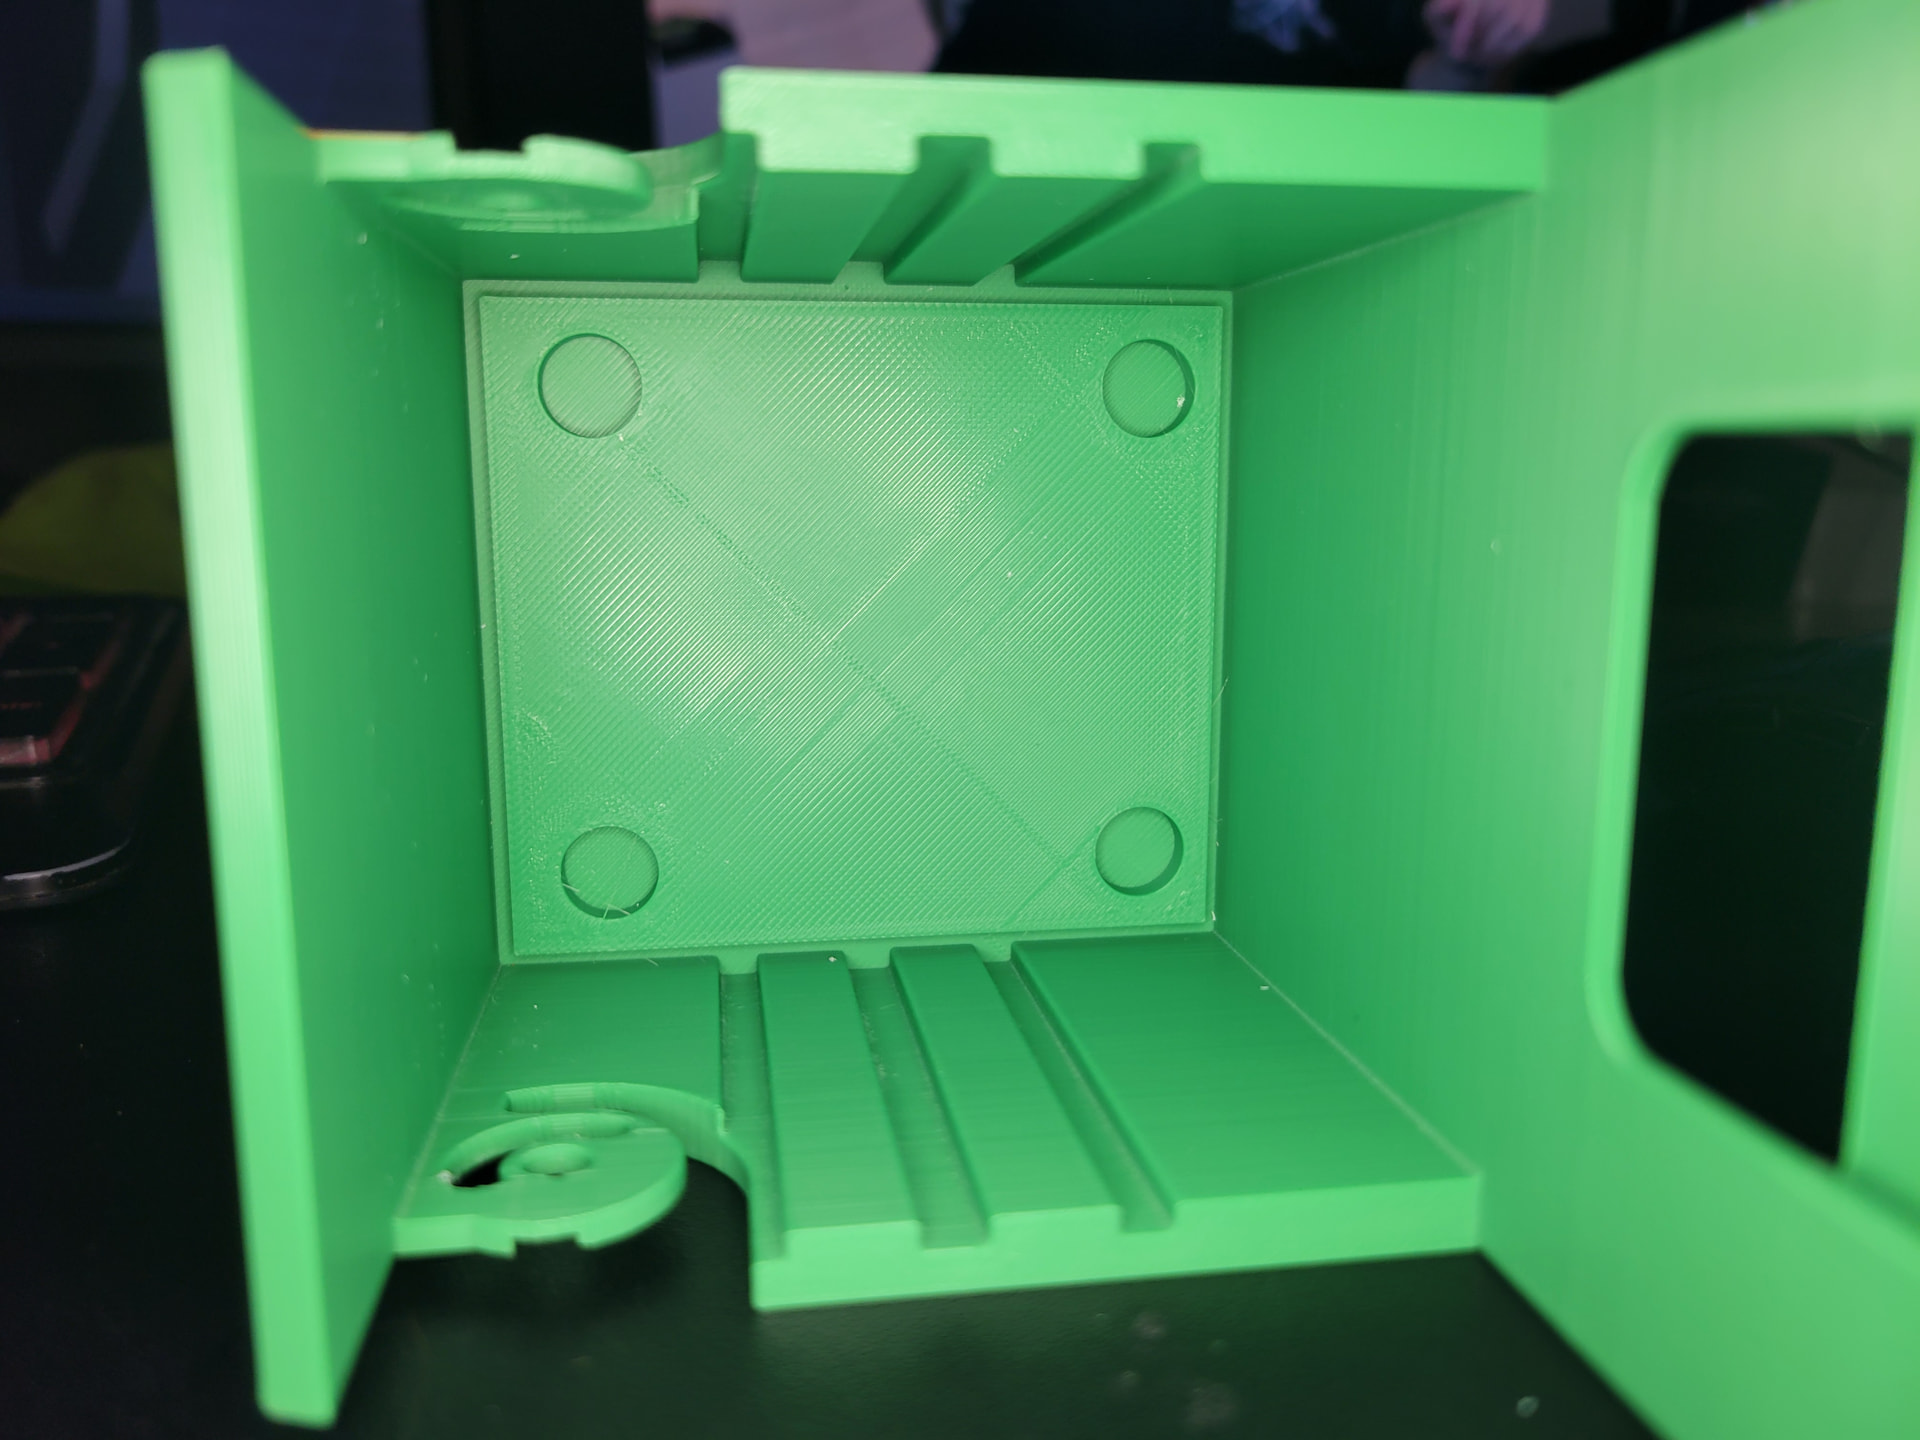
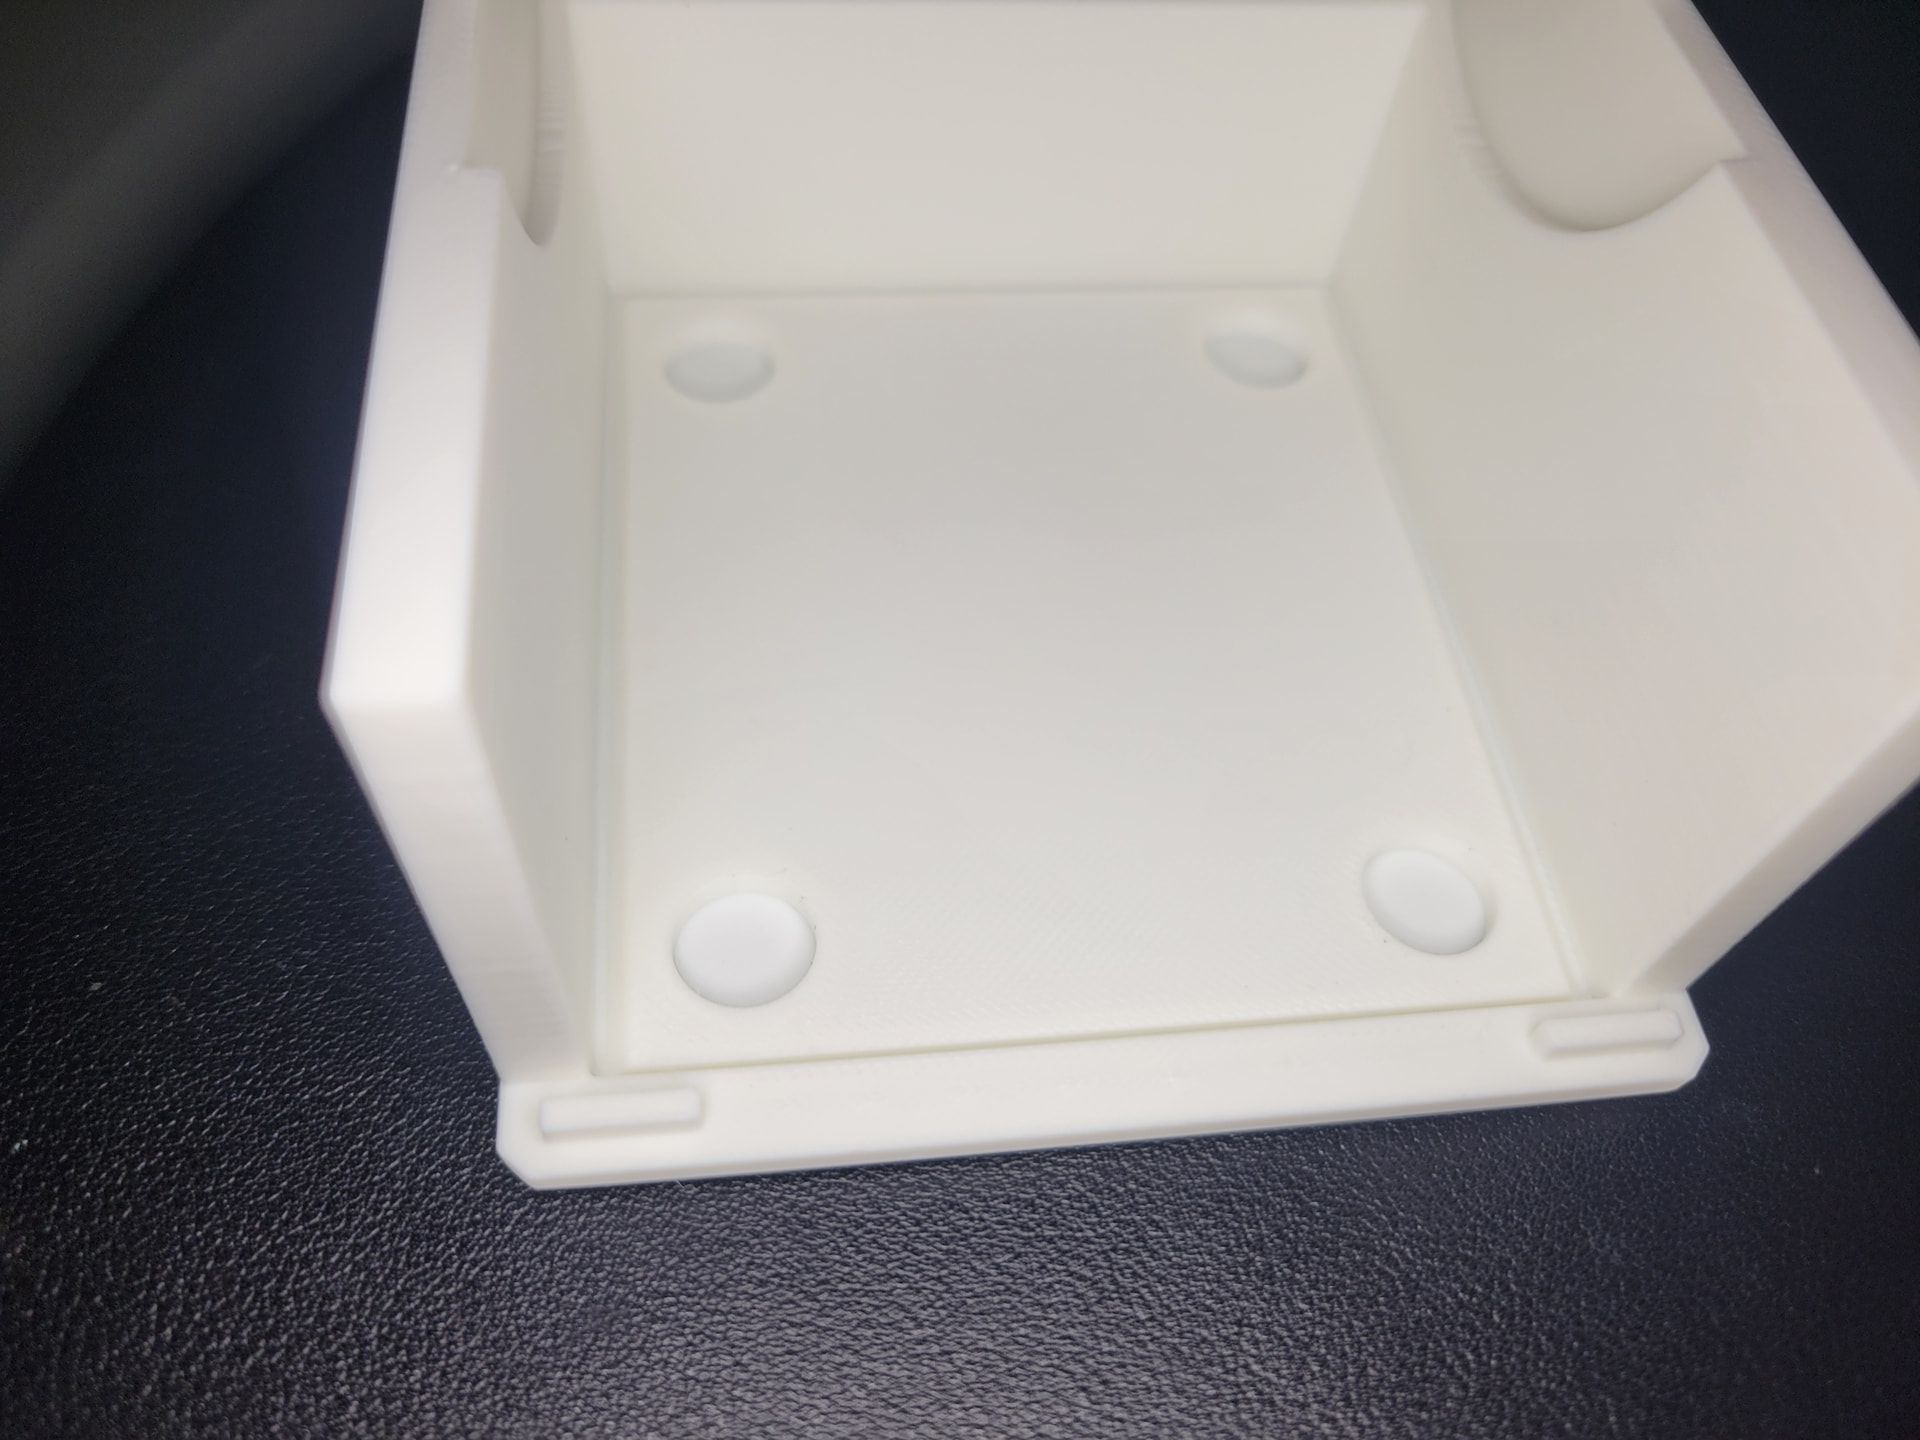
Then finally, this is the inside of the model. Are you saying add a chanfer on the inside so its not a 90 degree corner? Also how big of a chanfer do you think would fix this?
Regarding the chamfer, this is indeed the edge that I would recommend to put a chamfer on. I find it difficult to make recommendations as to the size though. Too small a chamfer will not change much but you may be constrained by the visible holes.
In addition, you could include a small (say 1-2mm) trench at the lower edge of the chamfer. That will “break” the strain path from the big inner upper surface to the outside of the box.
Regarding the warping, it looks quite apparent in the pic’s. But of course it may be a trick of the light.
To me, that indicates that there may still be too much moisture in the filament, the chamber temp is too low to make for an even cooling (my X1 likes anything up to 35°C for PLA while my H2C can do 40+°C without heat creep and a .4mm nozzle) and/or the print is being run too fast (layer height and speed) to avoid cooling effects.
Improving that will also help with (but probably not fully eliminate) the hull line.
Would you (or anyone else) be willing to elaborate on this? I think this is the first time I have seen anyone mention this regarding reducing the hull line issue and wouldn’t mind having better understanding of what this could mean! I think I have a decent guess from context and all, but if you have more information I would love to hear it.
One of the hardest things about learning online is gathering up some of these basic facts. Learning the terminology so you can ask the right questions is nearly impossible!
Apologies for the terminology. I am actually not certain, what the correct terminology would be
If you look at the link by @CarbonForge above, you’ll see different terms (control cuts, relief lines) describing the.same principle:
Smoothing out layer time effects by spreading large internal surfaces across multiple layers. Chamfer, Fillets or angling internal surfaces is more effective, but starting a surface a little lower does help as well.
Disrupting the shrinkage effect from large internal surfaces can be supported by introducing a geometric feature (trench, cut, line) which breaks up the straight loads of a large surface shrinking. It also effective in warping reduction. This thread here has a really good description and pic’s: Large Prints: Say Goodbye to Warping!
TL:DR - Add a Divot/Trench between the walls and the solid infil. Might also add a chamfer of the solid infill as well to make sure.
Alright, wanted to get testing in before I replied here.
I tried to modify settings in the bambu slicer and I bet I could have by slowing everything to a crawl or using the outer-inner slicer but I dont want to wait that many hours for a small defect and the model has an overhang. I will say having the chamber heat on did reduce the shrinkage of the bottom of the box but there was still a line, and I wanted to get rid of it fully.
So I was able to reduce the bench hull line or end of removing it by messing with the model (shocker I know). The two ways people usually edit the models to reduce the line is like recommended a Chamfer or to add a divot.
So the model on the inside is a thick square that then gets walls and is hollow. The line would come from the thick layer transitioning from infil to solid lines to finish the top layers. I first started by adding a chamfer until it didn’t hit the magnet holes (the 4 circular holes). This reduced it but didnt get rid of it fully.
So I added a trench between the walls and the solid infill portion. 1 mm wide. This actually got rid of the line in the bottom box, but for the top portion which is the same just with 1 wall removed the hull line was still there. So I depened the trench. The trench went 3 mm below where it would transition to 3 walls. Then I did a chamfer just in case (and to make it look pretty). This fixed the lines completely.
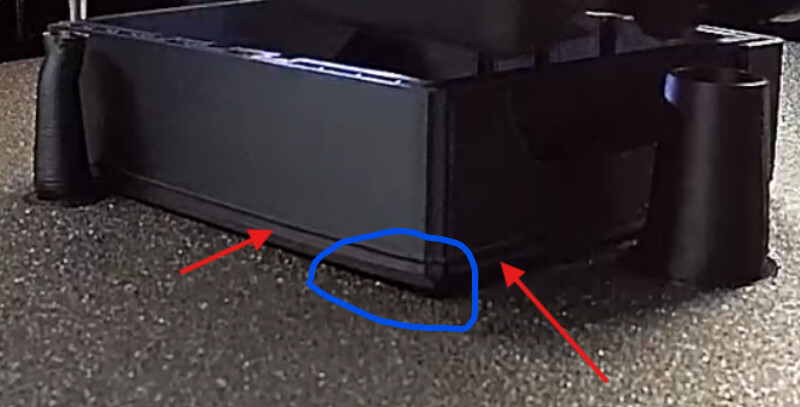
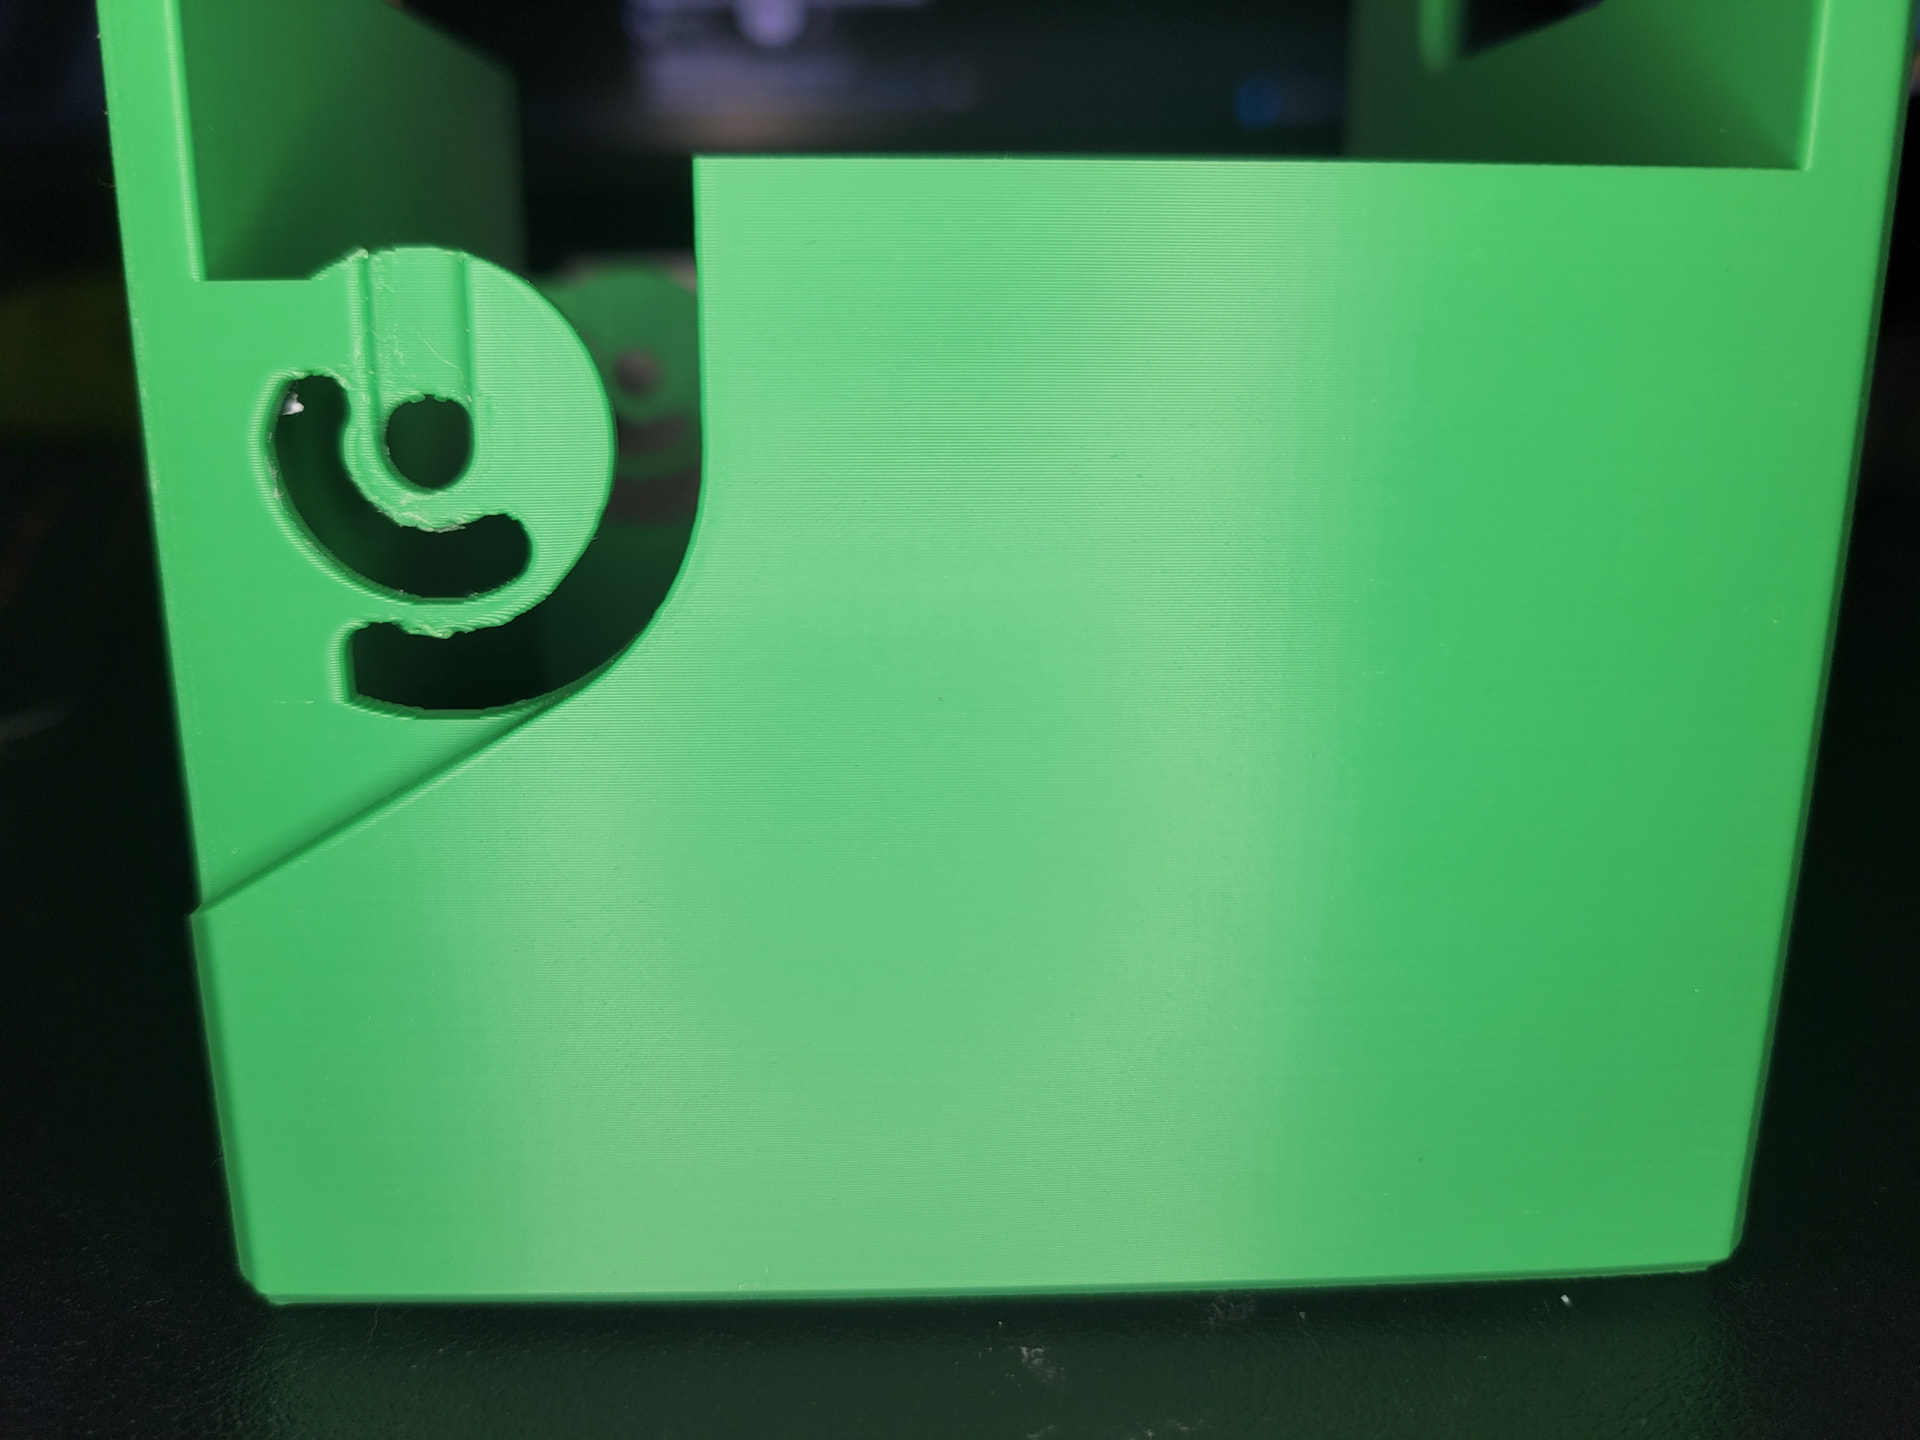
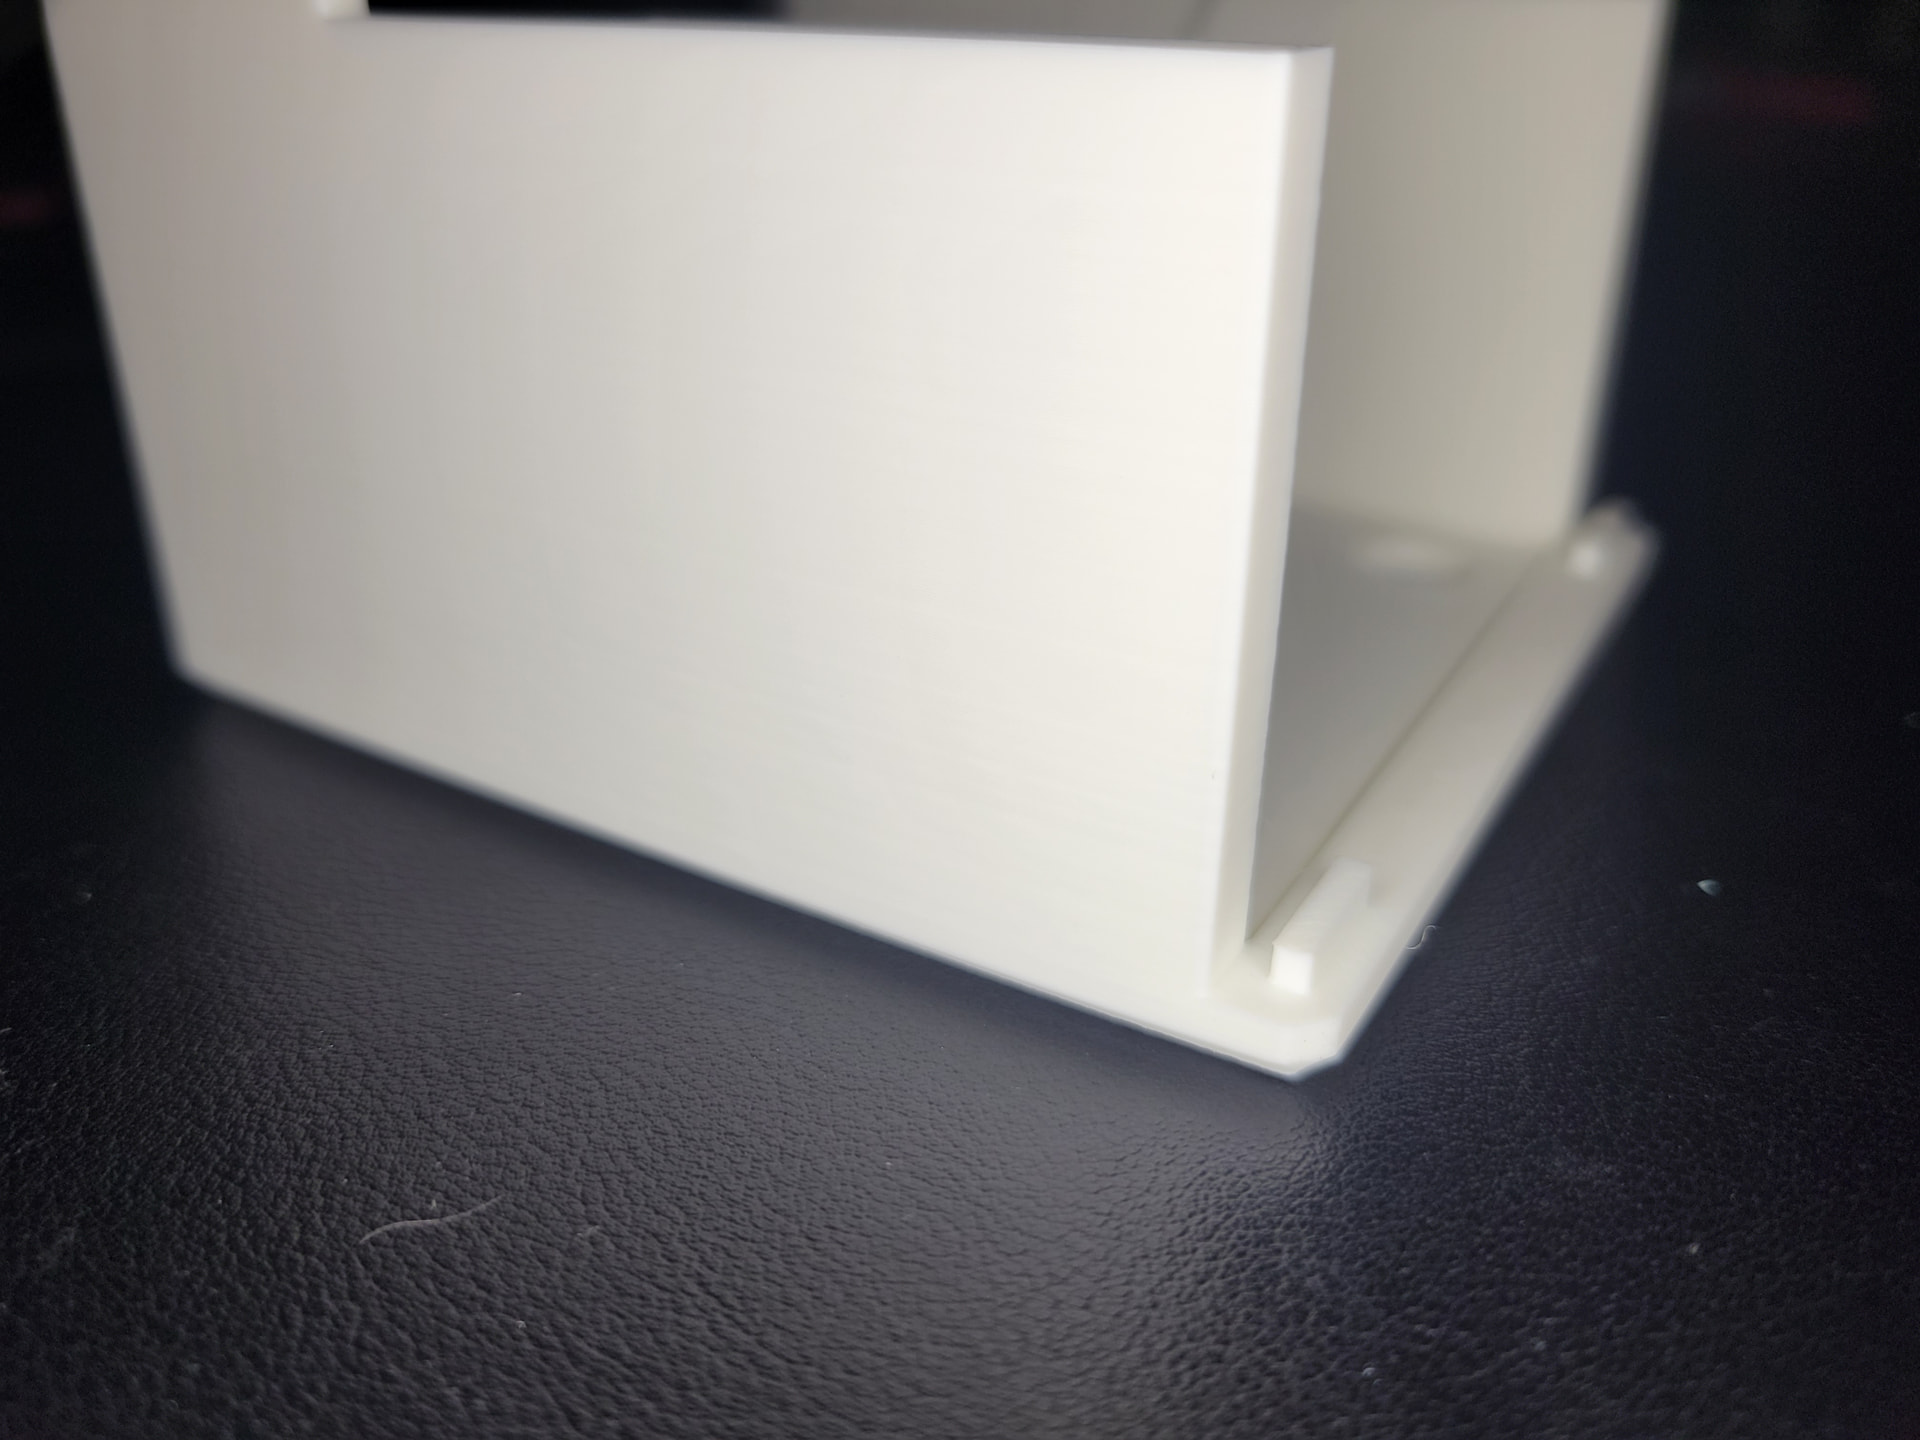
Here is the photos showing the lines gone and the inside where you see the trench. Thanks for all the help.
 &